...

Contact Skychem Group for more chemical solutions, If you have questions or need more information, please contact us.
Respond within 24 hours

Reactive Garment Dyeing: Process, Dyes, and Defect Control

A cotton T-shirt can match the approved body shade and still fail inspection because the collar is darker, the seams remain pale, or crease marks appear after drying. Garment dyeing brings together fabrics, threads, trims, and multilayer areas that may respond differently to the same bath.

Reactive garment dyeing colors assembled cellulosic garments through dye exhaustion and covalent fixation. Hydrolysis competes with fixation, leaving unfixed color that must be washed off. This guide covers dye selection, auxiliaries, process control, and defect prevention in industrial exhaust dyeing of cotton and other suitable cellulosic garments, including considerations for blends.

1. Selecting Reactive Dyes

Fiber and Component Compatibility

Check the complete garment specification before developing the recipe. Include body fabric, ribbing, pocketing, sewing thread, interlinings, labels, and trims.

Two cotton components can develop different shade depths because of differences in yarn, construction, mercerization, or preparation. Polyester sewing thread will not develop the same shade as cotton under a conventional cotton reactive dyeing process. Cotton-covered corespun thread may provide a closer match, but its appearance still requires a sewn-garment trial.

For blends, establish which components the process will color:

  • Cotton–polyester: Reactive dyes color the cellulosic portion. Matching the polyester requires a suitable additional dye system and compatible processing conditions.
  • Cotton–elastane: Check temperature, alkalinity, exposure time, and mechanical action against the material supplier’s recommendations. Assess stretch recovery and dimensional stability after processing.

Dye Compatibility and Process Suitability

Select reactive dyes for cellulosic fibers according to the target shade, machine capability, and application conditions. Compare solubility, recommended temperature, reactivity, exhaustion behavior, and wash-off performance.

Combination shades require compatible exhaustion and fixation behavior. When one dye reacts much faster than the others, dosing or temperature variation can shift the shade balance.

For sensitive combination shades, Skyzol RGB uses selected M-series dyes with similar substantivity and reactivity. Match the combination to the intended process and verify its response to changes in pH, electrolyte, temperature, and liquor ratio. Similar application behavior supports recipe compatibility but does not guarantee bulk shade reproducibility.
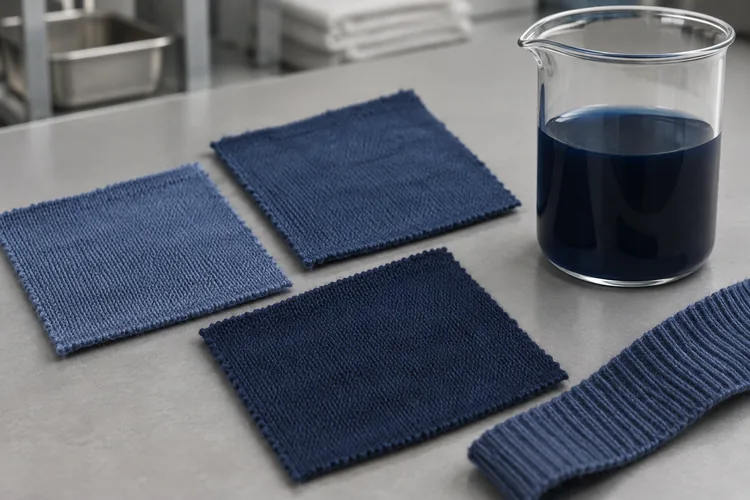
Cotton lab dips compared during reactive dye selection.

Fastness and Processing Cost

Define the required wash, rubbing, perspiration, and light fastness according to the garment’s end use. Strong wash fastness does not automatically establish suitability for every other exposure.

For deep shades, pay particular attention to wash-off demand and wet rubbing performance. Test after the intended finishing treatment because softening and drying can influence the final result.

Compare cost per kilogram of acceptable garments. Include dye consumption, auxiliaries, water, energy, processing time, and rework rather than judging a recipe by dye price alone.

2. Selecting Dyeing Auxiliaries

Select auxiliaries for a defined function and check compatibility across the complete bath.

Pretreatment Auxiliaries

Select textile pretreatment auxiliaries according to the impurities present and the garment’s preparation history. Wetting and scouring agents support uniform absorbency; sequestering agents help manage interfering metal ions.

Prepared-for-dyeing fabric can acquire sewing oils or handling contamination during garment assembly. Check the assembled garment, not just the original fabric specification.

Dyeing Auxiliaries and Process Chemicals

Choose dyeing auxiliaries for the machine, garment construction, and dye system. Check leveling agents for their effect on exhaustion and color yield. Address overloading or restricted movement directly; an anti-crease agent cannot correct those conditions.

Electrolyte and alkali have distinct roles in conventional reactive exhaust dyeing. Electrolyte promotes exhaustion; alkali creates conditions for dye–fiber fixation. Their quantities and addition sequence must match the selected application procedure.

Product category Main function Selection checks
Wetting and scouring agents Improve wetting and remove impurities Absorbency, foam, rinsability, and substrate suitability
Sequestering agents Manage interfering metal ions Water quality, working pH, and dye compatibility
Peroxide removal agents Eliminate residual peroxide after bleaching Working conditions and measured residual peroxide
Lubricants and anti-crease agents Reduce friction and crease formation Garment movement, machine conditions, and deposit risk
Leveling agents and defoamers Control uneven uptake or excessive foam where needed Bath stability, dye yield, and compatibility
Soaping agents Help remove unfixed dye and limit redeposition Shade depth, water quality, residual electrolyte, and fastness
Softeners Develop the required hand Shade change, spotting, absorbency, and compatibility
Fixing agents, where justified Improve specific fastness properties Measured benefit and effects on shade, hand, and other requirements

Wash-Off and Finishing Auxiliaries

Wash-off performance depends on dye substantivity, water quality, residual chemicals, temperature, and liquor exchange.

Sylic D2705 soaping agent is an anionic/nonionic surfactant–polymer powder for wash-off and anti-staining treatment of reactive-dyed cotton and rayon. Its pH of 6.0–8.0 refers to a 1% aqueous product solution, not the operating bath. Check compatibility with the other auxiliaries at the intended working conditions.

Set dosage, temperature, and sequence through garment trials. For a lower-temperature route, compare fastness, staining, and final shade with the established process before reducing heat input or cycle time. The required wash-off performance takes priority over potential energy savings.

Check softeners for effects on shade, absorbency, and hand. Use fixing agents only for a demonstrated fastness benefit; they do not replace fixation or effective washing-off.

Cotton garment partially immersed in a wash-off trial bath.

3. The Reactive Garment Dyeing Process

Step 1: Inspect and Prepare the Garments

Confirm garment weight, component lots, preparation history, and machine loading. Keep incompatible materials or preparation histories separate.

A practical readiness check includes:

  • Uniform absorbency across body fabric and components.
  • Removal of oils, sizing where present, and other relevant impurities.
  • Residual pH suitable for the next stage.
  • Acceptable process-water quality.
  • Verified peroxide removal when bleaching has been used.

Consistent cotton dyeing preparation provides the basis for uniform coloration. Include seams, waistbands, and pocket areas in the assessment; rapid wetting on the body alone does not establish readiness throughout an assembled garment.

Step 2: Prepare and Add the Dyes

Follow the dye-specific dissolution instructions for water quality, temperature, and concentration. Filter where required and inspect preparation tanks and transfer lines for contamination.

Establish uniform wetting and adequate garment movement before dosing. Introduce solutions through the intended addition system with sufficient mixing. Concentrated dye or alkali contacting garments directly can create local shade differences.

Prepare dye solutions within the recommended storage window. Avoid premature contact with alkali unless the application method specifically requires it.

Step 3: Control Exhaustion and Fixation

Use the application curve validated for the selected dye combination. Relevant reactive cotton dyeing parameters include temperature, pH, electrolyte, liquor ratio, and fixation time. Garment loading and movement must be controlled alongside them.

Follow the specified addition sequence, dosing rates, mixing intervals, and holding times. Staged addition is common, but alternative methods require their own validated procedure.

Monitor actual bath conditions using calibrated instruments. Record the measurement method because pH readings can differ with sample temperature and handling.

Keep dosage calculations consistent:

  • Grams per liter (g/L) depend on the actual bath volume.
  • Percent on weight of fiber (% owf) depends on the defined dry substrate weight.
  • Liquor ratio relates dry substrate mass to bath liquor mass. For an aqueous bath, a 100 kg load at 1:8 corresponds approximately to 800 liters of total liquor.

For blends, specify whether percentage additions are based on total dry garment weight or the cellulosic fraction. Include retained water and dosing water when determining the effective bath volume.

If color yield is weak, investigate preparation, weighing, dye strength, bath conditions, and process deviations before increasing chemical quantities.

Step 4: Rinse, Wash Off, and Finish

After fixation, remove residual chemicals and unfixed dye using the validated afterwashing sequence. Neutralization timing, rinse conditions, and soaping temperature depend on the dye and auxiliary system.

Provide enough garment movement and liquor exchange to clean multilayer areas as well as the body. Residual electrolyte can hinder removal of some unfixed dyes, so evaluate rinse efficiency when wash-off performance changes.

Apply finishing products under controlled conditions, then dry and condition consistently. Final approval should cover shade, component matching, fastness, hand, appearance, and dimensional stability.

4. Improving Shade Reproducibility

Standardize Materials and Chemical Inputs

A repeatable recipe requires consistent materials. Control fabric and component lots, preparation quality, dye strength, and auxiliary concentration.

Check incoming dye strength against an approved reference using a consistent procedure. Record any strength adjustment against the specific delivery so it does not become an unexplained change to the master recipe.

Validate Lab-to-Bulk Transfer

Use a defined lab-dip and scale-up workflow to compare laboratory and production conditions. Focus on liquor ratio, dosing, heating, mechanical action, washing-off, and finishing.

A fabric lab dip establishes a color target but cannot reproduce garment construction. Use representative sewn samples to check component matching, penetration, and appearance before bulk production.

Assess Color Under Agreed Conditions

Agree on the finished reference, conditioning procedure, illuminants, measurement locations, and acceptance tolerances before production.

For instrumental assessment, keep sample folding, orientation, backing, and measurement geometry consistent. Combine readings with visual inspection of the complete garment.

Check metamerism, where samples match under one light source but differ under another, using the buyer’s required lighting conditions. Assess shade after the specified finishing or wash treatment rather than comparing samples at different processing stages.

Use Batch Records to Investigate Variation

Record actual production conditions, including load, bath volume, material lots, chemical weights, additions, temperature, pH, interruptions, and corrections.

Compare a failed batch with an approved run before changing the formula. A different rib lot, unrecorded water addition, or dosing delay may explain the variation more directly than dye selection.

Cotton garments compared under controlled shade-assessment lighting.

5. Controlling Common Dyeing Defects

Map the defect before choosing a treatment. A problem affecting an entire batch suggests different causes from one limited to seams, folds, or individual garments.

Defect Causes to investigate Priority checks
Uneven or patchy shade Uneven preparation, restricted movement, residues, or irregular dosing Compare absorbency; review loading, circulation, and additions
Component mismatch Differences in fiber, construction, mercerization, or preparation Test actual sewn components and verify material specifications
Crease marks Persistent folds, friction, excessive loading, or unsuitable cooling Check garment movement, loading, lubrication, and cooling
Dye spots Undissolved dye, contamination, deposits, or concentrated additions Inspect dissolution, filters, tanks, dosing lines, and machine cleanliness
Batch shade variation Changed materials, dye strength, bath volume, or process execution Compare input lots and records with an approved batch
Poor wash or rubbing fastness Dye selection, incomplete fixation, ineffective wash-off, or finishing effects Test each property separately and review the relevant process stage
Backstaining Unfixed dye redepositing on receptive areas Review liquor exchange, rinse efficiency, water quality, and soaping
Shade change after finishing Softener effects, residues, pH, or drying variation Compare samples before and after finishing under consistent conditions

Evaluate corrective treatments for more than shade recovery. Additional washing, redyeing, or stripping can affect strength, stretch, hand, and dimensions. Confirm that the corrected garment meets the full specification before treating the batch.

For dye and auxiliary selection, specify the garment composition, component details, machine type, load, liquor ratio, target shade, fastness requirements, and current process. Use these details to define the trial recipe and acceptance criteria.

Paler crease-related shade mark on a cotton T-shirt.

FAQ

Is a fixing agent necessary after reactive garment dyeing?

No. First establish suitable dye selection, fixation, and washing-off. Consider a fixing agent when testing demonstrates a benefit against a defined requirement, and check its effects on shade, hand, and other performance criteria.

How can backstaining be reduced during washing-off?

Improve unfixed dye removal through suitable rinsing, liquor exchange, garment movement, and soaping conditions. Check water quality and residual electrolyte if performance changes. Confirm the improvement through staining and fastness tests rather than rinse-water appearance alone.

Sandy

With years of experience in chemical dyes and textile auxiliaries, I’m dedicated to sharing insights into the latest technologies, sustainable innovations, and market trends.

Recent Articles

Azo Dyes in Textiles: Restrictions, Testing, and Compliance

Table of Contents 1. Azo Dye Chemistry and Textile Uses What Is an Azo Dye? Where Are Azo Dyes Used? 2. Restricted Aromatic Amines How Azo Dyes Release Amines Which Amines Are Restricted? What Does “Azo-Free” Mean? 3. Compliance Requirements EU REACH Restrictions Destination-Market Rules Buyer RSLs and Chemical Standards 4. Azo Dye Testing Textile Test Methods Reading Test Reports 5. Buyer and Supplier Requirements Documents Buyers Should Request Selecting Suitable Dyes Managing Noncompliance FAQ Are All Azo Dyes Banned in Textiles? Does “Azo-Free” Mean REACH Compliant? Does ZDHC MRSL Conformance Replace Finished-Textile Testing? A dye that meets shade and fastness targets can still fail a customer’s chemical specification. For textile manufacturers and buyers, selecting azo dyes therefore requires both technical evaluation and reliable compliance evidence. Azo dyes are not universally banned. Restrictions target certain colorants and the aromatic amines they can release. Sound purchasing decisions depend on distinguishing dye chemistry, chemical-input controls, and finished-textile compliance. 1. Azo Dye Chemistry and Textile Uses What Is an Azo Dye? An azo dye contains one or more azo linkages, written as –N=N–, within its molecular structure. These linkages form part of a conjugated system that absorbs visible light. The surrounding molecular structure influences the resulting color and other properties. “Azo” describes chemical structure. “Reactive,” “direct,” “acid,” and “disperse” describe application classes, so a dye can belong to both categories. For example, azo direct dyes combine azo chemistry with the application characteristics of direct dyes. Reactive, acid, and disperse dye ranges can also include azo structures. Application class alone does not establish which restricted amines an individual product could release. Where Are Azo Dyes Used? For cotton and viscose, select reactive dyes according to the fixation process. The Skyzol KE/TE series uses monochlorotriazine reactive groups and is suited to dyeing at 80°C, including applications on viscose, towels, and mercerized cotton. It is not suitable for cold pad-batch processing. This process fit does not establish the azo structure or restricted-amine status of an individual shade; confirm those separately through product-specific information and test evidence. Disperse dyes are widely used on polyester, while acid dyes are commonly used on wool and nylon. 2. Restricted Aromatic Amines How Azo Dyes Release Amines Under reducing conditions, azo linkages can split through reductive cleavage. The resulting compounds depend on the colorant’s molecular structure. Certain azo dyes can release restricted aromatic amines. Laboratory tests use controlled conditions to assess this behavior. They do not simply measure dye washing off fabric, and their results are not direct predictions of exposure during ordinary wear. Two potential sources of amines should be distinguished: Amines released by cleavage: Compounds formed when the colorant breaks down under the specified test conditions. Free amine impurities: Residual compounds already present in a formulation or material. An unsuitable molecular structure and an impurity may require different corrective actions. Neither can be identified from shade alone. Which Amines Are Restricted? The REACH Appendix 8 list of aromatic amines contains 22 entries. Examples include benzidine, CAS 92-87-5; o-toluidine, CAS 95-53-4; and 4-aminoazobenzene, CAS 60-09-3. Compare CAS numbers as well as names when reviewing specifications. Different chemical names may refer to the same substance. Buyer lists may cover additional amines and related salts. A test panel covering the EU list may therefore be insufficient for a particular customer. What Does “Azo-Free” Mean? “Azo-free” is often used loosely in purchasing specifications. It may mean that no azo-structured colorants are permitted, or it may mean that a material must pass a restricted aromatic amine test. Define the term in writing before approval, specifying substances, test methods, acceptance limits, reporting limits, and components covered. 3. Compliance Requirements EU REACH Restrictions REACH Annex XVII Entry 43 prohibits the use of azo dyes that can release the listed aromatic amines above 30 mg/kg under specified testing conditions in textile and leather articles within scope, or their dyed parts. Nonconforming articles must not be placed on the market. The relevant articles are those that may come into direct and prolonged contact with skin or the oral cavity, including clothing, bedding, towels, and certain footwear and accessories. The threshold concerns individual listed amines released during testing. It is not a maximum concentration for all azo dyes in fabric or dye powder. Entry 43 also contains a separate restriction on colorants identified in Appendix 9. Passing an aromatic amine test alone should therefore not be presented as proof that every provision has been met. Destination-Market Rules Identify where the finished goods will be sold before finalizing the chemical specification. The manufacturing country does not determine all requirements for an export order. Confirm: Destination markets and product category. Intended use and relevant contact with skin or the mouth. Applicable legal requirements. The customer’s current restricted substances list. Testing and documentation requirements for individual components. A report prepared for a previous order may be useful, but its substance coverage, methods, and limits must match the new requirements. Buyer RSLs and Chemical Standards Legal restrictions, buyer specifications, and voluntary certification programs assess different aspects of the supply chain. Requirement or program What it addresses Key purchasing check REACH Entry 43 Restricted azo colorants and released amines in articles within scope Confirm product scope and applicable restrictions AFIRM RSL Restricted substances in finished-product component materials The 2026 list specifies 20 ppm each for listed azo-amines and arylamine salts, with a separate 5 ppm reporting limit ZDHC MRSL Restricted substances in manufacturing chemical formulations Verify conformance evidence for the exact chemical product OEKO-TEX STANDARD 100 Harmful-substance testing and certification of textiles Check certificate validity, article scope, and product class OEKO-TEX ECO PASSPORT Assessment and certification of chemicals, colorants, and auxiliaries Confirm that the supplied chemical product is covered A buyer may adopt an industry RSL or issue a separate specification. Confirm the version governing the order. An RSL addresses substances in finished materials or products. An MRSL addresses manufacturing chemical inputs. Conformant inputs help control risk, but they do not automatically establish finished-fabric compliance. When selecting ZDHC-conformant textile chemicals, match the product

Explore More »
Cotton yarn passing through metal guides during processing.

Textile Lubricants for Yarn and Fabric Processing: Selection, Dosage, and Compatibility

Table of Contents What Do Textile Lubricants Do? Choosing the Right Textile Lubricant Match the Fiber and Construction Match the Process and Equipment Compare Formulations Dosage and Application Understand the Dosage Basis Calculate Product Requirements Establish the Working Dosage Friction Control in Production Compatibility With Dyes and Auxiliaries Check Bath Stability Check Downstream Performance Validate Before Scale-Up Common Problems and Solutions FAQ How is textile lubricant dosage calculated? Can yarn lubricants be used in a dye bath? What is the difference between a textile lubricant and a softener? How can lubricant residues be removed before dyeing? Textile lubricants help control friction as fibers, yarns, and fabrics move through production. The right formulation and application can improve running stability, reduce abrasion, and support consistent processing. Selection depends on the substrate, equipment, and processing route. A lubricant must perform at the required application level without creating deposits or interfering with subsequent dyeing, printing, or finishing. This guide explains how to select textile lubricants, calculate application quantities, evaluate friction control, and check compatibility. What Do Textile Lubricants Do? Textile lubricants modify contact between textile materials and processing surfaces. Their functions differ across production stages. Processing stage Main lubrication objective Key evaluation points Fiber preparation and spinning Support controlled fiber movement while maintaining suitable cohesion Processing stability, distribution, static control where required Winding and knitting Maintain consistent yarn running behavior Yarn-to-metal friction, tension variation, breaks, deposits Warping and weaving Manage abrasion and yarn contact Size compatibility, yarn breaks, desizing requirements Sewing thread finishing Support thread passage through guides, tension devices, and needles Friction consistency, sewing performance, heat-related damage Wet fabric processing Reduce rubbing and associated abrasion or crease-mark risks Fabric movement, bath stability, foam, dye compatibility Fabric finishing Improve surface smoothness and sewability Handle, absorbency, shade, subsequent treatments These auxiliaries differ from machinery oils, which primarily lubricate components such as needles, bearings, and gears. Machinery oils should not replace substrate-applied lubricants unless specifically designed and approved for that use. Wet-processing anti-crease lubricants also differ from durable wrinkle-resistant finishes. They help reduce damaging friction during processing rather than impart lasting wrinkle resistance to the finished fabric. Choosing the Right Textile Lubricant Match the Fiber and Construction For yarn, record fiber composition, yarn count, spun or filament construction, twist, hairiness, and existing finish. Fine filament yarn and coarse spun yarn can require different lubrication and application conditions. For fabric, consider construction, weight, stretch content, and sensitivity to surface damage. Confirm suitability for elastane-containing materials under the intended treatment conditions. Test the substrate in its actual incoming condition. Existing spin finishes, sizing agents, surfactants, and softeners can affect wetting, lubricant pickup, and compatibility. Match the Process and Equipment Select spinning and yarn-processing auxiliaries according to the contact points that need lubrication and the requirements of the next production stage. For winding and knitting, prioritize uniform application and stable yarn tension. For weaving, evaluate abrasion and running behavior alongside sizing and desizing. Test sewing thread under representative speeds, tension settings, needles, and fabrics. Wet-processing lubricants must suit the intended temperature, pH, electrolyte concentration, and mechanical conditions. A yarn wax is not automatically suitable for a dye bath. The formulation must also work with the application equipment. Viscosity, dilution behavior, and feed consistency can influence distribution through metered applicators, kiss rolls, spray systems, exhaust baths, and padding equipment. Compare Formulations Wax emulsions, oil-based lubricants, and silicone-containing formulations offer different combinations of lubrication, application behavior, and removability. Performance depends on the complete formulation, including emulsifiers and functional additives. Sylic F3740 polyethylene wax emulsion is a nonionic formulation with 28–30% solids for textile lubrication and surface smoothness. It suits screening for processes requiring wax-based surface lubrication. Its concentration is relevant when calculating product consumption, while trials must establish friction control, deposit formation, and cleaning effectiveness. Solids content should not be treated as confirmed active content. Sylic F3741 silicone wax combines macromolecular polysiloxane and wax in a nonionic formulation. Evaluate it where a silicone-and-wax treatment is needed for lubrication and smoothness. Selection must account for application uniformity and removal before subsequent wet processing. Neither nonionic character nor silicone content alone establishes bath compatibility or antistatic performance. For either formulation, obtain the current technical data sheet to confirm the application method, dosage basis, and operating conditions. Dosage and Application Understand the Dosage Basis Dosage, bath concentration, and textile add-on describe different quantities. Term Meaning What to confirm % owf Product mass as a percentage of the specified textile weight Supplied product or diluted preparation g/L Product concentration in the treatment bath Bath volume and concentration basis Wet pickup Retained liquor mass as a percentage of dry textile mass Actual pickup during production Product add-on Applied or retained commercial product relative to textile weight Nominal or measured value, and measurement stage Active add-on Applied or retained active ingredient relative to textile weight Confirmed active content Yarn-processing instructions may use oiling rate or oil-on-yarn. Check the definition and measurement method before converting either value into equipment settings. Calculate Product Requirements For an exhaust recipe expressed as a percentage of textile weight: Product mass = textile mass × dosage percentage ÷ 100 Treating 500 kg of yarn at a hypothetical dosage of 1% owf requires 5 kg of commercial product. This is the amount introduced, not necessarily the amount deposited. For bath preparation: Product mass in grams = concentration in g/L × bath volume in liters An 800 L bath at a hypothetical concentration of 10 g/L requires 8,000 g, or 8 kg, of product. For padding with an aqueous bath having a density close to 1 kg/L: Nominal product add-on (%) = concentration (g/L) × wet pickup (%) ÷ 1,000 At 10 g/L and 70% wet pickup, nominal product add-on is 0.7% of dry textile weight. This assumes the retained liquor has the stated bath concentration. Incoming moisture, bath depletion, and replenishment can affect the estimate. These examples illustrate calculations, not recommended operating dosages. Understanding dosage and add-on in textile finishing helps prevent errors when comparing recipes or scaling up treatments. Establish the Working

Explore More »
Cotton twill samples beside dye samples and a scale.

Reactive Dye Pricing: Quotes, MOQ, and Total Dyeing Cost

Table of Contents What Drives Reactive Dye Prices? Dye Identity and Performance Strength and Product Form Supply and Order Conditions How to Compare Reactive Dye Quotes Match Product Specifications Check Commercial Terms Compare Landed Costs How MOQ Affects Purchasing Cost Confirm MOQ per Color and Order Balance Discounts and Inventory How to Calculate Total Dyeing Cost Dye Cost per Kilogram of Fabric Chemicals and Processing Costs Reprocessing and Quality Losses Worked Cost Comparison What to Include in a Quote Request FAQ How much do reactive dyes cost per kilogram? Why do quotes for the same dye differ? Are higher-strength reactive dyes more economical? What is the MOQ for reactive dyes? Can different colors be combined to meet the MOQ? How do I calculate dyeing cost per kilogram of fabric? The lowest reactive dye price per kilogram does not always produce the lowest dyeing cost. A less expensive product may require a higher dosage, a longer wash-off cycle, or more frequent shade corrections. A higher-priced alternative may be more economical if production trials confirm better color yield or lower processing costs. Compare reactive dye offers at three levels: quoted price, landed cost, and dyeing cost per kilogram of acceptable fabric. Product specifications, MOQ, and delivery terms determine whether those comparisons are meaningful. What Drives Reactive Dye Prices? Dye Identity and Performance Reactive dyes vary in chemical structure, color, formulation, and application requirements. These differences affect both manufacturing cost and performance in the dyehouse. Identify the exact product grade and Color Index identity, where applicable. A shared trade name does not establish equivalence, and products with the same Color Index identity can still differ in commercial strength, shade, and formulation. Select reactive dyes for the intended application before comparing prices. Assess solubility, compatibility in dye combinations, required fastness, and consistency between batches. The required shade depth matters as well. A product that performs well in pale shades may not deliver the most economical result at a deep shade. Compare candidates at the actual production shade and on representative fabric. Strength and Product Form Commercial strength designations such as 100%, 150%, and 200% describe color strength relative to a reference standard. They do not indicate chemical purity. For example, a 150% grade nominally has 1.5 times the color strength of its 100% reference under the specified test conditions. That relationship should not be assumed across suppliers using different standards or automatically converted into a production dosage. Powder and liquid products also need a common comparison basis. Price them against validated consumption, handling requirements, storage conditions, and transport costs. A lower price per kilogram of liquid does not necessarily mean a lower cost per kilogram of fabric. Supply and Order Conditions Raw material availability, energy costs, manufacturing requirements, currency movements, and logistics can affect a quotation. Order conditions add another layer: Quantity: Larger orders may qualify for volume discounts. Availability: Stocked grades and products requiring a production run may have different lead times. Packaging: Special pack sizes or labeling can add cost. Payment: Credit periods and other payment conditions may influence pricing. Delivery: Urgent transport can outweigh savings on the dye itself. When requesting a revised offer, specify the quantity, delivery schedule, or other condition that has changed. How to Compare Reactive Dye Quotes Match Product Specifications Give each supplier the same technical brief: fabric composition, target shade, application method, and acceptance requirements. Where available, provide an approved fabric sample or current dye reference. Use the following checklist to separate product differences from commercial differences. Comparison item What to confirm Why it matters Product identity Exact grade, Color Index identity where applicable, and intended process Similar names do not guarantee equivalent performance Commercial strength Reference standard, test conditions, and tolerance Strength percentages require a common basis Application results Validated dosage, shade, solubility, levelness, and fastness These determine suitability and consumption Quantity and packaging Net weight, pack size, MOQ, and price tier These affect purchase cost and inventory Commercial terms Currency, payment conditions, lead time, and quote validity Offers may reflect different commitments Delivery basis Trade term, named location, and excluded charges Unit prices may cover different delivery costs Approve the product through laboratory testing, followed by an appropriate production trial. Keep the substrate and process conditions consistent during initial comparisons, then document any adjustments needed. Check Commercial Terms For international orders, identify the selected Incoterms® 2020 rule and the named place or port. These rules allocate delivery responsibilities, costs, and risks between buyer and seller. Agree separately on payment timing, product specifications, acceptance procedures, and how quality claims will be handled. A trade term does not replace the purchase agreement. Compare Landed Costs Bring every offer to the same destination and cost basis before choosing a supplier. Landed dye cost/kg = Total acquisition cost ÷ Net kilograms received Include the product invoice plus applicable freight, insurance, import duties, clearance, and inland delivery that are not already covered. Avoid counting charges twice. Treat recoverable taxes separately from permanent costs, while accounting for their effect on cash flow. Use the landed dye price in subsequent recipe-cost calculations. How MOQ Affects Purchasing Cost Confirm MOQ per Color and Order Minimum order quantity can apply per product, per color, or per shipment. Confirm all applicable conditions. A supplier may accept a mixed-color shipment while retaining a minimum for each grade. Likewise, a standard 25 kg package, for example, does not prove that the MOQ is 25 kg. The minimum may involve several packages. Ask separately about laboratory samples and production-trial quantities. These may be available under different terms from routine bulk orders. Balance Discounts and Inventory Evaluate volume discounts against consumption, storage requirements, shelf life, and working capital. Slow-moving shades can tie up cash and leave stock unused, offsetting the lower purchase price. For recurring purchases, discuss scheduled releases or staged deliveries where available. Confirm whether the quoted price covers the full commitment, how long stock can be held, and whether additional delivery charges apply. How to Calculate Total Dyeing Cost Dye Cost per Kilogram of Fabric

Explore More »
Cotton twill swatches for vat dye shade evaluation.

How to Evaluate a Vat Dye Supplier?

Table of Contents 1. Shade Range Target-Shade Coverage Product Identity and Strength Recipe Compatibility 2. Batch Consistency Quality Control Evidence Multi-Lot Testing Acceptance Criteria 3. Reduction Behavior Process-Specific Conditions Reduction Completeness and Stability Auxiliary Compatibility 4. Fastness Performance End-Use Requirements Shade-Specific Results Finished-Fabric Verification 5. Supplier Comparison and Approval Evidence-Based Comparison Pilot Qualification 6. FAQ How can I verify a vat dye supplier’s shade range? How do I check vat dye batch consistency? Are vat dyes with the same Colour Index name interchangeable? How should I compare reduction behavior? Which fastness tests should I request? Can textile auxiliaries affect vat dye performance? A competitive price and a good-looking lab dip are useful starting points, but neither proves that a vat dye will perform reliably in production. Differences in commercial strength, formulation, reduction behavior, and lot quality can lead to shade corrections, longer processing, and rejected fabric. Evaluate suppliers on shade coverage, batch consistency, reduction behavior, and finished-fabric fastness. Give each supplier the same application brief before requesting samples. Include the substrate, pretreatment, dyeing method, target shades, shade depths, finishing route, and customer requirements. A clear brief makes recommendations more relevant and comparisons more reliable. 1. Shade Range Target-Shade Coverage Judge shade coverage against your production requirements. Start with repeat-order colors, high-volume dark shades, and combinations that are difficult to reproduce. For cotton dyeing, select Skythrene® vat dyes against the required shade and process, then verify the selected grades through lab dips on the intended fabric or yarn. Shade cards and screen images support initial selection, but they do not establish color accuracy or fastness on your substrate. Evaluate relevant depths, including pale shades where small hue differences are visible and deep shades where build-up and washing-off become more demanding. For blends, specify which fiber component the vat dye will color and assess the complete processing route. Product Identity and Strength Request the Colour Index name where applicable, commercial grade, physical form, and declared strength. Clarify whether each product is a single colorant or a formulated blend. Products with the same Colour Index name can differ in strength, formulation, dispersion, and application behavior. A shared identity therefore does not establish that two commercial grades are interchangeable. Strength labels also need context. A designation such as 100% or 200% refers to a defined reference basis, which may differ between suppliers. Compare the dosage required to reach the same approved shade instead of assuming that matching labels indicate equal performance. Recipe Compatibility Dyes that perform well individually may behave differently in a combination. Check whether the proposed components have compatible reduction conditions and dyeing characteristics. Ask for trials of complete recipes, especially those used for repeat orders. Assess whether the combination holds its hue within normal production variations. 2. Batch Consistency Quality Control Evidence Request certificates of analysis from separate production lots, supported by an explanation of the release tests. Relevant results may include relative color strength, shade difference against an approved reference, and physical quality checks appropriate to the product form. Confirm the reference batch, measurement procedure, and acceptance limits behind the results. Also confirm lot traceability, retained-sample practices, and notification procedures for formulation or manufacturing changes. These records help resolve discrepancies between an approved sample and a later shipment. Multi-Lot Testing Where practical, evaluate three lots using the same substrate batch, water, auxiliaries, equipment, and processing sequence. This is a practical qualification approach, not a universal minimum. Use two comparisons when necessary: Equal-dosage trials: Apply the same product dosage to identify differences in supplied strength and hue. Matched-depth trials: Adjust dosage to the target depth to compare achievable shade, fastness, and treatment cost. Assess the final color after consistent oxidation, soaping, drying, and conditioning. Keep lot numbers, recipes, test records, and dyed swatches together as references for incoming deliveries. Acceptance Criteria Agree on instrumental and visual assessment conditions before placing a bulk order. Define the color-difference formula, illuminant, observer, measurement setup, and sample preparation. Avoid a universal color-difference limit. Acceptable variation depends on shade, fabric appearance, end use, and customer expectations. Visual checks under relevant lighting also help identify matches that change noticeably between light sources. Finally, confirm how the supplier investigates an out-of-specification lot, communicates findings, and provides corrective action. 3. Reduction Behavior Process-Specific Conditions Vat dyes must be reduced to a soluble leuco form so the colorant can enter the cellulosic fiber. Oxidation then restores the insoluble form. This mechanism makes control of reduction and oxidation central to application performance. Request grade-specific recommendations for reducing agent, alkali, temperature, time, and addition sequence. Confirm whether stock-vat preparation or another application procedure is recommended. Account for the differences between continuous and exhaust vat dyeing. The available reduction time, application sequence, and exposure to air vary by process. A grade approved for one route should still be verified before use in another. Reduction Completeness and Stability Evaluate whether the dye reaches an adequately reduced state within the available processing time. Record residual particles or deposits, penetration, levelness, and final shade. Then assess stability within your normal operating window. Small, controlled variations in temperature, time, or chemical addition can help reveal whether a recipe is robust enough for production. Follow product-specific guidance, since excessive reduction can damage some vat dyes and cause irreversible shade changes. If redox potential is monitored, define the electrode and reference system, temperature, calibration checks, and measurement procedure. A reading without this context is an unreliable basis for comparing suppliers. Record chemical consumption, cycle time, and correction frequency alongside reduction speed. Auxiliary Compatibility Test the selected dyes with the textile dyeing auxiliaries intended for production. Confirm compatibility with the required alkalinity, temperature, reducing conditions, and equipment. Wetting, dispersion, water hardness, and foam can all influence uniformity. For applications requiring rapid wetting and penetration, Sylic P1400 wetting agent has an anionic/nonionic character and is used in pretreatment, dyeing, and finishing. Reference dosages are 0.5–2 g/L for intermittent processing and 2–6 g/L for continuous processing. Use these ranges as trial starting points, then check penetration, foam, and compatibility at the

Explore More »

Contact Us for Textile Auxiliaries and Dyes

Contact Skychem Group for more chemical solutions, If you have questions or need more information, please contact us.
We will respond within 24 hours

Get a project quote

Tell us your project requirements, country, and intended application.

Sandy

With years of experience in chemical dyes and textile auxiliaries, I’m dedicated to sharing insights into the latest technologies, sustainable innovations, and market trends.

Recent Articles

Azo Dyes in Textiles: Restrictions, Testing, and Compliance

Table of Contents 1. Azo Dye Chemistry and Textile Uses What Is an Azo Dye? Where Are Azo Dyes Used? 2. Restricted Aromatic Amines How Azo Dyes Release Amines Which Amines Are Restricted? What Does “Azo-Free” Mean? 3. Compliance Requirements EU REACH Restrictions Destination-Market Rules Buyer RSLs and Chemical Standards 4. Azo Dye Testing Textile Test Methods Reading Test Reports 5. Buyer and Supplier Requirements Documents Buyers Should Request Selecting Suitable Dyes Managing Noncompliance FAQ Are All Azo Dyes Banned in Textiles? Does “Azo-Free” Mean REACH Compliant? Does ZDHC MRSL Conformance Replace Finished-Textile Testing? A dye that meets shade and fastness targets can still fail a customer’s chemical specification. For textile manufacturers and buyers, selecting azo dyes therefore requires both technical evaluation and reliable compliance evidence. Azo dyes are not universally banned. Restrictions target certain colorants and the aromatic amines they can release. Sound purchasing decisions depend on distinguishing dye chemistry, chemical-input controls, and finished-textile compliance. 1. Azo Dye Chemistry and Textile Uses What Is an Azo Dye? An azo dye contains one or more azo linkages, written as –N=N–, within its molecular structure. These linkages form part of a conjugated system that absorbs visible light. The surrounding molecular structure influences the resulting color and other properties. “Azo” describes chemical structure. “Reactive,” “direct,” “acid,” and “disperse” describe application classes, so a dye can belong to both categories. For example, azo direct dyes combine azo chemistry with the application characteristics of direct dyes. Reactive, acid, and disperse dye ranges can also include azo structures. Application class alone does not establish which restricted amines an individual product could release. Where Are Azo Dyes Used? For cotton and viscose, select reactive dyes according to the fixation process. The Skyzol KE/TE series uses monochlorotriazine reactive groups and is suited to dyeing at 80°C, including applications on viscose, towels, and mercerized cotton. It is not suitable for cold pad-batch processing. This process fit does not establish the azo structure or restricted-amine status of an individual shade; confirm those separately through product-specific information and test evidence. Disperse dyes are widely used on polyester, while acid dyes are commonly used on wool and nylon. 2. Restricted Aromatic Amines How Azo Dyes Release Amines Under reducing conditions, azo linkages can split through reductive cleavage. The resulting compounds depend on the colorant’s molecular structure. Certain azo dyes can release restricted aromatic amines. Laboratory tests use controlled conditions to assess this behavior. They do not simply measure dye washing off fabric, and their results are not direct predictions of exposure during ordinary wear. Two potential sources of amines should be distinguished: Amines released by cleavage: Compounds formed when the colorant breaks down under the specified test conditions. Free amine impurities: Residual compounds already present in a formulation or material. An unsuitable molecular structure and an impurity may require different corrective actions. Neither can be identified from shade alone. Which Amines Are Restricted? The REACH Appendix 8 list of aromatic amines contains 22 entries. Examples include benzidine, CAS 92-87-5; o-toluidine, CAS 95-53-4; and 4-aminoazobenzene, CAS 60-09-3. Compare CAS numbers as well as names when reviewing specifications. Different chemical names may refer to the same substance. Buyer lists may cover additional amines and related salts. A test panel covering the EU list may therefore be insufficient for a particular customer. What Does “Azo-Free” Mean? “Azo-free” is often used loosely in purchasing specifications. It may mean that no azo-structured colorants are permitted, or it may mean that a material must pass a restricted aromatic amine test. Define the term in writing before approval, specifying substances, test methods, acceptance limits, reporting limits, and components covered. 3. Compliance Requirements EU REACH Restrictions REACH Annex XVII Entry 43 prohibits the use of azo dyes that can release the listed aromatic amines above 30 mg/kg under specified testing conditions in textile and leather articles within scope, or their dyed parts. Nonconforming articles must not be placed on the market. The relevant articles are those that may come into direct and prolonged contact with skin or the oral cavity, including clothing, bedding, towels, and certain footwear and accessories. The threshold concerns individual listed amines released during testing. It is not a maximum concentration for all azo dyes in fabric or dye powder. Entry 43 also contains a separate restriction on colorants identified in Appendix 9. Passing an aromatic amine test alone should therefore not be presented as proof that every provision has been met. Destination-Market Rules Identify where the finished goods will be sold before finalizing the chemical specification. The manufacturing country does not determine all requirements for an export order. Confirm: Destination markets and product category. Intended use and relevant contact with skin or the mouth. Applicable legal requirements. The customer’s current restricted substances list. Testing and documentation requirements for individual components. A report prepared for a previous order may be useful, but its substance coverage, methods, and limits must match the new requirements. Buyer RSLs and Chemical Standards Legal restrictions, buyer specifications, and voluntary certification programs assess different aspects of the supply chain. Requirement or program What it addresses Key purchasing check REACH Entry 43 Restricted azo colorants and released amines in articles within scope Confirm product scope and applicable restrictions AFIRM RSL Restricted substances in finished-product component materials The 2026 list specifies 20 ppm each for listed azo-amines and arylamine salts, with a separate 5 ppm reporting limit ZDHC MRSL Restricted substances in manufacturing chemical formulations Verify conformance evidence for the exact chemical product OEKO-TEX STANDARD 100 Harmful-substance testing and certification of textiles Check certificate validity, article scope, and product class OEKO-TEX ECO PASSPORT Assessment and certification of chemicals, colorants, and auxiliaries Confirm that the supplied chemical product is covered A buyer may adopt an industry RSL or issue a separate specification. Confirm the version governing the order. An RSL addresses substances in finished materials or products. An MRSL addresses manufacturing chemical inputs. Conformant inputs help control risk, but they do not automatically establish finished-fabric compliance. When selecting ZDHC-conformant textile chemicals, match the product

Explore More »
Cotton yarn passing through metal guides during processing.

Textile Lubricants for Yarn and Fabric Processing: Selection, Dosage, and Compatibility

Table of Contents What Do Textile Lubricants Do? Choosing the Right Textile Lubricant Match the Fiber and Construction Match the Process and Equipment Compare Formulations Dosage and Application Understand the Dosage Basis Calculate Product Requirements Establish the Working Dosage Friction Control in Production Compatibility With Dyes and Auxiliaries Check Bath Stability Check Downstream Performance Validate Before Scale-Up Common Problems and Solutions FAQ How is textile lubricant dosage calculated? Can yarn lubricants be used in a dye bath? What is the difference between a textile lubricant and a softener? How can lubricant residues be removed before dyeing? Textile lubricants help control friction as fibers, yarns, and fabrics move through production. The right formulation and application can improve running stability, reduce abrasion, and support consistent processing. Selection depends on the substrate, equipment, and processing route. A lubricant must perform at the required application level without creating deposits or interfering with subsequent dyeing, printing, or finishing. This guide explains how to select textile lubricants, calculate application quantities, evaluate friction control, and check compatibility. What Do Textile Lubricants Do? Textile lubricants modify contact between textile materials and processing surfaces. Their functions differ across production stages. Processing stage Main lubrication objective Key evaluation points Fiber preparation and spinning Support controlled fiber movement while maintaining suitable cohesion Processing stability, distribution, static control where required Winding and knitting Maintain consistent yarn running behavior Yarn-to-metal friction, tension variation, breaks, deposits Warping and weaving Manage abrasion and yarn contact Size compatibility, yarn breaks, desizing requirements Sewing thread finishing Support thread passage through guides, tension devices, and needles Friction consistency, sewing performance, heat-related damage Wet fabric processing Reduce rubbing and associated abrasion or crease-mark risks Fabric movement, bath stability, foam, dye compatibility Fabric finishing Improve surface smoothness and sewability Handle, absorbency, shade, subsequent treatments These auxiliaries differ from machinery oils, which primarily lubricate components such as needles, bearings, and gears. Machinery oils should not replace substrate-applied lubricants unless specifically designed and approved for that use. Wet-processing anti-crease lubricants also differ from durable wrinkle-resistant finishes. They help reduce damaging friction during processing rather than impart lasting wrinkle resistance to the finished fabric. Choosing the Right Textile Lubricant Match the Fiber and Construction For yarn, record fiber composition, yarn count, spun or filament construction, twist, hairiness, and existing finish. Fine filament yarn and coarse spun yarn can require different lubrication and application conditions. For fabric, consider construction, weight, stretch content, and sensitivity to surface damage. Confirm suitability for elastane-containing materials under the intended treatment conditions. Test the substrate in its actual incoming condition. Existing spin finishes, sizing agents, surfactants, and softeners can affect wetting, lubricant pickup, and compatibility. Match the Process and Equipment Select spinning and yarn-processing auxiliaries according to the contact points that need lubrication and the requirements of the next production stage. For winding and knitting, prioritize uniform application and stable yarn tension. For weaving, evaluate abrasion and running behavior alongside sizing and desizing. Test sewing thread under representative speeds, tension settings, needles, and fabrics. Wet-processing lubricants must suit the intended temperature, pH, electrolyte concentration, and mechanical conditions. A yarn wax is not automatically suitable for a dye bath. The formulation must also work with the application equipment. Viscosity, dilution behavior, and feed consistency can influence distribution through metered applicators, kiss rolls, spray systems, exhaust baths, and padding equipment. Compare Formulations Wax emulsions, oil-based lubricants, and silicone-containing formulations offer different combinations of lubrication, application behavior, and removability. Performance depends on the complete formulation, including emulsifiers and functional additives. Sylic F3740 polyethylene wax emulsion is a nonionic formulation with 28–30% solids for textile lubrication and surface smoothness. It suits screening for processes requiring wax-based surface lubrication. Its concentration is relevant when calculating product consumption, while trials must establish friction control, deposit formation, and cleaning effectiveness. Solids content should not be treated as confirmed active content. Sylic F3741 silicone wax combines macromolecular polysiloxane and wax in a nonionic formulation. Evaluate it where a silicone-and-wax treatment is needed for lubrication and smoothness. Selection must account for application uniformity and removal before subsequent wet processing. Neither nonionic character nor silicone content alone establishes bath compatibility or antistatic performance. For either formulation, obtain the current technical data sheet to confirm the application method, dosage basis, and operating conditions. Dosage and Application Understand the Dosage Basis Dosage, bath concentration, and textile add-on describe different quantities. Term Meaning What to confirm % owf Product mass as a percentage of the specified textile weight Supplied product or diluted preparation g/L Product concentration in the treatment bath Bath volume and concentration basis Wet pickup Retained liquor mass as a percentage of dry textile mass Actual pickup during production Product add-on Applied or retained commercial product relative to textile weight Nominal or measured value, and measurement stage Active add-on Applied or retained active ingredient relative to textile weight Confirmed active content Yarn-processing instructions may use oiling rate or oil-on-yarn. Check the definition and measurement method before converting either value into equipment settings. Calculate Product Requirements For an exhaust recipe expressed as a percentage of textile weight: Product mass = textile mass × dosage percentage ÷ 100 Treating 500 kg of yarn at a hypothetical dosage of 1% owf requires 5 kg of commercial product. This is the amount introduced, not necessarily the amount deposited. For bath preparation: Product mass in grams = concentration in g/L × bath volume in liters An 800 L bath at a hypothetical concentration of 10 g/L requires 8,000 g, or 8 kg, of product. For padding with an aqueous bath having a density close to 1 kg/L: Nominal product add-on (%) = concentration (g/L) × wet pickup (%) ÷ 1,000 At 10 g/L and 70% wet pickup, nominal product add-on is 0.7% of dry textile weight. This assumes the retained liquor has the stated bath concentration. Incoming moisture, bath depletion, and replenishment can affect the estimate. These examples illustrate calculations, not recommended operating dosages. Understanding dosage and add-on in textile finishing helps prevent errors when comparing recipes or scaling up treatments. Establish the Working

Explore More »
Cotton twill samples beside dye samples and a scale.

Reactive Dye Pricing: Quotes, MOQ, and Total Dyeing Cost

Table of Contents What Drives Reactive Dye Prices? Dye Identity and Performance Strength and Product Form Supply and Order Conditions How to Compare Reactive Dye Quotes Match Product Specifications Check Commercial Terms Compare Landed Costs How MOQ Affects Purchasing Cost Confirm MOQ per Color and Order Balance Discounts and Inventory How to Calculate Total Dyeing Cost Dye Cost per Kilogram of Fabric Chemicals and Processing Costs Reprocessing and Quality Losses Worked Cost Comparison What to Include in a Quote Request FAQ How much do reactive dyes cost per kilogram? Why do quotes for the same dye differ? Are higher-strength reactive dyes more economical? What is the MOQ for reactive dyes? Can different colors be combined to meet the MOQ? How do I calculate dyeing cost per kilogram of fabric? The lowest reactive dye price per kilogram does not always produce the lowest dyeing cost. A less expensive product may require a higher dosage, a longer wash-off cycle, or more frequent shade corrections. A higher-priced alternative may be more economical if production trials confirm better color yield or lower processing costs. Compare reactive dye offers at three levels: quoted price, landed cost, and dyeing cost per kilogram of acceptable fabric. Product specifications, MOQ, and delivery terms determine whether those comparisons are meaningful. What Drives Reactive Dye Prices? Dye Identity and Performance Reactive dyes vary in chemical structure, color, formulation, and application requirements. These differences affect both manufacturing cost and performance in the dyehouse. Identify the exact product grade and Color Index identity, where applicable. A shared trade name does not establish equivalence, and products with the same Color Index identity can still differ in commercial strength, shade, and formulation. Select reactive dyes for the intended application before comparing prices. Assess solubility, compatibility in dye combinations, required fastness, and consistency between batches. The required shade depth matters as well. A product that performs well in pale shades may not deliver the most economical result at a deep shade. Compare candidates at the actual production shade and on representative fabric. Strength and Product Form Commercial strength designations such as 100%, 150%, and 200% describe color strength relative to a reference standard. They do not indicate chemical purity. For example, a 150% grade nominally has 1.5 times the color strength of its 100% reference under the specified test conditions. That relationship should not be assumed across suppliers using different standards or automatically converted into a production dosage. Powder and liquid products also need a common comparison basis. Price them against validated consumption, handling requirements, storage conditions, and transport costs. A lower price per kilogram of liquid does not necessarily mean a lower cost per kilogram of fabric. Supply and Order Conditions Raw material availability, energy costs, manufacturing requirements, currency movements, and logistics can affect a quotation. Order conditions add another layer: Quantity: Larger orders may qualify for volume discounts. Availability: Stocked grades and products requiring a production run may have different lead times. Packaging: Special pack sizes or labeling can add cost. Payment: Credit periods and other payment conditions may influence pricing. Delivery: Urgent transport can outweigh savings on the dye itself. When requesting a revised offer, specify the quantity, delivery schedule, or other condition that has changed. How to Compare Reactive Dye Quotes Match Product Specifications Give each supplier the same technical brief: fabric composition, target shade, application method, and acceptance requirements. Where available, provide an approved fabric sample or current dye reference. Use the following checklist to separate product differences from commercial differences. Comparison item What to confirm Why it matters Product identity Exact grade, Color Index identity where applicable, and intended process Similar names do not guarantee equivalent performance Commercial strength Reference standard, test conditions, and tolerance Strength percentages require a common basis Application results Validated dosage, shade, solubility, levelness, and fastness These determine suitability and consumption Quantity and packaging Net weight, pack size, MOQ, and price tier These affect purchase cost and inventory Commercial terms Currency, payment conditions, lead time, and quote validity Offers may reflect different commitments Delivery basis Trade term, named location, and excluded charges Unit prices may cover different delivery costs Approve the product through laboratory testing, followed by an appropriate production trial. Keep the substrate and process conditions consistent during initial comparisons, then document any adjustments needed. Check Commercial Terms For international orders, identify the selected Incoterms® 2020 rule and the named place or port. These rules allocate delivery responsibilities, costs, and risks between buyer and seller. Agree separately on payment timing, product specifications, acceptance procedures, and how quality claims will be handled. A trade term does not replace the purchase agreement. Compare Landed Costs Bring every offer to the same destination and cost basis before choosing a supplier. Landed dye cost/kg = Total acquisition cost ÷ Net kilograms received Include the product invoice plus applicable freight, insurance, import duties, clearance, and inland delivery that are not already covered. Avoid counting charges twice. Treat recoverable taxes separately from permanent costs, while accounting for their effect on cash flow. Use the landed dye price in subsequent recipe-cost calculations. How MOQ Affects Purchasing Cost Confirm MOQ per Color and Order Minimum order quantity can apply per product, per color, or per shipment. Confirm all applicable conditions. A supplier may accept a mixed-color shipment while retaining a minimum for each grade. Likewise, a standard 25 kg package, for example, does not prove that the MOQ is 25 kg. The minimum may involve several packages. Ask separately about laboratory samples and production-trial quantities. These may be available under different terms from routine bulk orders. Balance Discounts and Inventory Evaluate volume discounts against consumption, storage requirements, shelf life, and working capital. Slow-moving shades can tie up cash and leave stock unused, offsetting the lower purchase price. For recurring purchases, discuss scheduled releases or staged deliveries where available. Confirm whether the quoted price covers the full commitment, how long stock can be held, and whether additional delivery charges apply. How to Calculate Total Dyeing Cost Dye Cost per Kilogram of Fabric

Explore More »
Cotton twill swatches for vat dye shade evaluation.

How to Evaluate a Vat Dye Supplier?

Table of Contents 1. Shade Range Target-Shade Coverage Product Identity and Strength Recipe Compatibility 2. Batch Consistency Quality Control Evidence Multi-Lot Testing Acceptance Criteria 3. Reduction Behavior Process-Specific Conditions Reduction Completeness and Stability Auxiliary Compatibility 4. Fastness Performance End-Use Requirements Shade-Specific Results Finished-Fabric Verification 5. Supplier Comparison and Approval Evidence-Based Comparison Pilot Qualification 6. FAQ How can I verify a vat dye supplier’s shade range? How do I check vat dye batch consistency? Are vat dyes with the same Colour Index name interchangeable? How should I compare reduction behavior? Which fastness tests should I request? Can textile auxiliaries affect vat dye performance? A competitive price and a good-looking lab dip are useful starting points, but neither proves that a vat dye will perform reliably in production. Differences in commercial strength, formulation, reduction behavior, and lot quality can lead to shade corrections, longer processing, and rejected fabric. Evaluate suppliers on shade coverage, batch consistency, reduction behavior, and finished-fabric fastness. Give each supplier the same application brief before requesting samples. Include the substrate, pretreatment, dyeing method, target shades, shade depths, finishing route, and customer requirements. A clear brief makes recommendations more relevant and comparisons more reliable. 1. Shade Range Target-Shade Coverage Judge shade coverage against your production requirements. Start with repeat-order colors, high-volume dark shades, and combinations that are difficult to reproduce. For cotton dyeing, select Skythrene® vat dyes against the required shade and process, then verify the selected grades through lab dips on the intended fabric or yarn. Shade cards and screen images support initial selection, but they do not establish color accuracy or fastness on your substrate. Evaluate relevant depths, including pale shades where small hue differences are visible and deep shades where build-up and washing-off become more demanding. For blends, specify which fiber component the vat dye will color and assess the complete processing route. Product Identity and Strength Request the Colour Index name where applicable, commercial grade, physical form, and declared strength. Clarify whether each product is a single colorant or a formulated blend. Products with the same Colour Index name can differ in strength, formulation, dispersion, and application behavior. A shared identity therefore does not establish that two commercial grades are interchangeable. Strength labels also need context. A designation such as 100% or 200% refers to a defined reference basis, which may differ between suppliers. Compare the dosage required to reach the same approved shade instead of assuming that matching labels indicate equal performance. Recipe Compatibility Dyes that perform well individually may behave differently in a combination. Check whether the proposed components have compatible reduction conditions and dyeing characteristics. Ask for trials of complete recipes, especially those used for repeat orders. Assess whether the combination holds its hue within normal production variations. 2. Batch Consistency Quality Control Evidence Request certificates of analysis from separate production lots, supported by an explanation of the release tests. Relevant results may include relative color strength, shade difference against an approved reference, and physical quality checks appropriate to the product form. Confirm the reference batch, measurement procedure, and acceptance limits behind the results. Also confirm lot traceability, retained-sample practices, and notification procedures for formulation or manufacturing changes. These records help resolve discrepancies between an approved sample and a later shipment. Multi-Lot Testing Where practical, evaluate three lots using the same substrate batch, water, auxiliaries, equipment, and processing sequence. This is a practical qualification approach, not a universal minimum. Use two comparisons when necessary: Equal-dosage trials: Apply the same product dosage to identify differences in supplied strength and hue. Matched-depth trials: Adjust dosage to the target depth to compare achievable shade, fastness, and treatment cost. Assess the final color after consistent oxidation, soaping, drying, and conditioning. Keep lot numbers, recipes, test records, and dyed swatches together as references for incoming deliveries. Acceptance Criteria Agree on instrumental and visual assessment conditions before placing a bulk order. Define the color-difference formula, illuminant, observer, measurement setup, and sample preparation. Avoid a universal color-difference limit. Acceptable variation depends on shade, fabric appearance, end use, and customer expectations. Visual checks under relevant lighting also help identify matches that change noticeably between light sources. Finally, confirm how the supplier investigates an out-of-specification lot, communicates findings, and provides corrective action. 3. Reduction Behavior Process-Specific Conditions Vat dyes must be reduced to a soluble leuco form so the colorant can enter the cellulosic fiber. Oxidation then restores the insoluble form. This mechanism makes control of reduction and oxidation central to application performance. Request grade-specific recommendations for reducing agent, alkali, temperature, time, and addition sequence. Confirm whether stock-vat preparation or another application procedure is recommended. Account for the differences between continuous and exhaust vat dyeing. The available reduction time, application sequence, and exposure to air vary by process. A grade approved for one route should still be verified before use in another. Reduction Completeness and Stability Evaluate whether the dye reaches an adequately reduced state within the available processing time. Record residual particles or deposits, penetration, levelness, and final shade. Then assess stability within your normal operating window. Small, controlled variations in temperature, time, or chemical addition can help reveal whether a recipe is robust enough for production. Follow product-specific guidance, since excessive reduction can damage some vat dyes and cause irreversible shade changes. If redox potential is monitored, define the electrode and reference system, temperature, calibration checks, and measurement procedure. A reading without this context is an unreliable basis for comparing suppliers. Record chemical consumption, cycle time, and correction frequency alongside reduction speed. Auxiliary Compatibility Test the selected dyes with the textile dyeing auxiliaries intended for production. Confirm compatibility with the required alkalinity, temperature, reducing conditions, and equipment. Wetting, dispersion, water hardness, and foam can all influence uniformity. For applications requiring rapid wetting and penetration, Sylic P1400 wetting agent has an anionic/nonionic character and is used in pretreatment, dyeing, and finishing. Reference dosages are 0.5–2 g/L for intermittent processing and 2–6 g/L for continuous processing. Use these ranges as trial starting points, then check penetration, foam, and compatibility at the

Explore More »

Contact Us for Textile Auxiliaries and Dyes

Contact Skychem Group for more chemical solutions, If you have questions or need more information, please contact us.
We will respond within 24 hours

Get a project quote

Please tell us the requirements, the country and the application.

Scroll to Top
Email WhatsApp

Contact Us for Textile Auxiliaries and Dyes

Contact Skychem Group for more chemical solutions, If you have questions or need more information, please contact us.
We will respond within 24 hours