...

Contact Skychem Group for more chemical solutions, If you have questions or need more information, please contact us.
Respond within 24 hours

How to Dye Polyester Fleece Fabric?

Dyeing polyester fleece is not the same as dyeing a flat polyester knit. The raised pile slows wet-out, changes how shade is perceived, and makes surface cleanliness more important for rubbing and appearance. This guide focuses on fleece-specific controls so mills and buyers can get stable shade and fastness without overcorrecting recipes.

Dyes for PET Fleece

Polyester fleece is dyed with disperse dyes, but the fleece surface changes what matters most in dye selection. Because the pile scatters light, the same recipe can read lighter on fleece than on smooth fabric, especially in pale and medium shades. At the same time, any dispersion weakness shows up quickly as specks or a dull cast on the pile.

For bulk fleece programs, select disperse dyes that stay stable through high-temperature circulation, deliver strong build-up for navy and black, and keep rubbing and wash performance acceptable on a brushed pile surface. Fleece highlights specks, surface stain, and tone drift more than flat polyester, so dye dispersion quality and fastness balance matter as much as shade strength.
Dyed Fleece Fabric

Before Dyeing

Wet-out for bulky fleece

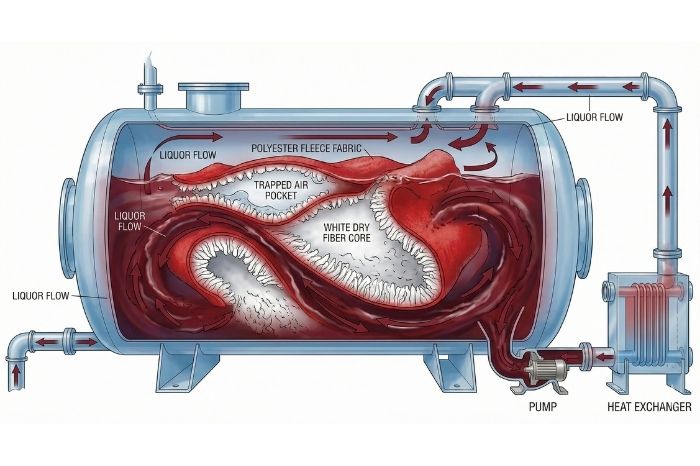
Most fleece problems start early, before shade has even developed. If the pile does not wet evenly, you can lock in bars and patchiness that no later correction fully fixes. Treat wet-out as a controlled step, not a quick prefill.

A textile wetting agent with strong penetration and low-foam behavior helps the dye liquor move through bulky fleece faster and more evenly, so both the pile and the ground knit start the process in the same condition. This reduces early-stage wet-out delays that often lead to bars, patchiness, and inconsistent depth in jet and overflow machines, where turbulence and foam can interfere with liquor contact.
Control hardness and metal ions

Hardness and trace metals can destabilize disperse dye dispersion and increase the chance of specks, dirty shade, or re-deposition during cooling and rinsing. Even stable operations can drift with seasonal water changes.

A textile sequestering agent helps control calcium, magnesium, and trace metal ions that can destabilize disperse dye dispersions and contribute to specks, dull tone, or re-deposition during cooling and rinsing. Keeping ion interference under control improves bath stability, supports cleaner shades on fleece piles, and reduces lot-to-lot variation when water quality shifts across seasons or different supply sources.

HT Exhaust Dyeing

Bath make-up and dosing

On fleece, dosing discipline is more important than long explanations. Poor dispersion or shock additions often show as dots and cloudy tone on the pile. Pre-disperse properly, keep circulation stable, and avoid local high concentration zones when adding dyes and auxiliaries.

Ramp, hold, cool

Heating rate is a key fleece lever. A controlled ramp gives time for migration and leveling through the bulky structure before fixation dominates. If you heat too fast, you can fix uneven penetration into visible bars. Holding at peak temperature should be just long enough to stabilize shade; excessive holding increases cost and can raise surface dye load. Controlled cooling helps reduce dispersion instability and re-deposition risk.

Rinse and check surface dye

Rinsing on fleece is not a formality. It directly impacts rubbing fastness because the pile surface retains loosely held dye more easily than flat fabrics. If rubbing complaints occur later, the root cause is often incomplete removal of surface dye before finishing.

Clearing and Shade Stability

When to run reduction clearing

Reduction clearing is commonly the step that makes fleece “clean” enough for real-world use, especially on deep shades and on fabrics that will face heat or abrasion. Use it based on requirement, not habit.

  • Deep or dark shades where surface dye load is high
  • Strict rubbing fastness targets on the pile
  • Sublimation resistance needed due to heat setting or garment processing

Re-deposition control

Clearing is only effective if removed dye does not return to the fabric. Maintain good liquor exchange, keep dispersion stable through the sequence, and avoid abrupt cooling or poor drainage that can drive re-deposition onto the pile.
Finishing for Fleece Hand

Silicone softener options for fleece

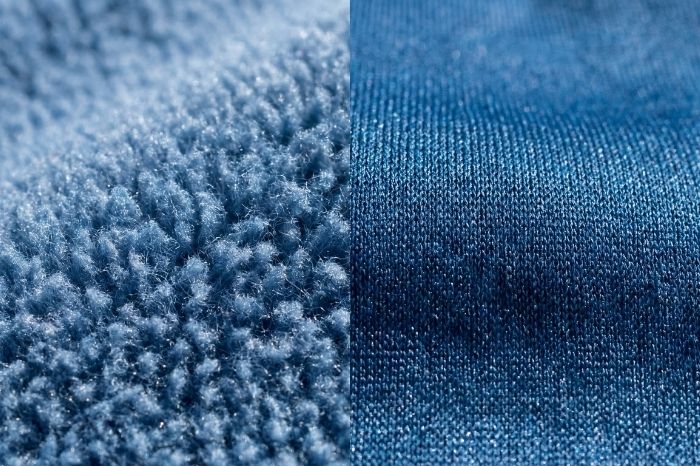
Fleece buyers evaluate the fabric first by hand, loft, and surface smoothness, and dyeing plus clearing can leave the pile feeling dry or flat. A silicone softener for textiles is commonly applied to rebuild a fuller, softer touch while maintaining controlled shade appearance and acceptable rubbing performance on the brushed surface.

Hydrophilic vs standard hand feel

Choose finishing direction based on the product spec. Hydrophilic systems fit performance fleece where moisture handling matters, while standard silicone systems fit blankets and casual fleece where plush hand is the top priority.

Shade and fastness compatibility

Finishing can shift shade and can change rubbing behavior on pile surfaces. Validate compatibility on the actual fleece construction and shade depth, then lock the finishing recipe for bulk to avoid lot-to-lot drift.

QC for Bulk Lots

Shade check on pile fabrics

Shade evaluation on fleece needs consistent handling. Changes in pile direction or surface state can look like shade variation even when dyeing is consistent.

  • Keep pile direction consistent during evaluation
  • Standardize lighting and viewing angle across teams
  • Compare like-with-like surface condition (brushed or unbrushed)

Key fastness tests

For most fleece programs, the practical core is wash fastness and dry and wet rubbing fastness. Add sublimation resistance when the end use includes high heat exposure. Align the test set to the buyer’s end-use requirement so you are not over-testing or missing a real risk.
Next Steps

For mills and sourcing teams running polyester fleece across multiple shades and repeat seasons, consistent results depend on clear technical alignment, not only on dye choice. Sharing fabric construction, target depth, machine type, and fastness requirements helps the supplier respond with a workable package covering disperse dye selection, wet-out and water control, clearing decisions, and finishing compatibility for fleece hand and performance. Use contact us to send your specifications: https://skychemi.com/contact-us/


Recommended readings:

  1. How to Dye Cationic Fabric?
  2. How to Dye Polyester Fabric?
  3. How to Dye Nylon Fabric?

Sandy

With years of experience in chemical dyes and textile auxiliaries, I’m dedicated to sharing insights into the latest technologies, sustainable innovations, and market trends.

Recent Articles

Cotton terry compares water absorbency.

Silicone Softener Problems: Causes and Solutions for Yellowing, Spots and Hydrophilicity Loss

Table of Contents Yellowing Issues Common Causes Heat and Curing Effects Prevention Tips Fixing Yellowed Fabric Spots and Uneven Deposits Causes of Spots Emulsion Stability Prevention Techniques Troubleshooting Steps Shade Change After Softening Why Shade Change Happens Dye Compatibility Minimizing Shade Variation Loss of Hydrophilicity Why Absorbency Drops Balancing Softness and Absorbency Hydrophilic Softener Options Best Practices for Application Correct Dosage and Dilution Padding and Drying Parameters Quality Control Testing Conclusion FAQs What causes silicone softener to turn fabric yellow? How can I prevent spots after softener treatment? Why does fabric shade change after softening? How do I restore hydrophilicity after softener use? Silicone softeners are among the most widely used finishing chemicals in textile mills, valued for the smooth hand feel, drape, and durability they bring to fabric. But they can also be a source of real headaches on the production floor. Yellowing on white goods, oily spots after padding, unexpected shade shifts, and a sudden loss of water absorbency are among the most common complaints raised by finishers, dyers, and quality teams worldwide. Nearly every one of these problems traces back to a small number of root causes: the wrong silicone chemistry for the substrate, poor emulsion stability, incorrect bath conditions, or curing parameters pushed past the chemistry’s limits. Once the underlying fiber and polymer behavior is understood, most of these issues can be prevented with a better product choice, a small process adjustment, or tighter quality control at the padding stage. This article walks through each problem in turn, covering what causes it and how to prevent or correct it. Yellowing Issues Yellowing is one of the most commonly reported complaints with silicone softeners, especially on white and pastel fabrics where even a slight color shift is immediately visible. Common Causes Most yellowing traces back to the amine content in the silicone polymer. Amino-modified silicones deliver excellent softness because the amine groups anchor strongly to the fiber surface, but those same groups are chemically reactive and prone to oxidation. A few conditions make the problem worse: Contamination from iron or other transition metals in the bath water Residual chlorine left over from bleaching Low-quality or inconsistent raw materials in the softener itself Heat and Curing Effects Yellowing often becomes visible only after the fabric passes through the stenter. Thermal oxidation of free amine groups during curing generates chromophores, the compounds responsible for the yellow tint, and this effect grows more pronounced as yellowing can become more pronounced when curing temperatures exceed the recommended range for the specific silicone softener and fabric. A second, less obvious mechanism is gas fading, sometimes called NOx yellowing, where atmospheric nitrogen oxides react with amine groups during storage or transport. This can occur without any heat exposure at all, which is why fabric sometimes yellows weeks after it leaves the finishing line, long after the mill has moved on to the next order. Prevention Tips A few adjustments go a long way toward keeping fabric bright: Choose a softener with a lower amine value for light and white goods Keep curing temperature and dwell time within the supplier’s recommended window Use demineralized water to reduce metal ion contamination Add an antioxidant, or switch to a block silicone rather than a straight amino silicone, for goods that will be stored or shipped over long distances Fixing Yellowed Fabric Once yellowing has occurred, options are limited. Mild cases can sometimes be improved with a peroxide or reducing bleach treatment, though this carries some risk to fabric strength and should always be tested on a sample first. In most cases, the more reliable fix is prevention on the next batch rather than correction after the fact, which is why product selection and process control matter so much upfront. Cause Recommended Fix High amine value silicone Switch to a low amine value or block silicone softener Excess curing temperature Reduce stenter temperature and dwell time to supplier guidance Metal ion contamination Use demineralized or softened process water Storage-related gas fading Improve ventilation, reduce storage time, add antioxidant protection For fabrics where yellowing resistance is a priority, Sylic F3575 Soft and Smooth Silicone Oil is a high-concentration self-emulsifying silicone oil with 64 to 66 percent solid content, formulated for low yellowing along with high bath stability and compatibility. It suits cotton, polyester, and blended fabrics that need to stay bright through curing, typically applied at 5 to 20 g/L in padding or 1 to 5 percent o.w.f. in exhaust dyeing. Spots and Uneven Deposits Oily-looking spots or uneven patches after softener application are frustrating because they often only appear after the fabric has dried, which means the problem is discovered late in the process. Causes of Spots Spots usually come from poor emulsion stability. When the silicone particles in the bath are too large, or the emulsion breaks under mechanical shear, agitation, or temperature swings, the oil phase separates and deposits unevenly on the fabric surface instead of spreading uniformly across the fibers. Emulsion Stability Several bath conditions influence how stable an emulsion stays through a padding run: pH, which should generally sit in the weakly acidic range for cationic silicone emulsions Water hardness and electrolyte content, both of which can destabilize the emulsion at higher levels Mixing sequence, since adding chemicals to the bath in the wrong order can cause premature coalescence before the fabric even enters the pad Prevention Techniques Pre-diluting the softener before it enters the bath, rather than adding concentrate directly, gives the emulsion time to disperse evenly and is the single most effective safeguard against spotting. Beyond that, maintaining a consistent bath temperature and controlling water hardness both reduce risk, and filtering the bath periodically during long runs helps catch early signs of emulsion breakdown before they show up on fabric. Self-emulsifying silicone oils, which carry built-in emulsifier groups in the polymer structure, disperse more evenly with simple agitation and are a good option where spotting is a recurring issue. Troubleshooting Steps If spots appear, start by checking the bath for visible

Explore More »
Solvent dye applications in plastics, inks, and coatings.

How to Choose the Right Solvent Dye for Plastics, Inks and Coating?

Table of Contents What Are Solvent Dyes? Why Use Solvent Dyes Instead of Pigments? Key Factors for Selecting Solvent Dyes Solubility Heat Resistance Light Fastness Migration Resistance Solvent Dye Selection by Application Plastics Printing Inks Coatings Recommended Solvent Dye Grades FAQs Can solvent dyes and pigments be combined in the same formulation? Which solvents suit gravure and flexographic inks? How is thermal stability tested? What causes dye migration in packaging? This guide compares solvent dyes for plastics, printing inks, and coatings by solubility, heat resistance, light fastness, and migration performance, so formulators can match the right grade to a specific solvent system, processing temperature, and end-use application. What Are Solvent Dyes? Solvent dyes are colorants that dissolve fully into the host medium at a molecular level, giving plastics, printing inks, and coatings their characteristic transparency, brightness, and consistent shade. Choosing a solvent dye for plastics, printing inks, or coatings comes down to three practical questions: does it dissolve cleanly in the carrier system, will it hold up at the required processing temperature, and will it stay in place once the product ships. Why Use Solvent Dyes Instead of Pigments? Pigments form particle suspensions that scatter light, which can introduce haze and uneven color strength in transparent parts. Solvent dyes dissolve fully in the host medium, producing clear, vibrant color even in thin films or lightly tinted plastics. For applications where transparency and color intensity matter more than opacity, such as clear plastic components, flexible packaging inks, or wood stains, solvent dyes are typically the better fit. Key Factors for Selecting Solvent Dyes Four factors most often determine whether a solvent dye grade performs as expected in a given application: solubility in the carrier system, heat resistance during processing, light fastness under end-use exposure, and migration resistance once the product is in service. Solubility Solvent dyes only perform as intended when they fully dissolve in the carrier a formulator is already using. Compatibility with the specific solvent blend determines both color strength and clarity in the finished product. Ketones and Esters. Ketones such as MEK and acetone, along with esters such as ethyl acetate and butyl acetate, are common carriers in gravure and flexographic printing inks. Solvent dyes formulated for these systems typically dissolve quickly and leave minimal residue, which supports consistent print density. Aromatic Hydrocarbons. Toluene and xylene remain widely used in industrial coatings and some legacy ink systems. Solubility in aromatic hydrocarbons can vary more between dye chemistries than it does in ketone or ester systems, so each grade needs to be checked against the specific carrier rather than assumed compatible by solvent class. Alcohols. Ethanol and isopropanol appear in a range of coatings and lower-VOC formulations. Solvent dye solubility tends to be more limited across the board in alcohol systems, which makes it one of the first properties worth confirming before committing to a grade. Because solubility varies by individual dye chemistry rather than by solvent class alone, it is worth verifying a dye’s solubility profile against the exact carrier solvent before finalizing a formulation. Heat Resistance Processing temperature is often the deciding factor between two otherwise similar solvent dyes. Thermal stability depends heavily on the underlying dye chemistry, and choosing incorrectly can lead to shade shift, gassing, or reduced clarity during melt processing or curing. Anthraquinone Dyes. Many anthraquinone-based solvent dyes offer excellent thermal stability and are commonly selected for high-temperature plastics applications such as polycarbonate and ABS, though the exact thermal ceiling varies by grade and should be confirmed for each specific dye. Azo Dyes. Azo-based solvent dyes typically have a lower thermal ceiling than anthraquinone types and generally suit lower-temperature processing such as polystyrene. They are often the more cost-effective option when the application does not require extended heat exposure. Property Anthraquinone Dyes Azo Dyes Typical thermal ceiling Generally higher, but varies by grade Generally lower, but varies by grade Light fastness Generally superior UV resistance Adequate for short-term or indoor use Common resins Polycarbonate, ABS Polystyrene Relative cost Higher Lower Light Fastness Light fastness measures how well a color resists fading under UV or prolonged light exposure. Anthraquinone dyes generally offer superior light fastness and are better suited to outdoor or long-term exposure applications, while azo dyes are typically adequate for short-term or indoor use. For coatings and plastics that will see extended outdoor exposure, light fastness is worth weighing alongside heat resistance rather than treating it as a separate afterthought. Migration Resistance Migration becomes a concern whenever a colored plastic, film, or coating sits in direct or indirect contact with another material over time. A dye that migrates can bleed into adjacent layers, packaging contents, or surrounding surfaces, affecting both appearance and, in some cases, regulatory compliance. Molecular Weight and Migration. Solvent dyes with higher molecular weight and lower solubility in the contacting medium generally show better migration resistance. This matters most in multilayer plastic films or packaging structures, where dye movement between layers can show up as discoloration or staining over time. Testing Conditions. Migration behavior should be assessed under the temperature and humidity conditions the finished product will actually see. Results measured at room temperature do not reliably predict performance in warmer storage or transport environments, so testing under real-world conditions is essential before a grade is finalized. For packaging destined for food-contact applications, migration testing is typically benchmarked against established frameworks such as the EU regulation on plastic materials intended for food contact. Colorants generally fall outside that regulation’s specific substance list, but they are still subject to its general safety requirements, so this remains a useful reference point when setting internal migration limits. Solvent Dye Selection by Application Once solubility, heat, light, and migration requirements are defined, the right solvent dye also depends on the specific application it will be used in. Plastics In plastics processing, common resins include polystyrene, ABS, acrylics, polycarbonate, and PET. Solvent dyes deliver transparent, uniform coloring that pigments cannot always match, especially in clear or lightly tinted parts. Printing Inks For flexographic, gravure,

Explore More »
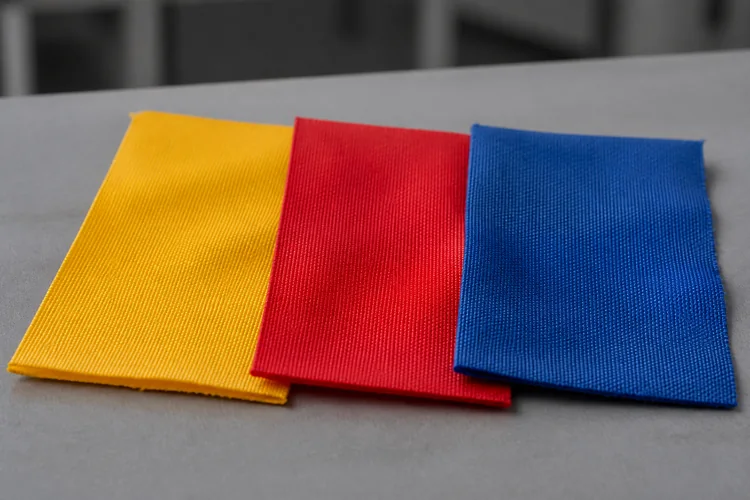
Yellow, red, and blue nylon swatches representing a compatible trichromatic acid dye set.

Trichromatic Acid Dye Selection for Consistent Nylon Shades

Table of Contents Understanding Strike Rate Factors Influencing Strike Rate Matching Strike Rates in a Combination The Role of pH in Dye Uptake pH Ranges by Dye Class Controlling pH During Dyeing Trichromatic Selection Principles Choosing Compatible Yellow, Red, Blue Typical Trichromatic Acid Dye Combinations for Nylon Light Shade Trichromatic Combination Deep Shade Trichromatic Combination Migration and Buildup Properties Avoiding Shade Shift Practical Recipe Guidelines Lab Trial Checklist FAQs What causes uneven dyeing with acid dyes on nylon? How does pH control affect reproducibility? What makes a trichromatic combination reliable? Nylon dyeing rewards precision. Acid dyes bond well with polyamide fibers, but shade consistency depends on how closely strike rate, pH, and trichromatic combinations are controlled together. A small mismatch in any one variable can shift a shade off standard, even when the recipe looks correct on paper. This article breaks down the practical factors that keep acid dye combinations compatible on nylon. Understanding Strike Rate Strike rate describes how quickly a dye moves from the bath onto the fiber. On nylon, this speed depends on dye structure, temperature ramp, and the number of available dye sites on the substrate. A dye with a fast strike rate can produce uneven color if it exhausts before the bath fully penetrates the goods, particularly on tightly constructed knits or dense yarns. Factors Influencing Strike Rate Three variables have the greatest effect on how fast a given acid dye takes up on nylon: Molecular size and structure: smaller, more mobile molecules tend to migrate and level more readily, while larger or more linear structures strike faster but migrate less once fixed. Electrolyte concentration: higher salt levels in the bath slow strike by increasing ionic competition at the fiber surface, which can help leveling but may reduce total exhaustion if not balanced correctly. Temperature ramp speed: a ramp that heats too quickly gives the dye little time to migrate before fixation, raising the risk of streaks or tailing on the goods. Matching Strike Rates in a Combination When combining dyes for a shade, each component should have a comparable strike rate. If one dye in a mix strikes noticeably faster than the others, it dominates the early stages of dyeing and shifts the shade as the bath progresses. This is one of the most common causes of reproducibility problems in nylon dyehouses, especially when recipes are adjusted without checking how the new combination behaves as a system rather than as individual dyes. The Role of pH in Dye Uptake Acid dyes require an acidic bath to bond effectively with the amine groups on nylon fiber. pH does more than set the chemical environment; it also governs how fast dye uptake occurs and how much correction is possible once dyeing has started. pH Ranges by Dye Class Different acid dye classes are formulated to perform within specific pH windows. Working outside that window changes uptake speed and can affect fastness properties. Dye Class Typical pH Range Uptake Behavior Leveling acid dyes pH 5 to 6 Slower strike, good migration, easier to correct Milling acid dyes pH 4.5 to 5.5 Moderate strike, less forgiving on unlevel dyeing Metal complex acid dyes pH 4 to 5 Faster strike, stronger fastness, tighter process control needed These ranges are starting references. Actual performance depends on the specific dye grade, liquor ratio, and machine type, so lab confirmation on the intended substrate remains necessary before scaling to bulk. Controlling pH During Dyeing Holding pH steady throughout the cycle matters as much as setting the correct starting point. A pH that drifts upward during dyeing slows uptake and can leave the shade pale or uneven, while a sharp early drop can cause the dye to strike too fast for proper migration. Buffering systems and controlled acid addition keep the bath within range from start to finish. Leveling agents and buffering auxiliaries formulated for pH and strike control help stabilize uptake speed across different fabric constructions and machine conditions, particularly on constructions prone to rapid initial strike. Trichromatic Selection Principles Trichromatic dyeing uses a yellow, red, and blue dye to build a wide range of shades from a small working palette. Compatibility across these three dyes determines how predictable the resulting shades will be, both in the lab and in bulk. Choosing Compatible Yellow, Red, Blue A workable trichromatic set should share similar strike rates, similar pH sensitivity, and comparable migration behavior. Mismatched components can produce shade drift between lab dips and production batches, even when the total dye concentration is correct. The Skyacido Acid Dyes, formulated specifically for polyamide dyeing, offers a wide shade gamut with strong inter-shade combinability, which supports matching yellow, red, and blue components as a coordinated set rather than selecting each color independently based on shade alone. The table below outlines what to check across each primary when building a trichromatic set: Component Strike Rate Check pH Sensitivity Migration Behavior Yellow Compare exhaustion curve against red and blue Note shift point where uptake accelerates Confirm redistribution at hold temperature Red Compare exhaustion curve against yellow and blue Note shift point where uptake accelerates Confirm redistribution at hold temperature Blue Compare exhaustion curve against yellow and red Note shift point where uptake accelerates Confirm redistribution at hold temperature Running this comparison during lab dip development, rather than after a bulk batch shows shade drift, catches mismatches while they are still inexpensive to correct. Typical Trichromatic Acid Dye Combinations for Nylon In practical nylon dyeing, trichromatic combinations are usually selected according to shade depth, buildup requirement, and compatibility between dyes. Different combinations may be required for light shades and deep shades to maintain balanced exhaustion, migration, and shade reproducibility. Light Shade Trichromatic Combination For light and medium shades, dyes with good migration performance and moderate strike behavior are preferred to achieve excellent leveling and shade correction ability. A typical light shade combination may include: Trichromatic Position Example Acid Dye Yellow Skyacido Yellow 199 Red Skyacido Red 337 Blue Skyacido Blue 324 This combination provides good compatibility and is

Explore More »
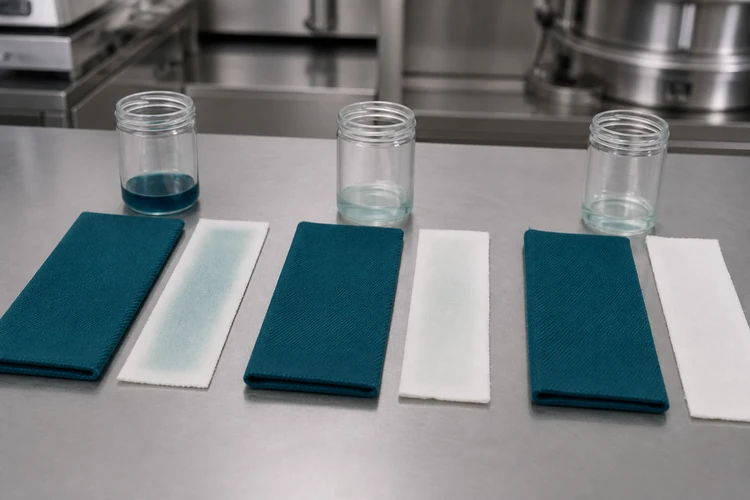
2. Low-temperature soaping leaves clearer wash liquor and less staining on adjacent white cotton strips.

Reactive Dye Soaping Guide: Better Wash Fastness, Less Back-Staining

Table of Contents What Is Reactive Dye Soaping Role in the Wash-Off Stage Why Unfixed and Hydrolyzed Dye Must Be Removed How Soaping Affects Wash Fastness Removing Hydrolyzed Dye from the Fiber Surface Connection Between Soaping and Fastness Ratings What Causes Back-Staining? Common Sources of Back-Staining Fabrics and Blends Most at Risk Key Process Parameters for Effective Soaping Temperature and Time Liquor Ratio Water Hardness and Sequestering Agents Choosing the Right Soaping Agents Anionic and Nonionic Soaping Agents Matching Agents to Fiber and Shade Depth Low-Temperature Soaping Agent Option: Sylic D2705 Key Benefits Recommended Application Performance Comparison Soaping Process Methods Cold Wash and Hot Wash Sequence One-Bath vs Multi-Step Soaping Role of Fixing Agents After Soaping Best Practices for Consistent Wash Fastness Results FAQs How long should reactive dye soaping take? Can back-staining be fixed after it happens? Does hard water affect soaping performance? Is a separate fixing agent always necessary after soaping? Reactive dye soaping is often treated as a quick step at the end of the dyeing cycle, but it has a direct effect on wash fastness and back-staining outcomes. Getting temperature, time, and agent selection right prevents costly rejects and repeat orders that eat into margins. What Is Reactive Dye Soaping Role in the Wash-Off Stage Soaping takes place after fixation, once the reactive dye has bonded to the fiber under alkaline conditions. Fabric is washed at or near boiling temperature with a detergent or specialty soaping agent to strip away everything that never formed a permanent bond with the fiber. Skipping or shortening this step leaves wash-off incomplete, and the fabric carries a hidden fastness risk that will not surface until later testing or, worse, after it reaches the customer. Why Unfixed and Hydrolyzed Dye Must Be Removed A portion of reactive dye always hydrolyzes in the dyebath instead of reacting with the fiber. Hydrolyzed dye sits loosely on the fabric surface, held only by weak physical attraction rather than a covalent bond. Left in place, it rubs off during handling, bleeds during laundering, and transfers onto lighter fabrics in the same wash load. Soaping is the step designed specifically to remove this residue before it becomes a fastness problem. How Soaping Affects Wash Fastness The quality of soaping determines much of what shows up later in fastness testing. A batch that looks correct on the shade card can still fail to wash or rub fastness if this step was rushed. Removing Hydrolyzed Dye from the Fiber Surface Effective soaping keeps loosened dye suspended in the wash liquor instead of letting it settle back onto the fabric. How completely this happens depends on agitation, liquor ratio, and the dispersing strength of the detergent or soaping agent used. Connection Between Soaping and Fastness Ratings Wash and rub fastness ratings, most commonly evaluated using AATCC colorfastness test methods, largely reflect how much unfixed dye remains after wash-off. A fabric can pass an initial shade check on the lab dip and still fail fastness testing on the bulk batch if soaping ran too briefly or at too low a temperature. What Causes Back-Staining? Common Sources of Back-Staining Back-staining happens when dye that has washed off the dyed fabric redeposits onto undyed or lighter areas in the same bath. The most common causes include: Overloaded soaping baths carrying more hydrolyzed dye than the liquor can hold Insufficient rinsing between soaping and finishing steps Soaping agents with weak dispersing power, which allow free dye particles to settle back onto the fabric Uneven liquor circulation, which creates localized zones of high dye concentration Fabrics and Blends Most at Risk Deep and dark shades generate the highest load of hydrolyzed dye and are the most frequent source of back-staining complaints. Blended fabrics, and any load that mixes dyed and undyed components, are particularly vulnerable, since redeposited dye is far more visible on the lighter portion of the fabric. Key Process Parameters for Effective Soaping Most causes of poor fastness and back-staining trace back to how tightly these three parameters are controlled. Temperature and Time Soaping typically runs at or close to boiling point for five to fifteen minutes, though the ideal combination depends on shade depth and fabric construction. Running the bath too cool slows dye removal, and cutting the time short leaves hydrolyzed dye behind even at the correct temperature. Shade depth Soaping temperature Typical time Light to medium 90 to 95°C 5 to 8 minutes Deep and dark Near boiling (98 to 100°C) 10 to 15 minutes Turquoise and problem shades Near boiling, multi-bath 15 minutes or more per bath This near-boiling range applies to conventional soaping agents. Low-temperature soaping agents are formulated to work effectively at 60 to 80°C instead, cutting energy use without giving up fastness performance (see the Sylic D2705 section below).  Liquor Ratio A tighter liquor ratio concentrates hydrolyzed dye in a smaller volume of water, which increases the risk of redeposition before it can be flushed out. Mills running jet or overflow machines at lower liquor ratios should compensate with stronger dispersing agents or an added rinse cycle. Water Hardness and Sequestering Agents Calcium, magnesium, and iron in the water supply interfere with soaping agent performance and can leave a hazy or uneven finish. A sequestering agent, such as Sylic P1501B, an anionic chelating dispersant with a pH of 2.5 to 4.0 in a 1% solution, binds these ions before soaping begins and lets the soaping agent perform as intended. Choosing the Right Soaping Agents Anionic and Nonionic Soaping Agents Anionic soaping agents are widely used for their strong dispersing action, while nonionic types perform better in hard water and at lower temperatures. Both types are available within a dyeing auxiliary range formulated for stability in alkaline baths and low-foam performance in jet machines. Matching Agents to Fiber and Shade Depth Cotton and other cellulosic fibers generally respond well to anionic soaping agents. Blends containing synthetic fibers may need a nonionic option instead, to avoid staining the more sensitive synthetic component. Deeper shades typically call

Explore More »

Contact Us for Textile Auxiliaries and Dyes

Contact Skychem Group for more chemical solutions, If you have questions or need more information, please contact us.
We will respond within 24 hours

Get a project quote

Tell us your project requirements, country, and intended application.

Sandy

With years of experience in chemical dyes and textile auxiliaries, I’m dedicated to sharing insights into the latest technologies, sustainable innovations, and market trends.

Recent Articles

Cotton terry compares water absorbency.

Silicone Softener Problems: Causes and Solutions for Yellowing, Spots and Hydrophilicity Loss

Table of Contents Yellowing Issues Common Causes Heat and Curing Effects Prevention Tips Fixing Yellowed Fabric Spots and Uneven Deposits Causes of Spots Emulsion Stability Prevention Techniques Troubleshooting Steps Shade Change After Softening Why Shade Change Happens Dye Compatibility Minimizing Shade Variation Loss of Hydrophilicity Why Absorbency Drops Balancing Softness and Absorbency Hydrophilic Softener Options Best Practices for Application Correct Dosage and Dilution Padding and Drying Parameters Quality Control Testing Conclusion FAQs What causes silicone softener to turn fabric yellow? How can I prevent spots after softener treatment? Why does fabric shade change after softening? How do I restore hydrophilicity after softener use? Silicone softeners are among the most widely used finishing chemicals in textile mills, valued for the smooth hand feel, drape, and durability they bring to fabric. But they can also be a source of real headaches on the production floor. Yellowing on white goods, oily spots after padding, unexpected shade shifts, and a sudden loss of water absorbency are among the most common complaints raised by finishers, dyers, and quality teams worldwide. Nearly every one of these problems traces back to a small number of root causes: the wrong silicone chemistry for the substrate, poor emulsion stability, incorrect bath conditions, or curing parameters pushed past the chemistry’s limits. Once the underlying fiber and polymer behavior is understood, most of these issues can be prevented with a better product choice, a small process adjustment, or tighter quality control at the padding stage. This article walks through each problem in turn, covering what causes it and how to prevent or correct it. Yellowing Issues Yellowing is one of the most commonly reported complaints with silicone softeners, especially on white and pastel fabrics where even a slight color shift is immediately visible. Common Causes Most yellowing traces back to the amine content in the silicone polymer. Amino-modified silicones deliver excellent softness because the amine groups anchor strongly to the fiber surface, but those same groups are chemically reactive and prone to oxidation. A few conditions make the problem worse: Contamination from iron or other transition metals in the bath water Residual chlorine left over from bleaching Low-quality or inconsistent raw materials in the softener itself Heat and Curing Effects Yellowing often becomes visible only after the fabric passes through the stenter. Thermal oxidation of free amine groups during curing generates chromophores, the compounds responsible for the yellow tint, and this effect grows more pronounced as yellowing can become more pronounced when curing temperatures exceed the recommended range for the specific silicone softener and fabric. A second, less obvious mechanism is gas fading, sometimes called NOx yellowing, where atmospheric nitrogen oxides react with amine groups during storage or transport. This can occur without any heat exposure at all, which is why fabric sometimes yellows weeks after it leaves the finishing line, long after the mill has moved on to the next order. Prevention Tips A few adjustments go a long way toward keeping fabric bright: Choose a softener with a lower amine value for light and white goods Keep curing temperature and dwell time within the supplier’s recommended window Use demineralized water to reduce metal ion contamination Add an antioxidant, or switch to a block silicone rather than a straight amino silicone, for goods that will be stored or shipped over long distances Fixing Yellowed Fabric Once yellowing has occurred, options are limited. Mild cases can sometimes be improved with a peroxide or reducing bleach treatment, though this carries some risk to fabric strength and should always be tested on a sample first. In most cases, the more reliable fix is prevention on the next batch rather than correction after the fact, which is why product selection and process control matter so much upfront. Cause Recommended Fix High amine value silicone Switch to a low amine value or block silicone softener Excess curing temperature Reduce stenter temperature and dwell time to supplier guidance Metal ion contamination Use demineralized or softened process water Storage-related gas fading Improve ventilation, reduce storage time, add antioxidant protection For fabrics where yellowing resistance is a priority, Sylic F3575 Soft and Smooth Silicone Oil is a high-concentration self-emulsifying silicone oil with 64 to 66 percent solid content, formulated for low yellowing along with high bath stability and compatibility. It suits cotton, polyester, and blended fabrics that need to stay bright through curing, typically applied at 5 to 20 g/L in padding or 1 to 5 percent o.w.f. in exhaust dyeing. Spots and Uneven Deposits Oily-looking spots or uneven patches after softener application are frustrating because they often only appear after the fabric has dried, which means the problem is discovered late in the process. Causes of Spots Spots usually come from poor emulsion stability. When the silicone particles in the bath are too large, or the emulsion breaks under mechanical shear, agitation, or temperature swings, the oil phase separates and deposits unevenly on the fabric surface instead of spreading uniformly across the fibers. Emulsion Stability Several bath conditions influence how stable an emulsion stays through a padding run: pH, which should generally sit in the weakly acidic range for cationic silicone emulsions Water hardness and electrolyte content, both of which can destabilize the emulsion at higher levels Mixing sequence, since adding chemicals to the bath in the wrong order can cause premature coalescence before the fabric even enters the pad Prevention Techniques Pre-diluting the softener before it enters the bath, rather than adding concentrate directly, gives the emulsion time to disperse evenly and is the single most effective safeguard against spotting. Beyond that, maintaining a consistent bath temperature and controlling water hardness both reduce risk, and filtering the bath periodically during long runs helps catch early signs of emulsion breakdown before they show up on fabric. Self-emulsifying silicone oils, which carry built-in emulsifier groups in the polymer structure, disperse more evenly with simple agitation and are a good option where spotting is a recurring issue. Troubleshooting Steps If spots appear, start by checking the bath for visible

Explore More »
Solvent dye applications in plastics, inks, and coatings.

How to Choose the Right Solvent Dye for Plastics, Inks and Coating?

Table of Contents What Are Solvent Dyes? Why Use Solvent Dyes Instead of Pigments? Key Factors for Selecting Solvent Dyes Solubility Heat Resistance Light Fastness Migration Resistance Solvent Dye Selection by Application Plastics Printing Inks Coatings Recommended Solvent Dye Grades FAQs Can solvent dyes and pigments be combined in the same formulation? Which solvents suit gravure and flexographic inks? How is thermal stability tested? What causes dye migration in packaging? This guide compares solvent dyes for plastics, printing inks, and coatings by solubility, heat resistance, light fastness, and migration performance, so formulators can match the right grade to a specific solvent system, processing temperature, and end-use application. What Are Solvent Dyes? Solvent dyes are colorants that dissolve fully into the host medium at a molecular level, giving plastics, printing inks, and coatings their characteristic transparency, brightness, and consistent shade. Choosing a solvent dye for plastics, printing inks, or coatings comes down to three practical questions: does it dissolve cleanly in the carrier system, will it hold up at the required processing temperature, and will it stay in place once the product ships. Why Use Solvent Dyes Instead of Pigments? Pigments form particle suspensions that scatter light, which can introduce haze and uneven color strength in transparent parts. Solvent dyes dissolve fully in the host medium, producing clear, vibrant color even in thin films or lightly tinted plastics. For applications where transparency and color intensity matter more than opacity, such as clear plastic components, flexible packaging inks, or wood stains, solvent dyes are typically the better fit. Key Factors for Selecting Solvent Dyes Four factors most often determine whether a solvent dye grade performs as expected in a given application: solubility in the carrier system, heat resistance during processing, light fastness under end-use exposure, and migration resistance once the product is in service. Solubility Solvent dyes only perform as intended when they fully dissolve in the carrier a formulator is already using. Compatibility with the specific solvent blend determines both color strength and clarity in the finished product. Ketones and Esters. Ketones such as MEK and acetone, along with esters such as ethyl acetate and butyl acetate, are common carriers in gravure and flexographic printing inks. Solvent dyes formulated for these systems typically dissolve quickly and leave minimal residue, which supports consistent print density. Aromatic Hydrocarbons. Toluene and xylene remain widely used in industrial coatings and some legacy ink systems. Solubility in aromatic hydrocarbons can vary more between dye chemistries than it does in ketone or ester systems, so each grade needs to be checked against the specific carrier rather than assumed compatible by solvent class. Alcohols. Ethanol and isopropanol appear in a range of coatings and lower-VOC formulations. Solvent dye solubility tends to be more limited across the board in alcohol systems, which makes it one of the first properties worth confirming before committing to a grade. Because solubility varies by individual dye chemistry rather than by solvent class alone, it is worth verifying a dye’s solubility profile against the exact carrier solvent before finalizing a formulation. Heat Resistance Processing temperature is often the deciding factor between two otherwise similar solvent dyes. Thermal stability depends heavily on the underlying dye chemistry, and choosing incorrectly can lead to shade shift, gassing, or reduced clarity during melt processing or curing. Anthraquinone Dyes. Many anthraquinone-based solvent dyes offer excellent thermal stability and are commonly selected for high-temperature plastics applications such as polycarbonate and ABS, though the exact thermal ceiling varies by grade and should be confirmed for each specific dye. Azo Dyes. Azo-based solvent dyes typically have a lower thermal ceiling than anthraquinone types and generally suit lower-temperature processing such as polystyrene. They are often the more cost-effective option when the application does not require extended heat exposure. Property Anthraquinone Dyes Azo Dyes Typical thermal ceiling Generally higher, but varies by grade Generally lower, but varies by grade Light fastness Generally superior UV resistance Adequate for short-term or indoor use Common resins Polycarbonate, ABS Polystyrene Relative cost Higher Lower Light Fastness Light fastness measures how well a color resists fading under UV or prolonged light exposure. Anthraquinone dyes generally offer superior light fastness and are better suited to outdoor or long-term exposure applications, while azo dyes are typically adequate for short-term or indoor use. For coatings and plastics that will see extended outdoor exposure, light fastness is worth weighing alongside heat resistance rather than treating it as a separate afterthought. Migration Resistance Migration becomes a concern whenever a colored plastic, film, or coating sits in direct or indirect contact with another material over time. A dye that migrates can bleed into adjacent layers, packaging contents, or surrounding surfaces, affecting both appearance and, in some cases, regulatory compliance. Molecular Weight and Migration. Solvent dyes with higher molecular weight and lower solubility in the contacting medium generally show better migration resistance. This matters most in multilayer plastic films or packaging structures, where dye movement between layers can show up as discoloration or staining over time. Testing Conditions. Migration behavior should be assessed under the temperature and humidity conditions the finished product will actually see. Results measured at room temperature do not reliably predict performance in warmer storage or transport environments, so testing under real-world conditions is essential before a grade is finalized. For packaging destined for food-contact applications, migration testing is typically benchmarked against established frameworks such as the EU regulation on plastic materials intended for food contact. Colorants generally fall outside that regulation’s specific substance list, but they are still subject to its general safety requirements, so this remains a useful reference point when setting internal migration limits. Solvent Dye Selection by Application Once solubility, heat, light, and migration requirements are defined, the right solvent dye also depends on the specific application it will be used in. Plastics In plastics processing, common resins include polystyrene, ABS, acrylics, polycarbonate, and PET. Solvent dyes deliver transparent, uniform coloring that pigments cannot always match, especially in clear or lightly tinted parts. Printing Inks For flexographic, gravure,

Explore More »
Yellow, red, and blue nylon swatches representing a compatible trichromatic acid dye set.

Trichromatic Acid Dye Selection for Consistent Nylon Shades

Table of Contents Understanding Strike Rate Factors Influencing Strike Rate Matching Strike Rates in a Combination The Role of pH in Dye Uptake pH Ranges by Dye Class Controlling pH During Dyeing Trichromatic Selection Principles Choosing Compatible Yellow, Red, Blue Typical Trichromatic Acid Dye Combinations for Nylon Light Shade Trichromatic Combination Deep Shade Trichromatic Combination Migration and Buildup Properties Avoiding Shade Shift Practical Recipe Guidelines Lab Trial Checklist FAQs What causes uneven dyeing with acid dyes on nylon? How does pH control affect reproducibility? What makes a trichromatic combination reliable? Nylon dyeing rewards precision. Acid dyes bond well with polyamide fibers, but shade consistency depends on how closely strike rate, pH, and trichromatic combinations are controlled together. A small mismatch in any one variable can shift a shade off standard, even when the recipe looks correct on paper. This article breaks down the practical factors that keep acid dye combinations compatible on nylon. Understanding Strike Rate Strike rate describes how quickly a dye moves from the bath onto the fiber. On nylon, this speed depends on dye structure, temperature ramp, and the number of available dye sites on the substrate. A dye with a fast strike rate can produce uneven color if it exhausts before the bath fully penetrates the goods, particularly on tightly constructed knits or dense yarns. Factors Influencing Strike Rate Three variables have the greatest effect on how fast a given acid dye takes up on nylon: Molecular size and structure: smaller, more mobile molecules tend to migrate and level more readily, while larger or more linear structures strike faster but migrate less once fixed. Electrolyte concentration: higher salt levels in the bath slow strike by increasing ionic competition at the fiber surface, which can help leveling but may reduce total exhaustion if not balanced correctly. Temperature ramp speed: a ramp that heats too quickly gives the dye little time to migrate before fixation, raising the risk of streaks or tailing on the goods. Matching Strike Rates in a Combination When combining dyes for a shade, each component should have a comparable strike rate. If one dye in a mix strikes noticeably faster than the others, it dominates the early stages of dyeing and shifts the shade as the bath progresses. This is one of the most common causes of reproducibility problems in nylon dyehouses, especially when recipes are adjusted without checking how the new combination behaves as a system rather than as individual dyes. The Role of pH in Dye Uptake Acid dyes require an acidic bath to bond effectively with the amine groups on nylon fiber. pH does more than set the chemical environment; it also governs how fast dye uptake occurs and how much correction is possible once dyeing has started. pH Ranges by Dye Class Different acid dye classes are formulated to perform within specific pH windows. Working outside that window changes uptake speed and can affect fastness properties. Dye Class Typical pH Range Uptake Behavior Leveling acid dyes pH 5 to 6 Slower strike, good migration, easier to correct Milling acid dyes pH 4.5 to 5.5 Moderate strike, less forgiving on unlevel dyeing Metal complex acid dyes pH 4 to 5 Faster strike, stronger fastness, tighter process control needed These ranges are starting references. Actual performance depends on the specific dye grade, liquor ratio, and machine type, so lab confirmation on the intended substrate remains necessary before scaling to bulk. Controlling pH During Dyeing Holding pH steady throughout the cycle matters as much as setting the correct starting point. A pH that drifts upward during dyeing slows uptake and can leave the shade pale or uneven, while a sharp early drop can cause the dye to strike too fast for proper migration. Buffering systems and controlled acid addition keep the bath within range from start to finish. Leveling agents and buffering auxiliaries formulated for pH and strike control help stabilize uptake speed across different fabric constructions and machine conditions, particularly on constructions prone to rapid initial strike. Trichromatic Selection Principles Trichromatic dyeing uses a yellow, red, and blue dye to build a wide range of shades from a small working palette. Compatibility across these three dyes determines how predictable the resulting shades will be, both in the lab and in bulk. Choosing Compatible Yellow, Red, Blue A workable trichromatic set should share similar strike rates, similar pH sensitivity, and comparable migration behavior. Mismatched components can produce shade drift between lab dips and production batches, even when the total dye concentration is correct. The Skyacido Acid Dyes, formulated specifically for polyamide dyeing, offers a wide shade gamut with strong inter-shade combinability, which supports matching yellow, red, and blue components as a coordinated set rather than selecting each color independently based on shade alone. The table below outlines what to check across each primary when building a trichromatic set: Component Strike Rate Check pH Sensitivity Migration Behavior Yellow Compare exhaustion curve against red and blue Note shift point where uptake accelerates Confirm redistribution at hold temperature Red Compare exhaustion curve against yellow and blue Note shift point where uptake accelerates Confirm redistribution at hold temperature Blue Compare exhaustion curve against yellow and red Note shift point where uptake accelerates Confirm redistribution at hold temperature Running this comparison during lab dip development, rather than after a bulk batch shows shade drift, catches mismatches while they are still inexpensive to correct. Typical Trichromatic Acid Dye Combinations for Nylon In practical nylon dyeing, trichromatic combinations are usually selected according to shade depth, buildup requirement, and compatibility between dyes. Different combinations may be required for light shades and deep shades to maintain balanced exhaustion, migration, and shade reproducibility. Light Shade Trichromatic Combination For light and medium shades, dyes with good migration performance and moderate strike behavior are preferred to achieve excellent leveling and shade correction ability. A typical light shade combination may include: Trichromatic Position Example Acid Dye Yellow Skyacido Yellow 199 Red Skyacido Red 337 Blue Skyacido Blue 324 This combination provides good compatibility and is

Explore More »
2. Low-temperature soaping leaves clearer wash liquor and less staining on adjacent white cotton strips.

Reactive Dye Soaping Guide: Better Wash Fastness, Less Back-Staining

Table of Contents What Is Reactive Dye Soaping Role in the Wash-Off Stage Why Unfixed and Hydrolyzed Dye Must Be Removed How Soaping Affects Wash Fastness Removing Hydrolyzed Dye from the Fiber Surface Connection Between Soaping and Fastness Ratings What Causes Back-Staining? Common Sources of Back-Staining Fabrics and Blends Most at Risk Key Process Parameters for Effective Soaping Temperature and Time Liquor Ratio Water Hardness and Sequestering Agents Choosing the Right Soaping Agents Anionic and Nonionic Soaping Agents Matching Agents to Fiber and Shade Depth Low-Temperature Soaping Agent Option: Sylic D2705 Key Benefits Recommended Application Performance Comparison Soaping Process Methods Cold Wash and Hot Wash Sequence One-Bath vs Multi-Step Soaping Role of Fixing Agents After Soaping Best Practices for Consistent Wash Fastness Results FAQs How long should reactive dye soaping take? Can back-staining be fixed after it happens? Does hard water affect soaping performance? Is a separate fixing agent always necessary after soaping? Reactive dye soaping is often treated as a quick step at the end of the dyeing cycle, but it has a direct effect on wash fastness and back-staining outcomes. Getting temperature, time, and agent selection right prevents costly rejects and repeat orders that eat into margins. What Is Reactive Dye Soaping Role in the Wash-Off Stage Soaping takes place after fixation, once the reactive dye has bonded to the fiber under alkaline conditions. Fabric is washed at or near boiling temperature with a detergent or specialty soaping agent to strip away everything that never formed a permanent bond with the fiber. Skipping or shortening this step leaves wash-off incomplete, and the fabric carries a hidden fastness risk that will not surface until later testing or, worse, after it reaches the customer. Why Unfixed and Hydrolyzed Dye Must Be Removed A portion of reactive dye always hydrolyzes in the dyebath instead of reacting with the fiber. Hydrolyzed dye sits loosely on the fabric surface, held only by weak physical attraction rather than a covalent bond. Left in place, it rubs off during handling, bleeds during laundering, and transfers onto lighter fabrics in the same wash load. Soaping is the step designed specifically to remove this residue before it becomes a fastness problem. How Soaping Affects Wash Fastness The quality of soaping determines much of what shows up later in fastness testing. A batch that looks correct on the shade card can still fail to wash or rub fastness if this step was rushed. Removing Hydrolyzed Dye from the Fiber Surface Effective soaping keeps loosened dye suspended in the wash liquor instead of letting it settle back onto the fabric. How completely this happens depends on agitation, liquor ratio, and the dispersing strength of the detergent or soaping agent used. Connection Between Soaping and Fastness Ratings Wash and rub fastness ratings, most commonly evaluated using AATCC colorfastness test methods, largely reflect how much unfixed dye remains after wash-off. A fabric can pass an initial shade check on the lab dip and still fail fastness testing on the bulk batch if soaping ran too briefly or at too low a temperature. What Causes Back-Staining? Common Sources of Back-Staining Back-staining happens when dye that has washed off the dyed fabric redeposits onto undyed or lighter areas in the same bath. The most common causes include: Overloaded soaping baths carrying more hydrolyzed dye than the liquor can hold Insufficient rinsing between soaping and finishing steps Soaping agents with weak dispersing power, which allow free dye particles to settle back onto the fabric Uneven liquor circulation, which creates localized zones of high dye concentration Fabrics and Blends Most at Risk Deep and dark shades generate the highest load of hydrolyzed dye and are the most frequent source of back-staining complaints. Blended fabrics, and any load that mixes dyed and undyed components, are particularly vulnerable, since redeposited dye is far more visible on the lighter portion of the fabric. Key Process Parameters for Effective Soaping Most causes of poor fastness and back-staining trace back to how tightly these three parameters are controlled. Temperature and Time Soaping typically runs at or close to boiling point for five to fifteen minutes, though the ideal combination depends on shade depth and fabric construction. Running the bath too cool slows dye removal, and cutting the time short leaves hydrolyzed dye behind even at the correct temperature. Shade depth Soaping temperature Typical time Light to medium 90 to 95°C 5 to 8 minutes Deep and dark Near boiling (98 to 100°C) 10 to 15 minutes Turquoise and problem shades Near boiling, multi-bath 15 minutes or more per bath This near-boiling range applies to conventional soaping agents. Low-temperature soaping agents are formulated to work effectively at 60 to 80°C instead, cutting energy use without giving up fastness performance (see the Sylic D2705 section below).  Liquor Ratio A tighter liquor ratio concentrates hydrolyzed dye in a smaller volume of water, which increases the risk of redeposition before it can be flushed out. Mills running jet or overflow machines at lower liquor ratios should compensate with stronger dispersing agents or an added rinse cycle. Water Hardness and Sequestering Agents Calcium, magnesium, and iron in the water supply interfere with soaping agent performance and can leave a hazy or uneven finish. A sequestering agent, such as Sylic P1501B, an anionic chelating dispersant with a pH of 2.5 to 4.0 in a 1% solution, binds these ions before soaping begins and lets the soaping agent perform as intended. Choosing the Right Soaping Agents Anionic and Nonionic Soaping Agents Anionic soaping agents are widely used for their strong dispersing action, while nonionic types perform better in hard water and at lower temperatures. Both types are available within a dyeing auxiliary range formulated for stability in alkaline baths and low-foam performance in jet machines. Matching Agents to Fiber and Shade Depth Cotton and other cellulosic fibers generally respond well to anionic soaping agents. Blends containing synthetic fibers may need a nonionic option instead, to avoid staining the more sensitive synthetic component. Deeper shades typically call

Explore More »

Contact Us for Textile Auxiliaries and Dyes

Contact Skychem Group for more chemical solutions, If you have questions or need more information, please contact us.
We will respond within 24 hours

Get a project quote

Please tell us the requirements, the country and the application.

Scroll to Top
Email WhatsApp

Contact Us for Textile Auxiliaries and Dyes

Contact Skychem Group for more chemical solutions, If you have questions or need more information, please contact us.
We will respond within 24 hours