...

Contact Skychem Group for more chemical solutions, If you have questions or need more information, please contact us.
Respond within 24 hours

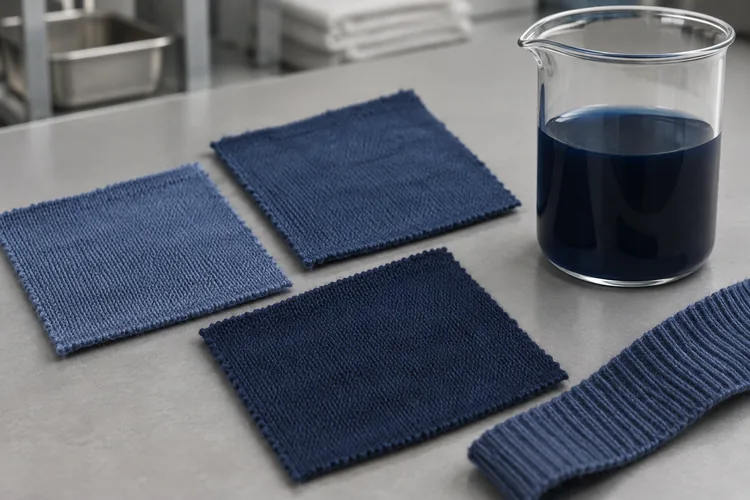
How to Dye Cationic Fabric: Process, Dyes, and Tips

Dyeing cationic fabrics correctly is essential for bright, clean shades and stable fastness. These substrates are engineered to dye differently than conventional polyester, so dye selection and process control matter more. This guide clarifies key terms, explains why cationic fabrics need cationic dyes, and provides a practical exhaust dyeing workflow with troubleshooting tips.

What Is Cationic Fabric?

In textiles, “cationic” can refer to a chemical property or to a fabric type. Mixing these meanings is a common source of confusion.

Cationic vs cationic fabric

  • Cationic (general term): describes a positively charged species in chemistry. In dyeing, cationic dyes (basic dyes) are positively charged dyes.
  • Cationic fabric (textile usage): most commonly refers to fabric containing cationic dyeable polyester (CDP), sometimes called modified polyester, or blends that include CDP.

This article focuses primarily on CDP or CDP blends. Always confirm the fiber content before selecting a dye system.
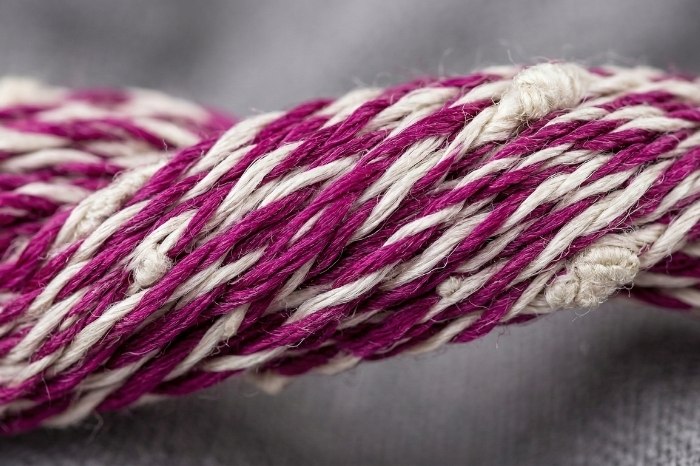
How to Dye Cationic Fabric?

Definition

Cationic dyeable polyester (CDP) is polyester modified during polymer production to introduce anionic dye sites (commonly sulfonate groups). These sites have strong affinity for cationic dyes, enabling brighter shades and clear tone separation when CDP is combined with regular polyester.

Typical benefits include:

  • High shade brilliance and clean tone
  • Clear heather or two tone effects in CDP plus regular PET constructions
  • Good bulk reproducibility when pH, dosing, and heating rate are controlled
  • Strong wash performance when proper afterwashing is used

CDP fabrics are common in sportswear, uniforms, home textiles, and fashion for visual texture and color clarity.

Which Dyes Are Used on Cationic Fabric?

For CDP and CDP blends, the key dye class is:

  • Cationic dyes (basic dyes): the primary dye class for acrylic and for CDP systems designed for cationic dyeing

If the fabric is a blend of CDP and regular PET, the dye plan depends on the desired effect:

  • Solid appearance (single shade across the fabric) may require coordinated dyeing strategies depending on construction.
  • Heather or two tone effects often use cationic dyes for the CDP component and disperse dyes for the regular PET component in controlled sequences.

Which Dyes Are Used on Cationic Fabric?

For CDP and CDP blends, the key dye class is:

  • Cationic dyes (basic dyes): the primary dye class for acrylic and for CDP systems designed for cationic dyeing

If the fabric is a blend of CDP and regular PET, the dye plan depends on the desired effect:

  • Solid appearance (single shade across the fabric) may require coordinated dyeing strategies depending on construction.
  • Heather or two tone effects often use cationic dyes for the CDP component and disperse dyes for the regular PET component in controlled sequences.

Comparison With Conventional Polyester Fabric

Feature Cationic Fabric (CDP or CDP blends) Conventional Polyester (PET)
Main dye class Cationic dyes Disperse dyes
Typical visual effect Bright shades, heather or two tone potential Solid shades; heather requires different constructions
Process sensitivity Higher (pH, dosing, ramp rate) Moderate
Common risk Rapid strike leading to unlevelness Poor dispersion or inadequate reduction clearing

Choosing Dyes for Cationic Fabric

Picking the perfect color of dye is what makes or breaks your project. The Skyzon® Cationic Dyes have been developed to ensure high-level professional results with superior fastness and levelness.

Key features include:

  • Top-level Second-to-none Levelness: Evenness of color in the yarn.
  • Excellent fastness properties: washing, rubbing, and light.
  • Steady Performance: Good applicability to batch and continuous dyeing.
  • High-Performance Formula: Developed for acrylic and cationic fibers.

Benefits for manufacturers:

  • Lower dyeing costs by re-dyeing reduction due to the equal uptake.
  • Long-lasting, vibrant colors.
  • Flexibility of use at several dyeing stages and various production levels.

It can be used in a variety of different textiles such as sweaters, blankets, and even carpets.

Step-by-Step Guide to Dyeing Cationic Fabric (Exhaust Method)

Exact parameters depend on your dye range, machine type, liquor ratio, shade depth, and fabric history. Use this workflow as a control framework and validate with lab dips and supplier technical data.

1) Preparation and scouring

Goal: remove oils, spin finish, and contaminants that cause unlevelness.

  • Pre scour as needed using a suitable detergent system for polyester fabrics
  • Rinse thoroughly until foam and oily residues are removed
  • Keep water quality consistent, especially hardness and trace metals

2) Set bath conditions

  • Start with strong circulation
  • Adjust to the target mildly acidic pH commonly used for cationic dyeing (often around pH 4.5 to 5.5 depending on system)
  • Pre dissolve dyes and filter if required to reduce specks

3) Add auxiliaries for control

Depending on your process package, add wetting and leveling auxiliaries designed for CDP and cationic dyes. The goal is stable migration and controlled strike, not maximum speed.

4) Dye addition and dosing discipline

  • Add dyes gradually with strong circulation
  • Avoid local concentration shocks from dumping dyes into stagnant zones
  • For deep shades, prioritize stability and levelness over fast strike

5) Temperature ramp and hold

  • Raise temperature steadily following the dye supplier recommendation and your validated lab profile
  • Hold long enough to reach target exhaustion and fixation behavior for the shade depth
  • Avoid rapid heating, which can trigger uneven uptake and streaking

6) Rinse and afterwash

  • Cool down in a controlled manner
  • Drain and rinse thoroughly
  • Afterwash according to fastness targets and dye supplier guidance to remove unfixed or surface dye
  • Neutralize to the finishing compatible pH range and avoid over correction into strong alkalinity

7) Finishing and drying

  • Apply compatible softeners or functional finishes only after shade stability is confirmed
  • Dry under controlled temperature to reduce shade shift or uneven appearance

Troubleshooting Common Problems

Issue Likely cause Practical fix
Streaks or unlevel dyeing Inadequate scouring, weak circulation, rapid strike, fast ramp rate Improve pre treatment, increase circulation, slow dosing, control heating rate
Shade too light Wrong dye class, pH out of range, insufficient time or temperature Confirm fiber type and dye system, correct pH, extend hold time as validated
Poor wash fastness Incomplete afterwash, surface dye remaining Strengthen rinse and afterwash, verify sequence and bath stability
Specks or dirty tone Undissolved dye, filtration issues, unstable bath Pre dissolve and filter dyes, improve bath stability, control water quality
Lot to lot variation Substrate variation, water quality variation, inconsistent dosing order Standardize incoming checks, lock dosing order, record pH and temperature curves

Production Tips for Better Repeatability

  • Standardize dosing order and dosing time
  • Track the pH curve at multiple points, not just start and finish
  • Lock the temperature ramp rate and hold time by shade depth
  • Stabilize water quality, especially hardness and metal ions
  • Validate lab dips using the same liquor ratio, dosing sequence, and ramp profile as production
  • Document every batch curve to identify drift early

Conclusion

When it comes to dyeing action, there is nothing that’ll get the job done quite like accuracy and well-made products in tandem. Employing cutting-edge solutions such as Skyzon® Cationic Dyes results in bright, permanent, and overall color-deep fabric. They are the flattest, fastest, and most consistent surfaces for dyeing.

Once you have learned what cationic fabric is and implemented the right dyeing methods, you can start reaping its benefits; your textiles become durable, colorful, professional-looking masterpieces!


Recommended reading:

  1. 9 Different Types of Dyes Used in Textile Industry
  2. Functions and Types of Textile Auxiliary Chemicals Explained
  3. The Differences Between Disperse and Reactive Dyes

Sandy

With years of experience in chemical dyes and textile auxiliaries, I’m dedicated to sharing insights into the latest technologies, sustainable innovations, and market trends.

Recent Articles

Chemical sample vials beside woven cotton test swatches.

APEO-Free Nonionic Wetting Agents for Textile Pretreatment

Table of Contents What Does APEO-Free Mean? APEO-Free vs. NPEO-Free Nonionic Alternatives to APEO Performance After APEO Replacement Wetting Speed and Fabric Penetration Oil Removal and Redeposition Foam Control and Rinsability Cloud Point and Operating Temperature Pretreatment Bath Compatibility Alkali Concentration and Stability Peroxide and Bleach Stabilizers Desizing and Scouring Enzymes Hard Water and Other Auxiliaries Selecting and Testing Alternatives Match the Fabric and Equipment Compare Active Content and Working Dosage Benchmark Against the Existing Product Verify Absorbency and Dyeing Uniformity Compliance and Supplier Evidence APEO-Free Claims and Detection Limits REACH: Formulations vs. Textile Articles ZDHC MRSL vs. Brand RSLs Supplier Declarations and Test Reports FAQs Is APEO-Free the Same as NPEO-Free? Can APEO-Free Alternatives Be Used at the Same Dosage? Does APEO-Free Mean ZDHC MRSL Conformance? APEO-free nonionic wetting agents help pretreatment liquors spread across fabric and penetrate its structure, supporting uniform desizing, scouring, and bleaching. Selecting a replacement for an APEO-based auxiliary requires more than an APEO-free declaration: wetting speed, foam, cleaning performance, and bath compatibility must meet the process requirements. For mills and textile chemical buyers, the key is to verify performance at a practical working dosage and confirm compliance with product-specific evidence. What Does APEO-Free Mean? APEO-Free vs. NPEO-Free Alkylphenol ethoxylates, or APEOs, are a family of nonionic surfactants that includes nonylphenol ethoxylates (NPEOs) and octylphenol ethoxylates (OPEOs). Commercial and regulatory documents may use either “NPE” or “NPEO” for nonylphenol ethoxylates. An NPEO-free declaration covers only part of this family. It does not establish that OPEOs or every substance covered by an APEO specification are absent. Likewise, “nonionic” describes ionic character, not restricted-substance content. APEOs themselves are nonionic. An APEO-free claim needs a defined substance scope and acceptance limit, as discussed in the compliance section below. Nonionic Alternatives to APEO Fatty alcohol ethoxylates and other alcohol alkoxylates are common alternatives. Their alcohol structure, ethoxylation level, and formulation influence wetting, emulsification, solubility, and foam. AEO-9 is a fatty alcohol ethoxylate with an average of about nine ethylene oxide units. It supports oil emulsification and cleaning in textile auxiliary formulations. Emulsifying oil and rapidly penetrating dense fabric are different functions, so assess wetting speed and cleaning performance separately when selecting a pretreatment formulation. APEO-free chemistry alone does not establish ready biodegradability or overall product safety. Performance After APEO Replacement Wetting Speed and Fabric Penetration Surface wetting is only the first step. The liquor must also reach the interior of yarns and fabric so that pretreatment chemicals can act evenly. Dense woven fabrics, compact knits, and yarn packages can reveal penetration problems that are not apparent in a simple solution test. Evaluate representative material at the intended concentration and temperature. On continuous lines, compare performance within the available contact time. In batch equipment, check wet-out across the load, including areas where trapped air or restricted circulation may delay penetration. Oil Removal and Redeposition Rapid wetting does not prove effective scouring. Cotton waxes, knitting oils, and other hydrophobic impurities may remain even when the treatment liquor spreads easily. The recipe must release these materials, keep them emulsified or dispersed, and remove them during washing. Check for oily spots and deposits after cooling and rinsing, when unstable emulsions may allow impurities to redeposit. If wetting is satisfactory but cleaning is poor, investigate detergency, temperature, treatment time, and washing efficiency before increasing the wetting-agent dose. Foam Control and Rinsability APEO-free and nonionic are not synonyms for low-foaming. Foam behavior depends on the formulation, working concentration, agitation, temperature, and impurities entering the bath. Evaluate low-foam wetting performance throughout filling, treatment, cooling, and rinsing. A quiet bath at the scouring temperature may still foam during dilution or circulation at a lower temperature. Sylic P1412 nonionic low-foaming wetting agent is based on polyoxyethylene compounds and combines wetting and emulsification for dyeing and finishing applications where foam control matters. Its reference dosage of 0.5–3.0 g/L provides a starting range for application trials, not a fixed pretreatment recipe. For APEO-free pretreatment, confirm product-specific APEO evidence and test foam, penetration, and compatibility at the intended alkali concentration and temperature. Assess rinsability alongside foam. A low-foaming product still needs to wash out sufficiently for the next processing stage. Cloud Point and Operating Temperature Many ethoxylated nonionic surfactants become cloudy when heating changes their hydration and water solubility. The measured cloud point depends on concentration, solution composition, and test conditions. A water-based data-sheet value may not represent a bath containing caustic soda, salts, and other auxiliaries. Electrolytes can shift clouding behavior, so test the complete recipe through its actual temperature cycle. Cloudiness alone is not a pass-or-fail criterion. Some formulations function effectively near or above their measured cloud point. The relevant checks are uniform treatment, adequate wetting, and the absence of troublesome separation or deposits. Pretreatment Bath Compatibility Alkali Concentration and Stability Specify alkali resistance in terms of sodium hydroxide concentration, temperature, and exposure time. Neither a broad working-pH range nor the measured pH of a dilute product solution establishes stability in concentrated caustic liquor. Check both physical stability and wetting performance. A bath may remain dispersed while penetration becomes too slow for the process. Cold pad-batch treatment, hot scouring, and mercerizing require separate assessments. Approval for alkaline scouring should not be extended to mercerizing without testing at the intended caustic concentration. Peroxide and Bleach Stabilizers In combined scouring and bleaching, evaluate the candidate with the actual peroxide, alkali, stabilizer, and sequestering system. Monitor bath appearance, foam, peroxide behavior, whiteness, and fabric condition. Unexpected peroxide loss or uneven bleaching requires investigation of the whole recipe, including water quality and metal contamination. The wetting agent distributes the liquor and supports impurity removal. It does not replace peroxide stabilization or metal-ion control. Desizing and Scouring Enzymes Test compatibility with the specific enzyme preparation and complete recipe under the enzyme supplier’s recommended conditions. Chelants, preservatives, solvents, and other ingredients may affect enzyme activity even when the main surfactant is compatible. For amylase desizing, compare residual starch size after identical washing. For enzymatic scouring, compare cleaning and absorbency. Hard Water and Other Auxiliaries

Explore More »
Cotton knit swatches compared for dyeing uniformity.

Multifunctional Scouring Agents for One-Bath Textile Pretreatment

Table of Contents What Are Multifunctional Scouring Agents? Which Functions Can They Combine? A Cotton-Knit and Yarn Application What May Still Require Separate Treatment? Bleaching and Alkali Adjustment Desizing and Difficult Contamination Washing and Post-Bleach Cleanup When to Use a Combined Formulation How to Select and Validate the Recipe Map Functions and Operating Conditions Assess Water and Metal Contamination Test Bath and Machine Compatibility Compare Preparation and Dyeing Results Compare Total Processing Costs FAQ Can a Multifunctional Scouring Agent Replace Every Pretreatment Chemical? What Dosage Should Be Used? Does One-Bath Pretreatment Include Dyeing? Multifunctional scouring agents simplify cotton pretreatment by combining several auxiliary functions in one formulation. In a compatible one-bath scouring and bleaching process, they can reduce separate chemical additions while providing the cleaning and bleaching support needed before dyeing. The main selection question is whether one product supplies the required balance at its working dose. Fabric contamination, water quality, machinery, and the intended finish determine which chemicals it can replace and which remain necessary. What Are Multifunctional Scouring Agents? Conventional scouring agents for cotton often combine wetting, emulsification, and dispersion. Multifunctional formulations extend that combination to additional requirements, such as peroxide stabilization or alkali supply. Terms such as “3-in-1” and “all-in-one” do not define a standard composition. One-bath scouring and bleaching combines impurity removal and bleaching in the same liquor. The process can still require staged additions, temperature changes, and controlled holding periods. Dyeing remains a separate operation unless a validated process specifically combines preparation and coloration. Replacing several auxiliaries simplifies the recipe. Combining previously separate treatment baths changes the process and may also reduce filling, draining, and heating operations. These are distinct sources of potential savings. Which Functions Can They Combine? Check the technical data sheet and application guidance to establish which functions the selected formulation supplies. Function Purpose Main verification Wetting and penetration Help liquor enter the textile evenly Performance at the intended alkali level, temperature, and circulation rate Detergency and emulsification Help release and suspend waxes, oils, and processing contamination Removal of the actual impurity load Dispersion Limit redeposition of removed material Cleanliness after washing and absence of deposits Metal-ion control Bind specified ions and limit associated interference Capacity for the relevant ions under working conditions Peroxide stabilization Limit unwanted peroxide decomposition Peroxide behavior, whiteness, and fabric condition Alkalinity Supply some or all of the required alkali Working pH, available alkalinity, and any additional alkali requirement Fast wetting does not establish complete oil removal. Likewise, metal-ion control and peroxide stabilization need separate assessment even when one formulation provides both. A Cotton-Knit and Yarn Application Sylic P1112 (F600) multifunctional pretreatment agent combines alkali, scouring, and stabilizing functions for cotton-knit and yarn pretreatment. It suits processes that need these functions together while retaining separate control of peroxide addition. The following conditions provide a starting point for application trials: Parameter Cotton-knit and yarn trial range Sylic P1112 (F600) 1–3 g/L Hydrogen peroxide, 30% solution 2–6 g/L Additional sodium hydroxide or sodium carbonate 0–1 g/L, as required Liquor ratio 1:4–1:8 Treatment temperature 95–100°C Holding time 50–60 minutes These application ranges are specific to the product and process. Follow the product-specific addition sequence and validate these conditions on the intended textile and equipment. The fixed combination reduces separate auxiliary additions but offers less independent adjustment of alkali, scouring, and stabilization than separately dosed products. What May Still Require Separate Treatment? Bleaching and Alkali Adjustment A peroxide stabilizer does not supply the bleaching chemical. Hydrogen peroxide remains a separate addition unless the formulation explicitly incorporates a suitable bleaching system. Separately dosed hydrogen peroxide bleaching stabilizers may still be needed when built-in stabilization is insufficient for the complete bath. Assess peroxide behavior together with whiteness and fabric strength. An alkaline multifunctional product can reduce caustic soda additions while maintaining an alkaline bath. Measure working pH and alkalinity rather than using the pH of a diluted product sample to predict operating conditions. Keep concentration calculations consistent: 4 g/L of a 30% hydrogen peroxide solution supplies 1.2 g/L of active hydrogen peroxide. This is a calculation example, not a recommended dose. Desizing and Difficult Contamination Sized woven fabrics need treatment matched to the sizing system. Starch, polyvinyl alcohol, and mixed sizes may require different removal conditions. Amylase can support starch desizing, but compatibility with the proposed bath must be established. Other needs may include: Additional emulsifying or degreasing support for heavy knitting oil or spin finishes. Adequate penetration and uniform liquor flow through dense fabrics or yarn packages. A compatible lubricant for crease-sensitive goods. Conditions that preserve elasticity and dimensional stability in cotton/elastane blends. A separate supporting auxiliary is often more practical when only one function needs strengthening. Increasing the multifunctional product raises all its components together. Washing and Post-Bleach Cleanup Washing must remove released impurities and residual chemicals. Check water exchange, circulation, and carryover before reducing the washing sequence. Before oxidation-sensitive dyeing, test residual peroxide and remove it as required. Catalase decomposes hydrogen peroxide into water and oxygen within the selected enzyme’s operating conditions. Verify the result by testing. Check fabric pH after washing and any required neutralization. Peroxide removal and pH adjustment address different residues. When to Use a Combined Formulation Fixed combinations are easiest to manage when incoming material, contamination, water quality, and production conditions remain reasonably consistent. Match the preparation target to the end use. Towels require consistent absorbency; pale shades and white goods require close control of the bleached base. Cotton/elastane goods also need checks on stretch recovery. Separate or hybrid recipes provide more flexibility when requirements change independently. Harder water may require more metal control without additional detergent. A heavier oil load may require more emulsification without more alkali. In these cases, retain a multifunctional base product and adjust the specific supporting auxiliary. How to Select and Validate the Recipe Map Functions and Operating Conditions Identify the purpose of each ingredient in the existing recipe. Establish which functions the replacement supplies at its proposed dose, then confirm: Fiber composition, construction, and contamination. Machinery, liquor ratio or wet

Explore More »

Azo Dyes in Textiles: Restrictions, Testing, and Compliance

Table of Contents 1. Azo Dye Chemistry and Textile Uses What Is an Azo Dye? Where Are Azo Dyes Used? 2. Restricted Aromatic Amines How Azo Dyes Release Amines Which Amines Are Restricted? What Does “Azo-Free” Mean? 3. Compliance Requirements EU REACH Restrictions Destination-Market Rules Buyer RSLs and Chemical Standards 4. Azo Dye Testing Textile Test Methods Reading Test Reports 5. Buyer and Supplier Requirements Documents Buyers Should Request Selecting Suitable Dyes Managing Noncompliance FAQ Are All Azo Dyes Banned in Textiles? Does “Azo-Free” Mean REACH Compliant? Does ZDHC MRSL Conformance Replace Finished-Textile Testing? A dye that meets shade and fastness targets can still fail a customer’s chemical specification. For textile manufacturers and buyers, selecting azo dyes therefore requires both technical evaluation and reliable compliance evidence. Azo dyes are not universally banned. Restrictions target certain colorants and the aromatic amines they can release. Sound purchasing decisions depend on distinguishing dye chemistry, chemical-input controls, and finished-textile compliance. 1. Azo Dye Chemistry and Textile Uses What Is an Azo Dye? An azo dye contains one or more azo linkages, written as –N=N–, within its molecular structure. These linkages form part of a conjugated system that absorbs visible light. The surrounding molecular structure influences the resulting color and other properties. “Azo” describes chemical structure. “Reactive,” “direct,” “acid,” and “disperse” describe application classes, so a dye can belong to both categories. For example, azo direct dyes combine azo chemistry with the application characteristics of direct dyes. Reactive, acid, and disperse dye ranges can also include azo structures. Application class alone does not establish which restricted amines an individual product could release. Where Are Azo Dyes Used? For cotton and viscose, select reactive dyes according to the fixation process. The Skyzol KE/TE series uses monochlorotriazine reactive groups and is suited to dyeing at 80°C, including applications on viscose, towels, and mercerized cotton. It is not suitable for cold pad-batch processing. This process fit does not establish the azo structure or restricted-amine status of an individual shade; confirm those separately through product-specific information and test evidence. Disperse dyes are widely used on polyester, while acid dyes are commonly used on wool and nylon. 2. Restricted Aromatic Amines How Azo Dyes Release Amines Under reducing conditions, azo linkages can split through reductive cleavage. The resulting compounds depend on the colorant’s molecular structure. Certain azo dyes can release restricted aromatic amines. Laboratory tests use controlled conditions to assess this behavior. They do not simply measure dye washing off fabric, and their results are not direct predictions of exposure during ordinary wear. Two potential sources of amines should be distinguished: Amines released by cleavage: Compounds formed when the colorant breaks down under the specified test conditions. Free amine impurities: Residual compounds already present in a formulation or material. An unsuitable molecular structure and an impurity may require different corrective actions. Neither can be identified from shade alone. Which Amines Are Restricted? The REACH Appendix 8 list of aromatic amines contains 22 entries. Examples include benzidine, CAS 92-87-5; o-toluidine, CAS 95-53-4; and 4-aminoazobenzene, CAS 60-09-3. Compare CAS numbers as well as names when reviewing specifications. Different chemical names may refer to the same substance. Buyer lists may cover additional amines and related salts. A test panel covering the EU list may therefore be insufficient for a particular customer. What Does “Azo-Free” Mean? “Azo-free” is often used loosely in purchasing specifications. It may mean that no azo-structured colorants are permitted, or it may mean that a material must pass a restricted aromatic amine test. Define the term in writing before approval, specifying substances, test methods, acceptance limits, reporting limits, and components covered. 3. Compliance Requirements EU REACH Restrictions REACH Annex XVII Entry 43 prohibits the use of azo dyes that can release the listed aromatic amines above 30 mg/kg under specified testing conditions in textile and leather articles within scope, or their dyed parts. Nonconforming articles must not be placed on the market. The relevant articles are those that may come into direct and prolonged contact with skin or the oral cavity, including clothing, bedding, towels, and certain footwear and accessories. The threshold concerns individual listed amines released during testing. It is not a maximum concentration for all azo dyes in fabric or dye powder. Entry 43 also contains a separate restriction on colorants identified in Appendix 9. Passing an aromatic amine test alone should therefore not be presented as proof that every provision has been met. Destination-Market Rules Identify where the finished goods will be sold before finalizing the chemical specification. The manufacturing country does not determine all requirements for an export order. Confirm: Destination markets and product category. Intended use and relevant contact with skin or the mouth. Applicable legal requirements. The customer’s current restricted substances list. Testing and documentation requirements for individual components. A report prepared for a previous order may be useful, but its substance coverage, methods, and limits must match the new requirements. Buyer RSLs and Chemical Standards Legal restrictions, buyer specifications, and voluntary certification programs assess different aspects of the supply chain. Requirement or program What it addresses Key purchasing check REACH Entry 43 Restricted azo colorants and released amines in articles within scope Confirm product scope and applicable restrictions AFIRM RSL Restricted substances in finished-product component materials The 2026 list specifies 20 ppm each for listed azo-amines and arylamine salts, with a separate 5 ppm reporting limit ZDHC MRSL Restricted substances in manufacturing chemical formulations Verify conformance evidence for the exact chemical product OEKO-TEX STANDARD 100 Harmful-substance testing and certification of textiles Check certificate validity, article scope, and product class OEKO-TEX ECO PASSPORT Assessment and certification of chemicals, colorants, and auxiliaries Confirm that the supplied chemical product is covered A buyer may adopt an industry RSL or issue a separate specification. Confirm the version governing the order. An RSL addresses substances in finished materials or products. An MRSL addresses manufacturing chemical inputs. Conformant inputs help control risk, but they do not automatically establish finished-fabric compliance. When selecting ZDHC-conformant textile chemicals, match the product

Explore More »
Cotton lab dips compared during reactive dye selection.

Reactive Garment Dyeing: Process, Dyes, and Defect Control

Table of Contents 1. Selecting Reactive Dyes Fiber and Component Compatibility Dye Compatibility and Process Suitability Fastness and Processing Cost 2. Selecting Dyeing Auxiliaries Pretreatment Auxiliaries Dyeing Auxiliaries and Process Chemicals Wash-Off and Finishing Auxiliaries 3. The Reactive Garment Dyeing Process Step 1: Inspect and Prepare the Garments Step 2: Prepare and Add the Dyes Step 3: Control Exhaustion and Fixation Step 4: Rinse, Wash Off, and Finish 4. Improving Shade Reproducibility Standardize Materials and Chemical Inputs Validate Lab-to-Bulk Transfer Assess Color Under Agreed Conditions Use Batch Records to Investigate Variation 5. Controlling Common Dyeing Defects FAQ Is a fixing agent necessary after reactive garment dyeing? How can backstaining be reduced during washing-off? A cotton T-shirt can match the approved body shade and still fail inspection because the collar is darker, the seams remain pale, or crease marks appear after drying. Garment dyeing brings together fabrics, threads, trims, and multilayer areas that may respond differently to the same bath. Reactive garment dyeing colors assembled cellulosic garments through dye exhaustion and covalent fixation. Hydrolysis competes with fixation, leaving unfixed color that must be washed off. This guide covers dye selection, auxiliaries, process control, and defect prevention in industrial exhaust dyeing of cotton and other suitable cellulosic garments, including considerations for blends. 1. Selecting Reactive Dyes Fiber and Component Compatibility Check the complete garment specification before developing the recipe. Include body fabric, ribbing, pocketing, sewing thread, interlinings, labels, and trims. Two cotton components can develop different shade depths because of differences in yarn, construction, mercerization, or preparation. Polyester sewing thread will not develop the same shade as cotton under a conventional cotton reactive dyeing process. Cotton-covered corespun thread may provide a closer match, but its appearance still requires a sewn-garment trial. For blends, establish which components the process will color: Cotton–polyester: Reactive dyes color the cellulosic portion. Matching the polyester requires a suitable additional dye system and compatible processing conditions. Cotton–elastane: Check temperature, alkalinity, exposure time, and mechanical action against the material supplier’s recommendations. Assess stretch recovery and dimensional stability after processing. Dye Compatibility and Process Suitability Select reactive dyes for cellulosic fibers according to the target shade, machine capability, and application conditions. Compare solubility, recommended temperature, reactivity, exhaustion behavior, and wash-off performance. Combination shades require compatible exhaustion and fixation behavior. When one dye reacts much faster than the others, dosing or temperature variation can shift the shade balance. For sensitive combination shades, Skyzol RGB uses selected M-series dyes with similar substantivity and reactivity. Match the combination to the intended process and verify its response to changes in pH, electrolyte, temperature, and liquor ratio. Similar application behavior supports recipe compatibility but does not guarantee bulk shade reproducibility. Fastness and Processing Cost Define the required wash, rubbing, perspiration, and light fastness according to the garment’s end use. Strong wash fastness does not automatically establish suitability for every other exposure. For deep shades, pay particular attention to wash-off demand and wet rubbing performance. Test after the intended finishing treatment because softening and drying can influence the final result. Compare cost per kilogram of acceptable garments. Include dye consumption, auxiliaries, water, energy, processing time, and rework rather than judging a recipe by dye price alone. 2. Selecting Dyeing Auxiliaries Select auxiliaries for a defined function and check compatibility across the complete bath. Pretreatment Auxiliaries Select textile pretreatment auxiliaries according to the impurities present and the garment’s preparation history. Wetting and scouring agents support uniform absorbency; sequestering agents help manage interfering metal ions. Prepared-for-dyeing fabric can acquire sewing oils or handling contamination during garment assembly. Check the assembled garment, not just the original fabric specification. Dyeing Auxiliaries and Process Chemicals Choose dyeing auxiliaries for the machine, garment construction, and dye system. Check leveling agents for their effect on exhaustion and color yield. Address overloading or restricted movement directly; an anti-crease agent cannot correct those conditions. Electrolyte and alkali have distinct roles in conventional reactive exhaust dyeing. Electrolyte promotes exhaustion; alkali creates conditions for dye–fiber fixation. Their quantities and addition sequence must match the selected application procedure. Product category Main function Selection checks Wetting and scouring agents Improve wetting and remove impurities Absorbency, foam, rinsability, and substrate suitability Sequestering agents Manage interfering metal ions Water quality, working pH, and dye compatibility Peroxide removal agents Eliminate residual peroxide after bleaching Working conditions and measured residual peroxide Lubricants and anti-crease agents Reduce friction and crease formation Garment movement, machine conditions, and deposit risk Leveling agents and defoamers Control uneven uptake or excessive foam where needed Bath stability, dye yield, and compatibility Soaping agents Help remove unfixed dye and limit redeposition Shade depth, water quality, residual electrolyte, and fastness Softeners Develop the required hand Shade change, spotting, absorbency, and compatibility Fixing agents, where justified Improve specific fastness properties Measured benefit and effects on shade, hand, and other requirements Wash-Off and Finishing Auxiliaries Wash-off performance depends on dye substantivity, water quality, residual chemicals, temperature, and liquor exchange. Sylic D2705 soaping agent is an anionic/nonionic surfactant–polymer powder for wash-off and anti-staining treatment of reactive-dyed cotton and rayon. Its pH of 6.0–8.0 refers to a 1% aqueous product solution, not the operating bath. Check compatibility with the other auxiliaries at the intended working conditions. Set dosage, temperature, and sequence through garment trials. For a lower-temperature route, compare fastness, staining, and final shade with the established process before reducing heat input or cycle time. The required wash-off performance takes priority over potential energy savings. Check softeners for effects on shade, absorbency, and hand. Use fixing agents only for a demonstrated fastness benefit; they do not replace fixation or effective washing-off. 3. The Reactive Garment Dyeing Process Step 1: Inspect and Prepare the Garments Confirm garment weight, component lots, preparation history, and machine loading. Keep incompatible materials or preparation histories separate. A practical readiness check includes: Uniform absorbency across body fabric and components. Removal of oils, sizing where present, and other relevant impurities. Residual pH suitable for the next stage. Acceptable process-water quality. Verified peroxide removal when bleaching has been used. Consistent cotton dyeing

Explore More »

Contact Us for Textile Auxiliaries and Dyes

Contact Skychem Group for more chemical solutions, If you have questions or need more information, please contact us.
We will respond within 24 hours

Get a project quote

Tell us your project requirements, country, and intended application.

Sandy

With years of experience in chemical dyes and textile auxiliaries, I’m dedicated to sharing insights into the latest technologies, sustainable innovations, and market trends.

Recent Articles

Chemical sample vials beside woven cotton test swatches.

APEO-Free Nonionic Wetting Agents for Textile Pretreatment

Table of Contents What Does APEO-Free Mean? APEO-Free vs. NPEO-Free Nonionic Alternatives to APEO Performance After APEO Replacement Wetting Speed and Fabric Penetration Oil Removal and Redeposition Foam Control and Rinsability Cloud Point and Operating Temperature Pretreatment Bath Compatibility Alkali Concentration and Stability Peroxide and Bleach Stabilizers Desizing and Scouring Enzymes Hard Water and Other Auxiliaries Selecting and Testing Alternatives Match the Fabric and Equipment Compare Active Content and Working Dosage Benchmark Against the Existing Product Verify Absorbency and Dyeing Uniformity Compliance and Supplier Evidence APEO-Free Claims and Detection Limits REACH: Formulations vs. Textile Articles ZDHC MRSL vs. Brand RSLs Supplier Declarations and Test Reports FAQs Is APEO-Free the Same as NPEO-Free? Can APEO-Free Alternatives Be Used at the Same Dosage? Does APEO-Free Mean ZDHC MRSL Conformance? APEO-free nonionic wetting agents help pretreatment liquors spread across fabric and penetrate its structure, supporting uniform desizing, scouring, and bleaching. Selecting a replacement for an APEO-based auxiliary requires more than an APEO-free declaration: wetting speed, foam, cleaning performance, and bath compatibility must meet the process requirements. For mills and textile chemical buyers, the key is to verify performance at a practical working dosage and confirm compliance with product-specific evidence. What Does APEO-Free Mean? APEO-Free vs. NPEO-Free Alkylphenol ethoxylates, or APEOs, are a family of nonionic surfactants that includes nonylphenol ethoxylates (NPEOs) and octylphenol ethoxylates (OPEOs). Commercial and regulatory documents may use either “NPE” or “NPEO” for nonylphenol ethoxylates. An NPEO-free declaration covers only part of this family. It does not establish that OPEOs or every substance covered by an APEO specification are absent. Likewise, “nonionic” describes ionic character, not restricted-substance content. APEOs themselves are nonionic. An APEO-free claim needs a defined substance scope and acceptance limit, as discussed in the compliance section below. Nonionic Alternatives to APEO Fatty alcohol ethoxylates and other alcohol alkoxylates are common alternatives. Their alcohol structure, ethoxylation level, and formulation influence wetting, emulsification, solubility, and foam. AEO-9 is a fatty alcohol ethoxylate with an average of about nine ethylene oxide units. It supports oil emulsification and cleaning in textile auxiliary formulations. Emulsifying oil and rapidly penetrating dense fabric are different functions, so assess wetting speed and cleaning performance separately when selecting a pretreatment formulation. APEO-free chemistry alone does not establish ready biodegradability or overall product safety. Performance After APEO Replacement Wetting Speed and Fabric Penetration Surface wetting is only the first step. The liquor must also reach the interior of yarns and fabric so that pretreatment chemicals can act evenly. Dense woven fabrics, compact knits, and yarn packages can reveal penetration problems that are not apparent in a simple solution test. Evaluate representative material at the intended concentration and temperature. On continuous lines, compare performance within the available contact time. In batch equipment, check wet-out across the load, including areas where trapped air or restricted circulation may delay penetration. Oil Removal and Redeposition Rapid wetting does not prove effective scouring. Cotton waxes, knitting oils, and other hydrophobic impurities may remain even when the treatment liquor spreads easily. The recipe must release these materials, keep them emulsified or dispersed, and remove them during washing. Check for oily spots and deposits after cooling and rinsing, when unstable emulsions may allow impurities to redeposit. If wetting is satisfactory but cleaning is poor, investigate detergency, temperature, treatment time, and washing efficiency before increasing the wetting-agent dose. Foam Control and Rinsability APEO-free and nonionic are not synonyms for low-foaming. Foam behavior depends on the formulation, working concentration, agitation, temperature, and impurities entering the bath. Evaluate low-foam wetting performance throughout filling, treatment, cooling, and rinsing. A quiet bath at the scouring temperature may still foam during dilution or circulation at a lower temperature. Sylic P1412 nonionic low-foaming wetting agent is based on polyoxyethylene compounds and combines wetting and emulsification for dyeing and finishing applications where foam control matters. Its reference dosage of 0.5–3.0 g/L provides a starting range for application trials, not a fixed pretreatment recipe. For APEO-free pretreatment, confirm product-specific APEO evidence and test foam, penetration, and compatibility at the intended alkali concentration and temperature. Assess rinsability alongside foam. A low-foaming product still needs to wash out sufficiently for the next processing stage. Cloud Point and Operating Temperature Many ethoxylated nonionic surfactants become cloudy when heating changes their hydration and water solubility. The measured cloud point depends on concentration, solution composition, and test conditions. A water-based data-sheet value may not represent a bath containing caustic soda, salts, and other auxiliaries. Electrolytes can shift clouding behavior, so test the complete recipe through its actual temperature cycle. Cloudiness alone is not a pass-or-fail criterion. Some formulations function effectively near or above their measured cloud point. The relevant checks are uniform treatment, adequate wetting, and the absence of troublesome separation or deposits. Pretreatment Bath Compatibility Alkali Concentration and Stability Specify alkali resistance in terms of sodium hydroxide concentration, temperature, and exposure time. Neither a broad working-pH range nor the measured pH of a dilute product solution establishes stability in concentrated caustic liquor. Check both physical stability and wetting performance. A bath may remain dispersed while penetration becomes too slow for the process. Cold pad-batch treatment, hot scouring, and mercerizing require separate assessments. Approval for alkaline scouring should not be extended to mercerizing without testing at the intended caustic concentration. Peroxide and Bleach Stabilizers In combined scouring and bleaching, evaluate the candidate with the actual peroxide, alkali, stabilizer, and sequestering system. Monitor bath appearance, foam, peroxide behavior, whiteness, and fabric condition. Unexpected peroxide loss or uneven bleaching requires investigation of the whole recipe, including water quality and metal contamination. The wetting agent distributes the liquor and supports impurity removal. It does not replace peroxide stabilization or metal-ion control. Desizing and Scouring Enzymes Test compatibility with the specific enzyme preparation and complete recipe under the enzyme supplier’s recommended conditions. Chelants, preservatives, solvents, and other ingredients may affect enzyme activity even when the main surfactant is compatible. For amylase desizing, compare residual starch size after identical washing. For enzymatic scouring, compare cleaning and absorbency. Hard Water and Other Auxiliaries

Explore More »
Cotton knit swatches compared for dyeing uniformity.

Multifunctional Scouring Agents for One-Bath Textile Pretreatment

Table of Contents What Are Multifunctional Scouring Agents? Which Functions Can They Combine? A Cotton-Knit and Yarn Application What May Still Require Separate Treatment? Bleaching and Alkali Adjustment Desizing and Difficult Contamination Washing and Post-Bleach Cleanup When to Use a Combined Formulation How to Select and Validate the Recipe Map Functions and Operating Conditions Assess Water and Metal Contamination Test Bath and Machine Compatibility Compare Preparation and Dyeing Results Compare Total Processing Costs FAQ Can a Multifunctional Scouring Agent Replace Every Pretreatment Chemical? What Dosage Should Be Used? Does One-Bath Pretreatment Include Dyeing? Multifunctional scouring agents simplify cotton pretreatment by combining several auxiliary functions in one formulation. In a compatible one-bath scouring and bleaching process, they can reduce separate chemical additions while providing the cleaning and bleaching support needed before dyeing. The main selection question is whether one product supplies the required balance at its working dose. Fabric contamination, water quality, machinery, and the intended finish determine which chemicals it can replace and which remain necessary. What Are Multifunctional Scouring Agents? Conventional scouring agents for cotton often combine wetting, emulsification, and dispersion. Multifunctional formulations extend that combination to additional requirements, such as peroxide stabilization or alkali supply. Terms such as “3-in-1” and “all-in-one” do not define a standard composition. One-bath scouring and bleaching combines impurity removal and bleaching in the same liquor. The process can still require staged additions, temperature changes, and controlled holding periods. Dyeing remains a separate operation unless a validated process specifically combines preparation and coloration. Replacing several auxiliaries simplifies the recipe. Combining previously separate treatment baths changes the process and may also reduce filling, draining, and heating operations. These are distinct sources of potential savings. Which Functions Can They Combine? Check the technical data sheet and application guidance to establish which functions the selected formulation supplies. Function Purpose Main verification Wetting and penetration Help liquor enter the textile evenly Performance at the intended alkali level, temperature, and circulation rate Detergency and emulsification Help release and suspend waxes, oils, and processing contamination Removal of the actual impurity load Dispersion Limit redeposition of removed material Cleanliness after washing and absence of deposits Metal-ion control Bind specified ions and limit associated interference Capacity for the relevant ions under working conditions Peroxide stabilization Limit unwanted peroxide decomposition Peroxide behavior, whiteness, and fabric condition Alkalinity Supply some or all of the required alkali Working pH, available alkalinity, and any additional alkali requirement Fast wetting does not establish complete oil removal. Likewise, metal-ion control and peroxide stabilization need separate assessment even when one formulation provides both. A Cotton-Knit and Yarn Application Sylic P1112 (F600) multifunctional pretreatment agent combines alkali, scouring, and stabilizing functions for cotton-knit and yarn pretreatment. It suits processes that need these functions together while retaining separate control of peroxide addition. The following conditions provide a starting point for application trials: Parameter Cotton-knit and yarn trial range Sylic P1112 (F600) 1–3 g/L Hydrogen peroxide, 30% solution 2–6 g/L Additional sodium hydroxide or sodium carbonate 0–1 g/L, as required Liquor ratio 1:4–1:8 Treatment temperature 95–100°C Holding time 50–60 minutes These application ranges are specific to the product and process. Follow the product-specific addition sequence and validate these conditions on the intended textile and equipment. The fixed combination reduces separate auxiliary additions but offers less independent adjustment of alkali, scouring, and stabilization than separately dosed products. What May Still Require Separate Treatment? Bleaching and Alkali Adjustment A peroxide stabilizer does not supply the bleaching chemical. Hydrogen peroxide remains a separate addition unless the formulation explicitly incorporates a suitable bleaching system. Separately dosed hydrogen peroxide bleaching stabilizers may still be needed when built-in stabilization is insufficient for the complete bath. Assess peroxide behavior together with whiteness and fabric strength. An alkaline multifunctional product can reduce caustic soda additions while maintaining an alkaline bath. Measure working pH and alkalinity rather than using the pH of a diluted product sample to predict operating conditions. Keep concentration calculations consistent: 4 g/L of a 30% hydrogen peroxide solution supplies 1.2 g/L of active hydrogen peroxide. This is a calculation example, not a recommended dose. Desizing and Difficult Contamination Sized woven fabrics need treatment matched to the sizing system. Starch, polyvinyl alcohol, and mixed sizes may require different removal conditions. Amylase can support starch desizing, but compatibility with the proposed bath must be established. Other needs may include: Additional emulsifying or degreasing support for heavy knitting oil or spin finishes. Adequate penetration and uniform liquor flow through dense fabrics or yarn packages. A compatible lubricant for crease-sensitive goods. Conditions that preserve elasticity and dimensional stability in cotton/elastane blends. A separate supporting auxiliary is often more practical when only one function needs strengthening. Increasing the multifunctional product raises all its components together. Washing and Post-Bleach Cleanup Washing must remove released impurities and residual chemicals. Check water exchange, circulation, and carryover before reducing the washing sequence. Before oxidation-sensitive dyeing, test residual peroxide and remove it as required. Catalase decomposes hydrogen peroxide into water and oxygen within the selected enzyme’s operating conditions. Verify the result by testing. Check fabric pH after washing and any required neutralization. Peroxide removal and pH adjustment address different residues. When to Use a Combined Formulation Fixed combinations are easiest to manage when incoming material, contamination, water quality, and production conditions remain reasonably consistent. Match the preparation target to the end use. Towels require consistent absorbency; pale shades and white goods require close control of the bleached base. Cotton/elastane goods also need checks on stretch recovery. Separate or hybrid recipes provide more flexibility when requirements change independently. Harder water may require more metal control without additional detergent. A heavier oil load may require more emulsification without more alkali. In these cases, retain a multifunctional base product and adjust the specific supporting auxiliary. How to Select and Validate the Recipe Map Functions and Operating Conditions Identify the purpose of each ingredient in the existing recipe. Establish which functions the replacement supplies at its proposed dose, then confirm: Fiber composition, construction, and contamination. Machinery, liquor ratio or wet

Explore More »

Azo Dyes in Textiles: Restrictions, Testing, and Compliance

Table of Contents 1. Azo Dye Chemistry and Textile Uses What Is an Azo Dye? Where Are Azo Dyes Used? 2. Restricted Aromatic Amines How Azo Dyes Release Amines Which Amines Are Restricted? What Does “Azo-Free” Mean? 3. Compliance Requirements EU REACH Restrictions Destination-Market Rules Buyer RSLs and Chemical Standards 4. Azo Dye Testing Textile Test Methods Reading Test Reports 5. Buyer and Supplier Requirements Documents Buyers Should Request Selecting Suitable Dyes Managing Noncompliance FAQ Are All Azo Dyes Banned in Textiles? Does “Azo-Free” Mean REACH Compliant? Does ZDHC MRSL Conformance Replace Finished-Textile Testing? A dye that meets shade and fastness targets can still fail a customer’s chemical specification. For textile manufacturers and buyers, selecting azo dyes therefore requires both technical evaluation and reliable compliance evidence. Azo dyes are not universally banned. Restrictions target certain colorants and the aromatic amines they can release. Sound purchasing decisions depend on distinguishing dye chemistry, chemical-input controls, and finished-textile compliance. 1. Azo Dye Chemistry and Textile Uses What Is an Azo Dye? An azo dye contains one or more azo linkages, written as –N=N–, within its molecular structure. These linkages form part of a conjugated system that absorbs visible light. The surrounding molecular structure influences the resulting color and other properties. “Azo” describes chemical structure. “Reactive,” “direct,” “acid,” and “disperse” describe application classes, so a dye can belong to both categories. For example, azo direct dyes combine azo chemistry with the application characteristics of direct dyes. Reactive, acid, and disperse dye ranges can also include azo structures. Application class alone does not establish which restricted amines an individual product could release. Where Are Azo Dyes Used? For cotton and viscose, select reactive dyes according to the fixation process. The Skyzol KE/TE series uses monochlorotriazine reactive groups and is suited to dyeing at 80°C, including applications on viscose, towels, and mercerized cotton. It is not suitable for cold pad-batch processing. This process fit does not establish the azo structure or restricted-amine status of an individual shade; confirm those separately through product-specific information and test evidence. Disperse dyes are widely used on polyester, while acid dyes are commonly used on wool and nylon. 2. Restricted Aromatic Amines How Azo Dyes Release Amines Under reducing conditions, azo linkages can split through reductive cleavage. The resulting compounds depend on the colorant’s molecular structure. Certain azo dyes can release restricted aromatic amines. Laboratory tests use controlled conditions to assess this behavior. They do not simply measure dye washing off fabric, and their results are not direct predictions of exposure during ordinary wear. Two potential sources of amines should be distinguished: Amines released by cleavage: Compounds formed when the colorant breaks down under the specified test conditions. Free amine impurities: Residual compounds already present in a formulation or material. An unsuitable molecular structure and an impurity may require different corrective actions. Neither can be identified from shade alone. Which Amines Are Restricted? The REACH Appendix 8 list of aromatic amines contains 22 entries. Examples include benzidine, CAS 92-87-5; o-toluidine, CAS 95-53-4; and 4-aminoazobenzene, CAS 60-09-3. Compare CAS numbers as well as names when reviewing specifications. Different chemical names may refer to the same substance. Buyer lists may cover additional amines and related salts. A test panel covering the EU list may therefore be insufficient for a particular customer. What Does “Azo-Free” Mean? “Azo-free” is often used loosely in purchasing specifications. It may mean that no azo-structured colorants are permitted, or it may mean that a material must pass a restricted aromatic amine test. Define the term in writing before approval, specifying substances, test methods, acceptance limits, reporting limits, and components covered. 3. Compliance Requirements EU REACH Restrictions REACH Annex XVII Entry 43 prohibits the use of azo dyes that can release the listed aromatic amines above 30 mg/kg under specified testing conditions in textile and leather articles within scope, or their dyed parts. Nonconforming articles must not be placed on the market. The relevant articles are those that may come into direct and prolonged contact with skin or the oral cavity, including clothing, bedding, towels, and certain footwear and accessories. The threshold concerns individual listed amines released during testing. It is not a maximum concentration for all azo dyes in fabric or dye powder. Entry 43 also contains a separate restriction on colorants identified in Appendix 9. Passing an aromatic amine test alone should therefore not be presented as proof that every provision has been met. Destination-Market Rules Identify where the finished goods will be sold before finalizing the chemical specification. The manufacturing country does not determine all requirements for an export order. Confirm: Destination markets and product category. Intended use and relevant contact with skin or the mouth. Applicable legal requirements. The customer’s current restricted substances list. Testing and documentation requirements for individual components. A report prepared for a previous order may be useful, but its substance coverage, methods, and limits must match the new requirements. Buyer RSLs and Chemical Standards Legal restrictions, buyer specifications, and voluntary certification programs assess different aspects of the supply chain. Requirement or program What it addresses Key purchasing check REACH Entry 43 Restricted azo colorants and released amines in articles within scope Confirm product scope and applicable restrictions AFIRM RSL Restricted substances in finished-product component materials The 2026 list specifies 20 ppm each for listed azo-amines and arylamine salts, with a separate 5 ppm reporting limit ZDHC MRSL Restricted substances in manufacturing chemical formulations Verify conformance evidence for the exact chemical product OEKO-TEX STANDARD 100 Harmful-substance testing and certification of textiles Check certificate validity, article scope, and product class OEKO-TEX ECO PASSPORT Assessment and certification of chemicals, colorants, and auxiliaries Confirm that the supplied chemical product is covered A buyer may adopt an industry RSL or issue a separate specification. Confirm the version governing the order. An RSL addresses substances in finished materials or products. An MRSL addresses manufacturing chemical inputs. Conformant inputs help control risk, but they do not automatically establish finished-fabric compliance. When selecting ZDHC-conformant textile chemicals, match the product

Explore More »
Cotton lab dips compared during reactive dye selection.

Reactive Garment Dyeing: Process, Dyes, and Defect Control

Table of Contents 1. Selecting Reactive Dyes Fiber and Component Compatibility Dye Compatibility and Process Suitability Fastness and Processing Cost 2. Selecting Dyeing Auxiliaries Pretreatment Auxiliaries Dyeing Auxiliaries and Process Chemicals Wash-Off and Finishing Auxiliaries 3. The Reactive Garment Dyeing Process Step 1: Inspect and Prepare the Garments Step 2: Prepare and Add the Dyes Step 3: Control Exhaustion and Fixation Step 4: Rinse, Wash Off, and Finish 4. Improving Shade Reproducibility Standardize Materials and Chemical Inputs Validate Lab-to-Bulk Transfer Assess Color Under Agreed Conditions Use Batch Records to Investigate Variation 5. Controlling Common Dyeing Defects FAQ Is a fixing agent necessary after reactive garment dyeing? How can backstaining be reduced during washing-off? A cotton T-shirt can match the approved body shade and still fail inspection because the collar is darker, the seams remain pale, or crease marks appear after drying. Garment dyeing brings together fabrics, threads, trims, and multilayer areas that may respond differently to the same bath. Reactive garment dyeing colors assembled cellulosic garments through dye exhaustion and covalent fixation. Hydrolysis competes with fixation, leaving unfixed color that must be washed off. This guide covers dye selection, auxiliaries, process control, and defect prevention in industrial exhaust dyeing of cotton and other suitable cellulosic garments, including considerations for blends. 1. Selecting Reactive Dyes Fiber and Component Compatibility Check the complete garment specification before developing the recipe. Include body fabric, ribbing, pocketing, sewing thread, interlinings, labels, and trims. Two cotton components can develop different shade depths because of differences in yarn, construction, mercerization, or preparation. Polyester sewing thread will not develop the same shade as cotton under a conventional cotton reactive dyeing process. Cotton-covered corespun thread may provide a closer match, but its appearance still requires a sewn-garment trial. For blends, establish which components the process will color: Cotton–polyester: Reactive dyes color the cellulosic portion. Matching the polyester requires a suitable additional dye system and compatible processing conditions. Cotton–elastane: Check temperature, alkalinity, exposure time, and mechanical action against the material supplier’s recommendations. Assess stretch recovery and dimensional stability after processing. Dye Compatibility and Process Suitability Select reactive dyes for cellulosic fibers according to the target shade, machine capability, and application conditions. Compare solubility, recommended temperature, reactivity, exhaustion behavior, and wash-off performance. Combination shades require compatible exhaustion and fixation behavior. When one dye reacts much faster than the others, dosing or temperature variation can shift the shade balance. For sensitive combination shades, Skyzol RGB uses selected M-series dyes with similar substantivity and reactivity. Match the combination to the intended process and verify its response to changes in pH, electrolyte, temperature, and liquor ratio. Similar application behavior supports recipe compatibility but does not guarantee bulk shade reproducibility. Fastness and Processing Cost Define the required wash, rubbing, perspiration, and light fastness according to the garment’s end use. Strong wash fastness does not automatically establish suitability for every other exposure. For deep shades, pay particular attention to wash-off demand and wet rubbing performance. Test after the intended finishing treatment because softening and drying can influence the final result. Compare cost per kilogram of acceptable garments. Include dye consumption, auxiliaries, water, energy, processing time, and rework rather than judging a recipe by dye price alone. 2. Selecting Dyeing Auxiliaries Select auxiliaries for a defined function and check compatibility across the complete bath. Pretreatment Auxiliaries Select textile pretreatment auxiliaries according to the impurities present and the garment’s preparation history. Wetting and scouring agents support uniform absorbency; sequestering agents help manage interfering metal ions. Prepared-for-dyeing fabric can acquire sewing oils or handling contamination during garment assembly. Check the assembled garment, not just the original fabric specification. Dyeing Auxiliaries and Process Chemicals Choose dyeing auxiliaries for the machine, garment construction, and dye system. Check leveling agents for their effect on exhaustion and color yield. Address overloading or restricted movement directly; an anti-crease agent cannot correct those conditions. Electrolyte and alkali have distinct roles in conventional reactive exhaust dyeing. Electrolyte promotes exhaustion; alkali creates conditions for dye–fiber fixation. Their quantities and addition sequence must match the selected application procedure. Product category Main function Selection checks Wetting and scouring agents Improve wetting and remove impurities Absorbency, foam, rinsability, and substrate suitability Sequestering agents Manage interfering metal ions Water quality, working pH, and dye compatibility Peroxide removal agents Eliminate residual peroxide after bleaching Working conditions and measured residual peroxide Lubricants and anti-crease agents Reduce friction and crease formation Garment movement, machine conditions, and deposit risk Leveling agents and defoamers Control uneven uptake or excessive foam where needed Bath stability, dye yield, and compatibility Soaping agents Help remove unfixed dye and limit redeposition Shade depth, water quality, residual electrolyte, and fastness Softeners Develop the required hand Shade change, spotting, absorbency, and compatibility Fixing agents, where justified Improve specific fastness properties Measured benefit and effects on shade, hand, and other requirements Wash-Off and Finishing Auxiliaries Wash-off performance depends on dye substantivity, water quality, residual chemicals, temperature, and liquor exchange. Sylic D2705 soaping agent is an anionic/nonionic surfactant–polymer powder for wash-off and anti-staining treatment of reactive-dyed cotton and rayon. Its pH of 6.0–8.0 refers to a 1% aqueous product solution, not the operating bath. Check compatibility with the other auxiliaries at the intended working conditions. Set dosage, temperature, and sequence through garment trials. For a lower-temperature route, compare fastness, staining, and final shade with the established process before reducing heat input or cycle time. The required wash-off performance takes priority over potential energy savings. Check softeners for effects on shade, absorbency, and hand. Use fixing agents only for a demonstrated fastness benefit; they do not replace fixation or effective washing-off. 3. The Reactive Garment Dyeing Process Step 1: Inspect and Prepare the Garments Confirm garment weight, component lots, preparation history, and machine loading. Keep incompatible materials or preparation histories separate. A practical readiness check includes: Uniform absorbency across body fabric and components. Removal of oils, sizing where present, and other relevant impurities. Residual pH suitable for the next stage. Acceptable process-water quality. Verified peroxide removal when bleaching has been used. Consistent cotton dyeing

Explore More »

Contact Us for Textile Auxiliaries and Dyes

Contact Skychem Group for more chemical solutions, If you have questions or need more information, please contact us.
We will respond within 24 hours

Get a project quote

Please tell us the requirements, the country and the application.

Scroll to Top
Email WhatsApp

Contact Us for Textile Auxiliaries and Dyes

Contact Skychem Group for more chemical solutions, If you have questions or need more information, please contact us.
We will respond within 24 hours