...

Contact Skychem Group for more chemical solutions, If you have questions or need more information, please contact us.
Respond within 24 hours

Delta E 2000: Common Error Sources in Textile Color Measurement

Color accuracy when using Delta E 2000 (ΔE2000) is essential to ensure the quality of textiles continues to improve over time. To that end, this paper discusses the potential sources of error encountered when measuring ΔE2000, which includes instrument calibration, sample preparation, and environmental conditions, and offers methods to help eliminate these errors so that the highest quality and the most consistent results are achieved.

Delta E 2000 Color Management

Spectrophotometer Calibration Issues

Measurement errors most frequently arise from the process of calibration. The instrument needs standard white reference calibration, and drift monitoring because it produces unreliable measurements. Regular calibration is crucial to ensure reliable color readings. The manufacturers need to create a standard calibration plan, which becomes essential when instruments relocate to new settings. This is important after extended periods of operation. Using certified calibration standards also ensures accuracy across different instruments and testing locations.

For more advanced tools and techniques in calibration, explore our textile color solutions, where Skychem offers specialized products designed to ensure precise color measurements in textile production. Our solutions help maintain consistency and accuracy across different instruments and environments.

Variations Between Different Instruments

The design elements of spectrophotometers, along with their spectral range and individual settings, lead to minor variations in their measurement results. The use of multiple instruments during production leads to inconsistent results because instruments operate at different times throughout the manufacturing process. Manufacturers should implement instrument standardization across all testing facilities as a solution to reduce this problem. The use of calibration software for multiple instruments enables standardization of measurements across different devices, which produces consistent results.

To standardize instruments across your facilities and improve measurement consistency, visit Skychem’s textile chemicals manufacturer, where we provide cutting-edge textile chemical solutions that support optimal calibration and consistent results across all testing devices.

Light Source Instability or Incorrect Illuminant Settings

The stability and type of light source used in color measurements play a significant role in the accuracy of ΔE2000 readings. For instance, fabrics intended for use under natural light should be measured using daylight as the light source. If an incorrect illuminant is used, it can cause inaccurate readings and affect the final color evaluation. Regular checks and calibration of the light source are essential to ensure stable, consistent lighting conditions, which are crucial for reliable color measurements.

Aperture Size Mismatch with Fabric Texture

The spectrophotometer needs an aperture size that matches the fabric’s texture. The instrument will fail to capture the entire fabric color when the aperture size does not match the fabric texture because it becomes too big for fine-textured materials or too small for thick materials. The different dimensions between the materials will produce incorrect measurement results. Manufacturers should adjust the aperture size based on fabric thickness and texture to ensure accurate color measurements. The proper calibration of the aperture prevents measurement errors while keeping consistent results when working with various fabric types.

Sensor Aging or Contamination on Optical Components

Spectrophotometer sensors experience wear and tear because dust particles and other contaminants accumulate on them during regular operation. The color reading accuracy suffers when the sensor detects dust or particles that interfere with detection. The spectrophotometer requires ongoing maintenance because optical parts need cleaning, and sensors must be replaced when they show signs of wear to maintain proper operation. Air purifiers, together with environmental monitoring systems, help minimize contamination risks, which results in better equipment durability.

Spectrophotometer

Fabric Texture Affecting Light Scattering

Fabric texture determines the way light bounces off surfaces, which directly affects the results of color measurement processes. The way light bounces off different fabric textures, including knits and woven materials, and pile and fleece, results in small differences in how people see colors. To minimize this, manufacturers should adjust sampling methods based on fabric texture. The study of how texture affects light dispersion helps scientists achieve better color measurement results when working with different fabric materials.

Surface Directionality or Shading

Fabrics with directional surfaces, such as brushed or napped materials, can show varying colors depending on the angle at which the measurement is taken. The measurement process gets affected by the color variation because it causes inconsistent results when using ΔE2000. The method requires measurements at one specific angle or multiple measurements from different angles to correct shading errors. The elimination of this error source depends on using standardized sample preparation and testing procedures, which lead to more precise results.

Inconsistent Sample Preparation or Folding

The incorrect folding of fabric samples, along with inconsistent folding methods, creates alterations in light reflection, which results in incorrect measurement results. The ΔE2000 reading becomes affected by tiny fabric wrinkles and folds, which produce color inconsistencies. Standardizing sample preparation practices, such as flattening the fabric and ensuring it is properly aligned in the spectrophotometer, ensures that color measurements are consistent and reliable across tests.

Moisture Content Changes Before Measurement

Moisture content stands as a crucial factor that determines how a fabric looks while also affecting its color. The light absorption and scattering properties of fabric become distorted when moisture levels fluctuate because of humidity variations or inadequate storage conditions, which results in inaccurate color measurements. Manufacturers need to maintain fabric sample moisture stability when they take measurements by using moisture meters and setting fabric moisture levels to specific controlled conditions.

Dye Migration or Uneven Dyeing

Uneven dyeing or dye migration within a fabric sample can cause discrepancies in color measurements. When dye is not evenly applied or migrates during production, color variations can occur within the same sample, leading to unreliable ΔE2000 readings. To prevent this, manufacturers should closely monitor dyeing processes and ensure that dyes are applied uniformly. Additionally, fabric should be properly fixed to prevent dye migration, ensuring consistent color measurement results.

To ensure even dye application and prevent inconsistencies in your fabric, explore our textile color solutions by Skychem. We specialize in textile treatments that help achieve uniform dyeing and prevent migration, ensuring the highest color accuracy in your measurements.

Measurement Condition Errors

Inconsistent Measurement Geometry

The measurement geometry, such as 45/0 or d/8, plays a significant role in how color is captured. The way light interacts with fabric depends on these specific geometries, which determine its behavior with both glossy and matte surfaces. The use of consistent measurement geometry throughout all tests produces results that can be reliably duplicated. Manufacturers should select the correct geometry based on fabric finish and texture to ensure the measurement accurately reflects the fabric’s true color.

Diffferent Fabric Texture

Impact of Measurement Geometry on Glossy vs Matte Surfaces

Glossy and matte fabrics reflect light differently, which can lead to discrepancies in color measurements if the geometry of the measurement isn’t adjusted accordingly. Glossy fabrics tend to reflect light at a higher angle, leading to potential color differences depending on the viewing angle. Understanding how measurement geometry impacts the perceived color of glossy and matte surfaces allows manufacturers to optimize their measurement methods for greater accuracy.

For detailed guidance on adjusting measurement geometry based on fabric finish, visit Skychem’s textile chemicals manufacturer. We provide specialized textile solutions designed to help you optimize measurement techniques and improve color consistency for all fabric types, including glossy and matte finishes.

Incorrect UV Content Settings for Optical Brighteners

Manufacturers apply optical brighteners to various textiles in order to achieve better whiteness results. The UV light measurement system requires proper calibration because uncalibrated UV settings result in inaccurate ΔE2000 measurement results. The process of adjusting UV content for fabrics that have optical brighteners applied requires absolute precision to produce accurate measurement results. The measurement process for textiles with optical brighteners requires manufacturers to consider UV light effects because this produces accurate color measurement results.

Backing Material Differences

The selection of backing material during color measurement procedures leads to major changes in the measurement outcomes. The selection of backing materials between white, black, and neutral gray bases impacts light reflection patterns, which affects the precision of color measurement results. Neutral gray functions as the most precise color measurement tool because it stays neutral without affecting the way fabric colors appear to viewers. Standardizing backing materials ensures that color measurements are consistent and reliable across different testing environments.

Temperature and Humidity Variations in the Lab

Temperature and humidity levels in the environment influence how fabric looks while also affecting the operational capabilities of spectrophotometers. The measurement results will show inconsistencies because of the different environmental conditions. Maintaining a steady testing environment with proper control proves vital for obtaining dependable and repeatable color measurement results. Manufacturers should monitor and regulate temperature and humidity levels to ensure that external factors do not interfere with the accuracy of measurements.

Operator Handling Differences

Operator handling can significantly affect the consistency of color measurements. The process of measuring color consistency faces two main sources of errors, which are pressure differences and placement and repeatability issues. Standardized procedures and operator training programs work together to guarantee that measurement consistency exists. The production of operators needs to be trained by manufacturers who must develop exact protocols that maintain measurement consistency.

Environmental Factors

Temperature Fluctuations During Testing

Temperature fluctuations in the testing environment can alter fabric color. Some fabrics may shrink or expand slightly with temperature changes, which can affect the measurement. Maintaining a constant temperature during testing ensures that color readings are not influenced by environmental changes. Manufacturers should control the temperature of the testing environment to minimize any temperature-related measurement variations.

Humidity Levels and Their Impact on Fiber Moisture Content

As mentioned earlier, moisture content is critical for accurate color measurement. Humidity levels can affect fiber moisture content, leading to changes in reflectance and, consequently, color accuracy. Ensuring that humidity levels are controlled in the testing environment helps minimize this issue. Manufacturers should maintain consistent humidity levels to ensure that fabric moisture content remains stable during measurement.

To better manage moisture content and improve color consistency, Skychem’s textile color solutions offer effective treatments that stabilize fabric conditions during testing, ensuring your measurements remain accurate regardless of environmental fluctuations.

Ambient Light Variations Affecting Color Perception

Ambient light can influence the perceived color of fabrics. Variations in surrounding light can cause discrepancies in color measurements. Using controlled lighting conditions during testing, such as those provided by a spectrophotometer with stable illumination, ensures that ambient light does not affect the results. Manufacturers should make sure that testing occurs in a controlled environment with consistent lighting.

Storage and Transport Conditions

Fabrics exposed to sunlight or extreme temperatures during storage or transport can change color. These changes can affect color consistency when the fabric is measured later. Proper storage and transport conditions are crucial to preserving fabric color integrity. Manufacturers should store fabrics in temperature- and humidity-controlled environments to protect them from exposure to harsh conditions.

Airborne Pollutants or Dust Influencing Sample Appearance

Dust and pollutants can settle on fabric surfaces, affecting how light is reflected and, in turn, altering the color readings. Keeping the testing environment free from airborne contaminants ensures accurate fabric measurements. Manufacturers should use clean rooms or air filtration systems to maintain a dust-free testing environment.

Standard and Methodology Issues

Improper Use of ΔE2000 Parameters

The incorrect application of ΔE2000 parameters, including SL, KC, and KH, results in incorrect color measurement results. The process of obtaining precise outcomes requires knowledge about how to modify these parameters according to fabric type and environmental conditions. Manufacturers should ensure that the ΔE2000 formula parameters are applied consistently to match the fabric’s characteristics.

Impact of Reference Standard Choice on ΔE2000 Calculation

The reference standard used in ΔE2000 calculations influences the accuracy of the color difference results. The use of wrong or old standards results in measurement differences. The measurement accuracy depends on the correct and current status of reference materials. Manufacturers need to update their reference standards on a regular basis to match contemporary color trends and material characteristics.

Inconsistent Color Standards or Outdated Reference Swatches

Outdated color standards and inconsistent standards create measurement differences when various tests or suppliers perform color evaluations. The process of regular updates and maintenance of reference swatches helps maintain testing accuracy and uniformity. Manufacturers need to follow industry-standard color libraries while performing necessary swatch replacements and recalibrations.

Insufficient Number of Readings Per Sample

The natural variations in fabric color cause unreliable ΔE2000 values when only a small number of readings are taken from a sample. Multiple point readings across the sample help researchers obtain more precise measurement results. Manufacturers need to create protocols that define the required number of readings for each fabric type and its anticipated level of uniformity.

Lack of Alignment on Tolerance Limits Between Suppliers and Brands

The acceptance of color proves to be problematic because suppliers and brands cannot reach an agreement about the allowed color tolerance limits. Establishing precise and uniform tolerance boundaries allows all parties to reach consensus about which color variations stay within acceptable limits. Manufacturers should establish common color tolerance standards across the supply chain to avoid confusion and reduce disputes.

Conclusion

Understanding the potential sources of error in ΔE2000 measurements is essential for maintaining color consistency and product quality. By standardizing testing procedures, controlling environmental factors, and ensuring proper calibration and sample preparation, manufacturers can reduce measurement errors and enhance color accuracy. For a comprehensive overview of reliable solutions, visit https://skychemi.com/textile-solutions/ and feel free to contact us for more details!


Recommended reading:

  1. Color Difference Formula and ΔE: CIE Standards and Color Tolerance
  2. What are L*,a*,b*,C*,h°,DL*,Da*,Db*,DC*,DH*,DE*,DEcmc?
  3. Crepe vs. Silk: How Textile Auxiliaries Enhance Their Performance

Sandy

With years of experience in chemical dyes and textile auxiliaries, I’m dedicated to sharing insights into the latest technologies, sustainable innovations, and market trends.

Recent Articles

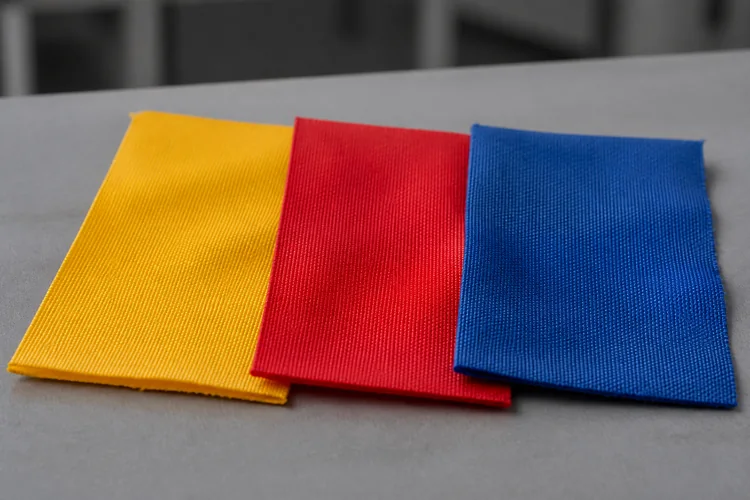
Yellow, red, and blue nylon swatches representing a compatible trichromatic acid dye set.

Trichromatic Acid Dye Selection for Consistent Nylon Shades

Table of Contents Understanding Strike Rate Factors Influencing Strike Rate Matching Strike Rates in a Combination The Role of pH in Dye Uptake pH Ranges by Dye Class Controlling pH During Dyeing Trichromatic Selection Principles Choosing Compatible Yellow, Red, Blue Typical Trichromatic Acid Dye Combinations for Nylon Light Shade Trichromatic Combination Deep Shade Trichromatic Combination Migration and Buildup Properties Avoiding Shade Shift Practical Recipe Guidelines Lab Trial Checklist FAQs What causes uneven dyeing with acid dyes on nylon? How does pH control affect reproducibility? What makes a trichromatic combination reliable? Nylon dyeing rewards precision. Acid dyes bond well with polyamide fibers, but shade consistency depends on how closely strike rate, pH, and trichromatic combinations are controlled together. A small mismatch in any one variable can shift a shade off standard, even when the recipe looks correct on paper. This article breaks down the practical factors that keep acid dye combinations compatible on nylon. Understanding Strike Rate Strike rate describes how quickly a dye moves from the bath onto the fiber. On nylon, this speed depends on dye structure, temperature ramp, and the number of available dye sites on the substrate. A dye with a fast strike rate can produce uneven color if it exhausts before the bath fully penetrates the goods, particularly on tightly constructed knits or dense yarns. Factors Influencing Strike Rate Three variables have the greatest effect on how fast a given acid dye takes up on nylon: Molecular size and structure: smaller, more mobile molecules tend to migrate and level more readily, while larger or more linear structures strike faster but migrate less once fixed. Electrolyte concentration: higher salt levels in the bath slow strike by increasing ionic competition at the fiber surface, which can help leveling but may reduce total exhaustion if not balanced correctly. Temperature ramp speed: a ramp that heats too quickly gives the dye little time to migrate before fixation, raising the risk of streaks or tailing on the goods. Matching Strike Rates in a Combination When combining dyes for a shade, each component should have a comparable strike rate. If one dye in a mix strikes noticeably faster than the others, it dominates the early stages of dyeing and shifts the shade as the bath progresses. This is one of the most common causes of reproducibility problems in nylon dyehouses, especially when recipes are adjusted without checking how the new combination behaves as a system rather than as individual dyes. The Role of pH in Dye Uptake Acid dyes require an acidic bath to bond effectively with the amine groups on nylon fiber. pH does more than set the chemical environment; it also governs how fast dye uptake occurs and how much correction is possible once dyeing has started. pH Ranges by Dye Class Different acid dye classes are formulated to perform within specific pH windows. Working outside that window changes uptake speed and can affect fastness properties. Dye Class Typical pH Range Uptake Behavior Leveling acid dyes pH 5 to 6 Slower strike, good migration, easier to correct Milling acid dyes pH 4.5 to 5.5 Moderate strike, less forgiving on unlevel dyeing Metal complex acid dyes pH 4 to 5 Faster strike, stronger fastness, tighter process control needed These ranges are starting references. Actual performance depends on the specific dye grade, liquor ratio, and machine type, so lab confirmation on the intended substrate remains necessary before scaling to bulk. Controlling pH During Dyeing Holding pH steady throughout the cycle matters as much as setting the correct starting point. A pH that drifts upward during dyeing slows uptake and can leave the shade pale or uneven, while a sharp early drop can cause the dye to strike too fast for proper migration. Buffering systems and controlled acid addition keep the bath within range from start to finish. Leveling agents and buffering auxiliaries formulated for pH and strike control help stabilize uptake speed across different fabric constructions and machine conditions, particularly on constructions prone to rapid initial strike. Trichromatic Selection Principles Trichromatic dyeing uses a yellow, red, and blue dye to build a wide range of shades from a small working palette. Compatibility across these three dyes determines how predictable the resulting shades will be, both in the lab and in bulk. Choosing Compatible Yellow, Red, Blue A workable trichromatic set should share similar strike rates, similar pH sensitivity, and comparable migration behavior. Mismatched components can produce shade drift between lab dips and production batches, even when the total dye concentration is correct. The Skyacido Acid Dyes, formulated specifically for polyamide dyeing, offers a wide shade gamut with strong inter-shade combinability, which supports matching yellow, red, and blue components as a coordinated set rather than selecting each color independently based on shade alone. The table below outlines what to check across each primary when building a trichromatic set: Component Strike Rate Check pH Sensitivity Migration Behavior Yellow Compare exhaustion curve against red and blue Note shift point where uptake accelerates Confirm redistribution at hold temperature Red Compare exhaustion curve against yellow and blue Note shift point where uptake accelerates Confirm redistribution at hold temperature Blue Compare exhaustion curve against yellow and red Note shift point where uptake accelerates Confirm redistribution at hold temperature Running this comparison during lab dip development, rather than after a bulk batch shows shade drift, catches mismatches while they are still inexpensive to correct. Typical Trichromatic Acid Dye Combinations for Nylon In practical nylon dyeing, trichromatic combinations are usually selected according to shade depth, buildup requirement, and compatibility between dyes. Different combinations may be required for light shades and deep shades to maintain balanced exhaustion, migration, and shade reproducibility. Light Shade Trichromatic Combination For light and medium shades, dyes with good migration performance and moderate strike behavior are preferred to achieve excellent leveling and shade correction ability. A typical light shade combination may include: Trichromatic Position Example Acid Dye Yellow Skyacido Yellow 199 Red Skyacido Red 337 Blue Skyacido Blue 324 This combination provides good compatibility and is

Explore More »
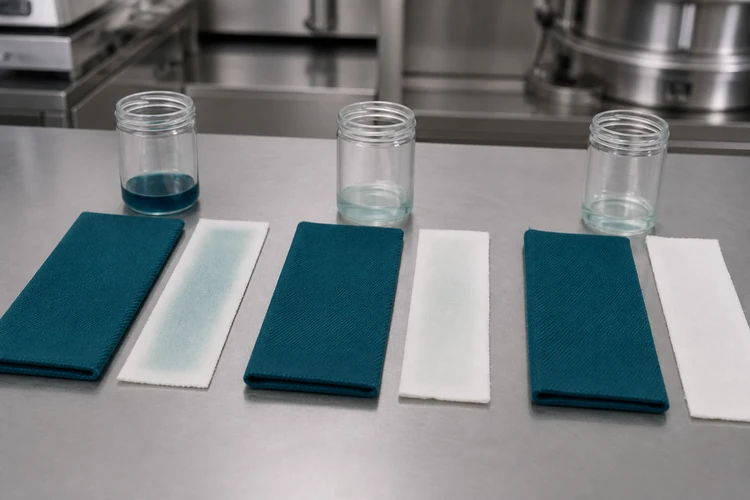
2. Low-temperature soaping leaves clearer wash liquor and less staining on adjacent white cotton strips.

Reactive Dye Soaping Guide: Better Wash Fastness, Less Back-Staining

Table of Contents What Is Reactive Dye Soaping Role in the Wash-Off Stage Why Unfixed and Hydrolyzed Dye Must Be Removed How Soaping Affects Wash Fastness Removing Hydrolyzed Dye from the Fiber Surface Connection Between Soaping and Fastness Ratings What Causes Back-Staining? Common Sources of Back-Staining Fabrics and Blends Most at Risk Key Process Parameters for Effective Soaping Temperature and Time Liquor Ratio Water Hardness and Sequestering Agents Choosing the Right Soaping Agents Anionic and Nonionic Soaping Agents Matching Agents to Fiber and Shade Depth Low-Temperature Soaping Agent Option: Sylic D2705 Key Benefits Recommended Application Performance Comparison Soaping Process Methods Cold Wash and Hot Wash Sequence One-Bath vs Multi-Step Soaping Role of Fixing Agents After Soaping Best Practices for Consistent Wash Fastness Results FAQs How long should reactive dye soaping take? Can back-staining be fixed after it happens? Does hard water affect soaping performance? Is a separate fixing agent always necessary after soaping? Reactive dye soaping is often treated as a quick step at the end of the dyeing cycle, but it has a direct effect on wash fastness and back-staining outcomes. Getting temperature, time, and agent selection right prevents costly rejects and repeat orders that eat into margins. What Is Reactive Dye Soaping Role in the Wash-Off Stage Soaping takes place after fixation, once the reactive dye has bonded to the fiber under alkaline conditions. Fabric is washed at or near boiling temperature with a detergent or specialty soaping agent to strip away everything that never formed a permanent bond with the fiber. Skipping or shortening this step leaves wash-off incomplete, and the fabric carries a hidden fastness risk that will not surface until later testing or, worse, after it reaches the customer. Why Unfixed and Hydrolyzed Dye Must Be Removed A portion of reactive dye always hydrolyzes in the dyebath instead of reacting with the fiber. Hydrolyzed dye sits loosely on the fabric surface, held only by weak physical attraction rather than a covalent bond. Left in place, it rubs off during handling, bleeds during laundering, and transfers onto lighter fabrics in the same wash load. Soaping is the step designed specifically to remove this residue before it becomes a fastness problem. How Soaping Affects Wash Fastness The quality of soaping determines much of what shows up later in fastness testing. A batch that looks correct on the shade card can still fail to wash or rub fastness if this step was rushed. Removing Hydrolyzed Dye from the Fiber Surface Effective soaping keeps loosened dye suspended in the wash liquor instead of letting it settle back onto the fabric. How completely this happens depends on agitation, liquor ratio, and the dispersing strength of the detergent or soaping agent used. Connection Between Soaping and Fastness Ratings Wash and rub fastness ratings, most commonly evaluated using AATCC colorfastness test methods, largely reflect how much unfixed dye remains after wash-off. A fabric can pass an initial shade check on the lab dip and still fail fastness testing on the bulk batch if soaping ran too briefly or at too low a temperature. What Causes Back-Staining? Common Sources of Back-Staining Back-staining happens when dye that has washed off the dyed fabric redeposits onto undyed or lighter areas in the same bath. The most common causes include: Overloaded soaping baths carrying more hydrolyzed dye than the liquor can hold Insufficient rinsing between soaping and finishing steps Soaping agents with weak dispersing power, which allow free dye particles to settle back onto the fabric Uneven liquor circulation, which creates localized zones of high dye concentration Fabrics and Blends Most at Risk Deep and dark shades generate the highest load of hydrolyzed dye and are the most frequent source of back-staining complaints. Blended fabrics, and any load that mixes dyed and undyed components, are particularly vulnerable, since redeposited dye is far more visible on the lighter portion of the fabric. Key Process Parameters for Effective Soaping Most causes of poor fastness and back-staining trace back to how tightly these three parameters are controlled. Temperature and Time Soaping typically runs at or close to boiling point for five to fifteen minutes, though the ideal combination depends on shade depth and fabric construction. Running the bath too cool slows dye removal, and cutting the time short leaves hydrolyzed dye behind even at the correct temperature. Shade depth Soaping temperature Typical time Light to medium 90 to 95°C 5 to 8 minutes Deep and dark Near boiling (98 to 100°C) 10 to 15 minutes Turquoise and problem shades Near boiling, multi-bath 15 minutes or more per bath This near-boiling range applies to conventional soaping agents. Low-temperature soaping agents are formulated to work effectively at 60 to 80°C instead, cutting energy use without giving up fastness performance (see the Sylic D2705 section below).  Liquor Ratio A tighter liquor ratio concentrates hydrolyzed dye in a smaller volume of water, which increases the risk of redeposition before it can be flushed out. Mills running jet or overflow machines at lower liquor ratios should compensate with stronger dispersing agents or an added rinse cycle. Water Hardness and Sequestering Agents Calcium, magnesium, and iron in the water supply interfere with soaping agent performance and can leave a hazy or uneven finish. A sequestering agent, such as Sylic P1501B, an anionic chelating dispersant with a pH of 2.5 to 4.0 in a 1% solution, binds these ions before soaping begins and lets the soaping agent perform as intended. Choosing the Right Soaping Agents Anionic and Nonionic Soaping Agents Anionic soaping agents are widely used for their strong dispersing action, while nonionic types perform better in hard water and at lower temperatures. Both types are available within a dyeing auxiliary range formulated for stability in alkaline baths and low-foam performance in jet machines. Matching Agents to Fiber and Shade Depth Cotton and other cellulosic fibers generally respond well to anionic soaping agents. Blends containing synthetic fibers may need a nonionic option instead, to avoid staining the more sensitive synthetic component. Deeper shades typically call

Explore More »

Reduction Clearing in Polyester Dyeing: A Complete Guide

Table of Contents What Is Reduction Clearing? Definition and Purpose Role in Disperse Dyeing Impact on Colorfastness Common Quality Complaints When Reduction Clearing Is Needed Dark and Medium Shades High Dye Concentration Recipes Blends with Cellulosic Fibers When It Can Be Skipped Process and Control Typical Recipe and Parameters Controlling Temperature and pH Avoiding Over-Reduction or Under-Reduction Rinsing and Neutralization Choosing the Right Reducing Agents Sodium Hydrosulfite Sulfur-Free Reducing Agents Low-Temperature and Sustainable Options High Wash Fastness Dyes to Reduce Clearing Load Troubleshooting Common Issues Poor Wash Fastness After Clearing Shade Change or Dulling Conclusion FAQs What Happens If You Skip It? Reduction Clearing vs Normal Washing? Can It Be Done at Low Temperature? Hydrosulfite vs Sulfur-Free Agents? A batch that looks perfect on the machine can still fail a wash fastness test days later. More often than not, the cause is unfixed disperse dye left on the fiber surface, and the fix is reduction clearing. This guide covers when the step is necessary, the chemistry behind it, and how to keep results consistent from lab dip to bulk production. What Is Reduction Clearing? Definition and Purpose Reduction clearing is a post-dyeing treatment that removes disperse dye which has not penetrated or fixed onto polyester fibers. During high temperature dyeing, some dye molecules remain on the fiber surface instead of diffusing into the polymer structure. Left untreated, this residual dye rubs off and bleeds during washing, lowering overall color fastness. A reduction clearing bath breaks down and strips away the surface dye, leaving only the dye that has properly fixed inside the fiber. Role in Disperse Dyeing Reduction clearing takes place at the end of the disperse dyeing cycle, after the main dyeing stage and before final rinsing. It is one part of a larger polyester dyeing workflow that also includes pretreatment, dyeing, and finishing. The polyester dyeing application solutions page outlines how these stages connect, along with recommended auxiliaries for each step. Impact on Colorfastness Wash and rub fastness are among the specifications buyers check most closely before accepting a shipment. Surface dye that has not been cleared is loosely bound and washes out easily, which is precisely what standardized tests such as AATCC’s laundering fastness methods are designed to detect. A properly executed reduction clearing step improves these results by removing the dye that would otherwise cause a failed test. Common Quality Complaints Mills that skip or under-perform reduction clearing tend to see a recurring pattern of issues: Color bleeding onto lighter garments in the same wash load Staining on packaging or trims during transport and storage Dull or hazy shades compared to the approved lab dip Rejected shipments after failed fastness testing at the buyer’s lab These problems are almost always traceable to residual disperse dye rather than a flaw in the dye recipe itself, which is why reduction clearing deserves the same attention as the dyeing stage it follows. When Reduction Clearing Is Needed Dark and Medium Shades Darker and medium depth shades require higher dye concentrations, which naturally leaves more unfixed dye on the fiber surface. The Skycron disperse dyes range covers both dyeing and printing applications across dark, medium, and vivid shades, and pairing these dyes with a proper reduction clearing step is standard practice for reaching acceptable fastness at these heavier depths. High Dye Concentration Recipes Any recipe with a high total dye percentage on weight of fabric (% o.w.f.) benefits from reduction clearing, not only dark shades. As a general reference, mills commonly group shade depth this way: Shade Depth Typical Dye Concentration Reduction Clearing Light Below 1% o.w.f. Often optional Medium 1 to 3% o.w.f. Recommended Dark Above 3% o.w.f. Required These figures are a general guide rather than a fixed rule, since dye class, fiber blend, and fastness targets all shift the threshold. Multi-dye combinations used for precise custom shades fall into this same logic, as several dye classes combined can leave behind varying amounts of surface residue even at a moderate total percentage. Blends with Cellulosic Fibers Polyester-cotton and polyester-viscose blends add another layer of risk. Disperse dye that has not fixed to the polyester portion can stain the cellulosic fiber, causing an unwanted tone shift across the fabric. Reduction clearing protects the intended contrast or solid shade across both fiber types. When It Can Be Skipped Very light shades with low dye loading sometimes do not require a full reduction clearing cycle, particularly when high-exhaustion dyes and well-controlled dyeing conditions are used, and a simple hot wash can be enough. Skipping the step should still be a deliberate decision based on shade depth and fastness requirements, not a shortcut taken to save time. Process and Control Typical Recipe and Parameters A standard alkaline reduction clearing bath includes a reducing agent, caustic soda or soda ash, and a wetting or dispersing agent. Sulfur-free acid-clearing systems, which run at a lower pH, are increasingly used as an alternative. A general starting point looks like this: Parameter Typical Range Reducing agent 2 to 4 g/L Alkali (NaOH or soda ash) 2 to 4 g/L Temperature 70 to 80°C Time 15 to 20 minutes Liquor ratio 1:8 to 1:15 These figures vary by shade depth, dye class, and fiber blend, so lab trials should confirm the final recipe before scaling to bulk. Controlling Temperature and pH Temperature and pH are the two variables that most affect clearing efficiency: Too cool or too brief: residual dye is left behind, and fastness suffers. Too hot or too alkaline: the polyester surface or hand feel can be affected. Most conventional recipes target a mildly alkaline pH between 9 and 11. Acid-based sulfur-free systems instead work in a neutral to mildly acidic range, depending on the product used, so the pH target should always match the chemistry selected rather than a single fixed rule. Avoiding Over-Reduction or Under-Reduction Under-reduction leaves surface dye behind, which shows up later as poor fastness. Over-reduction strips properly fixed dye from the fiber, causing shade loss, dulling, or an uneven

Explore More »
C0 vs. C6 Water Repellent Finishes

C0 vs. C6 Water Repellent Finishes: Which One Fits Your Textiles?

Table of Contents The Chemistry Behind C0 and C6 What is C6 DWR What is C0 DWR Key Structural Differences Performance Comparison Water and Oil Repellency Durability and Wash Resistance Breathability and Hand Feel Global Regulatory Landscape REACH and EU Restrictions US State Regulations Brand and Retailer Requirements Use Cases by Industry Outdoor and Sportswear Workwear and Protective Textiles Home Textiles and Upholstery Choosing the Right Finish Key Factors to Consider Testing and Certification Tips Conclusion FAQs What is the difference between C0 and C6 finishes? Is C6 DWR banned? Does C0 perform as well as C6? How do I choose between C0 and C6? Ask a fabric supplier for a water-repellent finish today, and there is a good chance you will get two very different answers: C6, or C0. Both claim to keep fabric dry. Only one is currently facing phase-out pressure from regulators in the EU, California, and New York, and from major apparel brands. For buyers sourcing water-repellent textiles right now, the choice is no longer just about performance. It is about which chemistry will still be sellable in your target market two years from now. The Chemistry Behind C0 and C6 What is C6 DWR C6 durable water repellent (DWR) finishes use short-chain fluorocarbon polymers, specifically six-carbon fluorinated side chains, to coat individual fibers. This chemistry lowers the surface energy of the fiber to roughly 12 mJ/m², which is below the surface tension of most water and oils. As a result, C6 finishes deliver both water and oil repellency, a combination that few fluorine-free systems can fully match. C6 chemistry replaced older C8 fluorotelomer finishes over a decade ago. C8 degrades into PFOA, a substance known for being persistent and bioaccumulative in the environment. C6 degrades into perfluorohexanoic acid (PFHxA) instead, which has a shorter environmental half-life and lower bioaccumulation potential. However, PFHxA is not free of regulatory scrutiny, as covered in the compliance section below. For buyers sourcing C6 products, formulations such as the Skyguard C6-C8 Waterproofer combine water and oil resistance with good wash fastness on both cellulose and synthetic fibers, applied at typical dosages of 10 to 40 g/L, and are produced without PFOS, PFOA, or APEO. What is C0 DWR C0 refers to fluorine-free water repellent chemistry. Instead of fluorocarbon side chains, C0 finishes rely on dendrimer, wax, or polyurethane-based polymers to build a hydrophobic fiber surface. These systems typically reach a surface energy of 20 to 25 mJ/m², which is sufficient to repel water effectively but generally not enough to provide strong oil repellency. Demand for C0 finishes is growing quickly because they carry no PFAS-related compliance risk, a factor that matters more each year as regulatory scope widens. Ranges such as the Skyguard Fluorine-free Waterproofer line are applied at roughly 10 to 80 g/L depending on the durability required, contain no APEO, and are built for fabrics where oil repellency is not a functional requirement, including most outerwear, home textiles, and fashion applications. Key Structural Differences Attribute C6 (Fluorocarbon) C0 (Fluorine-Free) Surface energy Approx. 12 mJ/m² Approx. 20 to 25 mJ/m² Water repellency Excellent Good to excellent Oil repellency Yes Limited or none PFAS content Present (PFHxA-based) None Typical curing temperature 150 to 160°C 160 to 180°C Performance Comparison Water and Oil Repellency C6 finishes remain the benchmark wherever oil, grease, or organic stain resistance is needed alongside water repellency, such as workwear exposed to machine oils or food-contact aprons. C0 finishes have closed most of the gap on pure water repellency, with many recent formulations achieving results comparable to C6 under standardized water resistance testing. On oil-based stains, however, C0 finishes still fall short. Durability and Wash Resistance Both chemistries rely on physical adsorption when first applied to the fabric, and this bond weakens progressively with repeated laundering and detergent exposure. A crosslinking agent extends wash durability by binding DWR polymer chains to each other and to reactive groups on the fiber surface, converting a loosely adsorbed coating into a chemically anchored one. The Sylic Cross-linking Agent, for example, is dosed in the same bath at 10 to 30 percent of the water repellent quantity, contains no APEO, PFOA, PFOS, or formaldehyde, and is compatible with both C6 and fluorine-free systems, making it a practical add-on when a finish needs to withstand 20 or more industrial or home wash cycles. Breathability and Hand Feel Both C0 and C6 finishes coat the fiber surface rather than filling the pore spaces between yarns, so breathability is generally preserved at correct application levels. Two factors most often compromise this balance: Overdosing the finish, which can partially block inter-yarn porosity and stiffen the fabric hand Uneven bath concentration, which creates localized high-add zones across the fabric width C0 finishes sometimes require slightly higher application levels to match C6 water repellency, which makes dosing accuracy and bath uniformity especially important for maintaining a soft, breathable result. Global Regulatory Landscape REACH and EU Restrictions The EU regulates PFAS in textiles under REACH Annex XVII. A restriction on PFHxA, the degradation product of C6 chemistry, takes effect in the EU and EEA from 2026, and a broader restriction covering the wider PFAS family is currently under evaluation by the European Chemicals Agency. Buyers and brands sourcing for the EU market should treat C6 as a chemistry under increasing regulatory pressure rather than a long-term safe option, and should monitor ECHA’s PFAS regulatory updates for the latest scope and timelines. US State Regulations Regulation is not limited to the EU. Two US states have already enacted PFAS restrictions specific to textiles and apparel: California AB 1817 bans the manufacture, distribution, and sale of new textile articles containing intentionally added PFAS above 100 ppm total organic fluorine as of January 1, 2025, dropping to 50 ppm from January 1, 2027. Outdoor apparel for severe wet conditions has an extension until January 1, 2028. The full requirements are set out in the official bill text. New York Environmental Conservation Law § 37-0121 prohibits the sale of new apparel

Explore More »

Contact Us for Textile Auxiliaries and Dyes

Contact Skychem Group for more chemical solutions, If you have questions or need more information, please contact us.
We will respond within 24 hours

Get a project quote

Tell us your project requirements, country, and intended application.

Sandy

With years of experience in chemical dyes and textile auxiliaries, I’m dedicated to sharing insights into the latest technologies, sustainable innovations, and market trends.

Recent Articles

Yellow, red, and blue nylon swatches representing a compatible trichromatic acid dye set.

Trichromatic Acid Dye Selection for Consistent Nylon Shades

Table of Contents Understanding Strike Rate Factors Influencing Strike Rate Matching Strike Rates in a Combination The Role of pH in Dye Uptake pH Ranges by Dye Class Controlling pH During Dyeing Trichromatic Selection Principles Choosing Compatible Yellow, Red, Blue Typical Trichromatic Acid Dye Combinations for Nylon Light Shade Trichromatic Combination Deep Shade Trichromatic Combination Migration and Buildup Properties Avoiding Shade Shift Practical Recipe Guidelines Lab Trial Checklist FAQs What causes uneven dyeing with acid dyes on nylon? How does pH control affect reproducibility? What makes a trichromatic combination reliable? Nylon dyeing rewards precision. Acid dyes bond well with polyamide fibers, but shade consistency depends on how closely strike rate, pH, and trichromatic combinations are controlled together. A small mismatch in any one variable can shift a shade off standard, even when the recipe looks correct on paper. This article breaks down the practical factors that keep acid dye combinations compatible on nylon. Understanding Strike Rate Strike rate describes how quickly a dye moves from the bath onto the fiber. On nylon, this speed depends on dye structure, temperature ramp, and the number of available dye sites on the substrate. A dye with a fast strike rate can produce uneven color if it exhausts before the bath fully penetrates the goods, particularly on tightly constructed knits or dense yarns. Factors Influencing Strike Rate Three variables have the greatest effect on how fast a given acid dye takes up on nylon: Molecular size and structure: smaller, more mobile molecules tend to migrate and level more readily, while larger or more linear structures strike faster but migrate less once fixed. Electrolyte concentration: higher salt levels in the bath slow strike by increasing ionic competition at the fiber surface, which can help leveling but may reduce total exhaustion if not balanced correctly. Temperature ramp speed: a ramp that heats too quickly gives the dye little time to migrate before fixation, raising the risk of streaks or tailing on the goods. Matching Strike Rates in a Combination When combining dyes for a shade, each component should have a comparable strike rate. If one dye in a mix strikes noticeably faster than the others, it dominates the early stages of dyeing and shifts the shade as the bath progresses. This is one of the most common causes of reproducibility problems in nylon dyehouses, especially when recipes are adjusted without checking how the new combination behaves as a system rather than as individual dyes. The Role of pH in Dye Uptake Acid dyes require an acidic bath to bond effectively with the amine groups on nylon fiber. pH does more than set the chemical environment; it also governs how fast dye uptake occurs and how much correction is possible once dyeing has started. pH Ranges by Dye Class Different acid dye classes are formulated to perform within specific pH windows. Working outside that window changes uptake speed and can affect fastness properties. Dye Class Typical pH Range Uptake Behavior Leveling acid dyes pH 5 to 6 Slower strike, good migration, easier to correct Milling acid dyes pH 4.5 to 5.5 Moderate strike, less forgiving on unlevel dyeing Metal complex acid dyes pH 4 to 5 Faster strike, stronger fastness, tighter process control needed These ranges are starting references. Actual performance depends on the specific dye grade, liquor ratio, and machine type, so lab confirmation on the intended substrate remains necessary before scaling to bulk. Controlling pH During Dyeing Holding pH steady throughout the cycle matters as much as setting the correct starting point. A pH that drifts upward during dyeing slows uptake and can leave the shade pale or uneven, while a sharp early drop can cause the dye to strike too fast for proper migration. Buffering systems and controlled acid addition keep the bath within range from start to finish. Leveling agents and buffering auxiliaries formulated for pH and strike control help stabilize uptake speed across different fabric constructions and machine conditions, particularly on constructions prone to rapid initial strike. Trichromatic Selection Principles Trichromatic dyeing uses a yellow, red, and blue dye to build a wide range of shades from a small working palette. Compatibility across these three dyes determines how predictable the resulting shades will be, both in the lab and in bulk. Choosing Compatible Yellow, Red, Blue A workable trichromatic set should share similar strike rates, similar pH sensitivity, and comparable migration behavior. Mismatched components can produce shade drift between lab dips and production batches, even when the total dye concentration is correct. The Skyacido Acid Dyes, formulated specifically for polyamide dyeing, offers a wide shade gamut with strong inter-shade combinability, which supports matching yellow, red, and blue components as a coordinated set rather than selecting each color independently based on shade alone. The table below outlines what to check across each primary when building a trichromatic set: Component Strike Rate Check pH Sensitivity Migration Behavior Yellow Compare exhaustion curve against red and blue Note shift point where uptake accelerates Confirm redistribution at hold temperature Red Compare exhaustion curve against yellow and blue Note shift point where uptake accelerates Confirm redistribution at hold temperature Blue Compare exhaustion curve against yellow and red Note shift point where uptake accelerates Confirm redistribution at hold temperature Running this comparison during lab dip development, rather than after a bulk batch shows shade drift, catches mismatches while they are still inexpensive to correct. Typical Trichromatic Acid Dye Combinations for Nylon In practical nylon dyeing, trichromatic combinations are usually selected according to shade depth, buildup requirement, and compatibility between dyes. Different combinations may be required for light shades and deep shades to maintain balanced exhaustion, migration, and shade reproducibility. Light Shade Trichromatic Combination For light and medium shades, dyes with good migration performance and moderate strike behavior are preferred to achieve excellent leveling and shade correction ability. A typical light shade combination may include: Trichromatic Position Example Acid Dye Yellow Skyacido Yellow 199 Red Skyacido Red 337 Blue Skyacido Blue 324 This combination provides good compatibility and is

Explore More »
2. Low-temperature soaping leaves clearer wash liquor and less staining on adjacent white cotton strips.

Reactive Dye Soaping Guide: Better Wash Fastness, Less Back-Staining

Table of Contents What Is Reactive Dye Soaping Role in the Wash-Off Stage Why Unfixed and Hydrolyzed Dye Must Be Removed How Soaping Affects Wash Fastness Removing Hydrolyzed Dye from the Fiber Surface Connection Between Soaping and Fastness Ratings What Causes Back-Staining? Common Sources of Back-Staining Fabrics and Blends Most at Risk Key Process Parameters for Effective Soaping Temperature and Time Liquor Ratio Water Hardness and Sequestering Agents Choosing the Right Soaping Agents Anionic and Nonionic Soaping Agents Matching Agents to Fiber and Shade Depth Low-Temperature Soaping Agent Option: Sylic D2705 Key Benefits Recommended Application Performance Comparison Soaping Process Methods Cold Wash and Hot Wash Sequence One-Bath vs Multi-Step Soaping Role of Fixing Agents After Soaping Best Practices for Consistent Wash Fastness Results FAQs How long should reactive dye soaping take? Can back-staining be fixed after it happens? Does hard water affect soaping performance? Is a separate fixing agent always necessary after soaping? Reactive dye soaping is often treated as a quick step at the end of the dyeing cycle, but it has a direct effect on wash fastness and back-staining outcomes. Getting temperature, time, and agent selection right prevents costly rejects and repeat orders that eat into margins. What Is Reactive Dye Soaping Role in the Wash-Off Stage Soaping takes place after fixation, once the reactive dye has bonded to the fiber under alkaline conditions. Fabric is washed at or near boiling temperature with a detergent or specialty soaping agent to strip away everything that never formed a permanent bond with the fiber. Skipping or shortening this step leaves wash-off incomplete, and the fabric carries a hidden fastness risk that will not surface until later testing or, worse, after it reaches the customer. Why Unfixed and Hydrolyzed Dye Must Be Removed A portion of reactive dye always hydrolyzes in the dyebath instead of reacting with the fiber. Hydrolyzed dye sits loosely on the fabric surface, held only by weak physical attraction rather than a covalent bond. Left in place, it rubs off during handling, bleeds during laundering, and transfers onto lighter fabrics in the same wash load. Soaping is the step designed specifically to remove this residue before it becomes a fastness problem. How Soaping Affects Wash Fastness The quality of soaping determines much of what shows up later in fastness testing. A batch that looks correct on the shade card can still fail to wash or rub fastness if this step was rushed. Removing Hydrolyzed Dye from the Fiber Surface Effective soaping keeps loosened dye suspended in the wash liquor instead of letting it settle back onto the fabric. How completely this happens depends on agitation, liquor ratio, and the dispersing strength of the detergent or soaping agent used. Connection Between Soaping and Fastness Ratings Wash and rub fastness ratings, most commonly evaluated using AATCC colorfastness test methods, largely reflect how much unfixed dye remains after wash-off. A fabric can pass an initial shade check on the lab dip and still fail fastness testing on the bulk batch if soaping ran too briefly or at too low a temperature. What Causes Back-Staining? Common Sources of Back-Staining Back-staining happens when dye that has washed off the dyed fabric redeposits onto undyed or lighter areas in the same bath. The most common causes include: Overloaded soaping baths carrying more hydrolyzed dye than the liquor can hold Insufficient rinsing between soaping and finishing steps Soaping agents with weak dispersing power, which allow free dye particles to settle back onto the fabric Uneven liquor circulation, which creates localized zones of high dye concentration Fabrics and Blends Most at Risk Deep and dark shades generate the highest load of hydrolyzed dye and are the most frequent source of back-staining complaints. Blended fabrics, and any load that mixes dyed and undyed components, are particularly vulnerable, since redeposited dye is far more visible on the lighter portion of the fabric. Key Process Parameters for Effective Soaping Most causes of poor fastness and back-staining trace back to how tightly these three parameters are controlled. Temperature and Time Soaping typically runs at or close to boiling point for five to fifteen minutes, though the ideal combination depends on shade depth and fabric construction. Running the bath too cool slows dye removal, and cutting the time short leaves hydrolyzed dye behind even at the correct temperature. Shade depth Soaping temperature Typical time Light to medium 90 to 95°C 5 to 8 minutes Deep and dark Near boiling (98 to 100°C) 10 to 15 minutes Turquoise and problem shades Near boiling, multi-bath 15 minutes or more per bath This near-boiling range applies to conventional soaping agents. Low-temperature soaping agents are formulated to work effectively at 60 to 80°C instead, cutting energy use without giving up fastness performance (see the Sylic D2705 section below).  Liquor Ratio A tighter liquor ratio concentrates hydrolyzed dye in a smaller volume of water, which increases the risk of redeposition before it can be flushed out. Mills running jet or overflow machines at lower liquor ratios should compensate with stronger dispersing agents or an added rinse cycle. Water Hardness and Sequestering Agents Calcium, magnesium, and iron in the water supply interfere with soaping agent performance and can leave a hazy or uneven finish. A sequestering agent, such as Sylic P1501B, an anionic chelating dispersant with a pH of 2.5 to 4.0 in a 1% solution, binds these ions before soaping begins and lets the soaping agent perform as intended. Choosing the Right Soaping Agents Anionic and Nonionic Soaping Agents Anionic soaping agents are widely used for their strong dispersing action, while nonionic types perform better in hard water and at lower temperatures. Both types are available within a dyeing auxiliary range formulated for stability in alkaline baths and low-foam performance in jet machines. Matching Agents to Fiber and Shade Depth Cotton and other cellulosic fibers generally respond well to anionic soaping agents. Blends containing synthetic fibers may need a nonionic option instead, to avoid staining the more sensitive synthetic component. Deeper shades typically call

Explore More »

Reduction Clearing in Polyester Dyeing: A Complete Guide

Table of Contents What Is Reduction Clearing? Definition and Purpose Role in Disperse Dyeing Impact on Colorfastness Common Quality Complaints When Reduction Clearing Is Needed Dark and Medium Shades High Dye Concentration Recipes Blends with Cellulosic Fibers When It Can Be Skipped Process and Control Typical Recipe and Parameters Controlling Temperature and pH Avoiding Over-Reduction or Under-Reduction Rinsing and Neutralization Choosing the Right Reducing Agents Sodium Hydrosulfite Sulfur-Free Reducing Agents Low-Temperature and Sustainable Options High Wash Fastness Dyes to Reduce Clearing Load Troubleshooting Common Issues Poor Wash Fastness After Clearing Shade Change or Dulling Conclusion FAQs What Happens If You Skip It? Reduction Clearing vs Normal Washing? Can It Be Done at Low Temperature? Hydrosulfite vs Sulfur-Free Agents? A batch that looks perfect on the machine can still fail a wash fastness test days later. More often than not, the cause is unfixed disperse dye left on the fiber surface, and the fix is reduction clearing. This guide covers when the step is necessary, the chemistry behind it, and how to keep results consistent from lab dip to bulk production. What Is Reduction Clearing? Definition and Purpose Reduction clearing is a post-dyeing treatment that removes disperse dye which has not penetrated or fixed onto polyester fibers. During high temperature dyeing, some dye molecules remain on the fiber surface instead of diffusing into the polymer structure. Left untreated, this residual dye rubs off and bleeds during washing, lowering overall color fastness. A reduction clearing bath breaks down and strips away the surface dye, leaving only the dye that has properly fixed inside the fiber. Role in Disperse Dyeing Reduction clearing takes place at the end of the disperse dyeing cycle, after the main dyeing stage and before final rinsing. It is one part of a larger polyester dyeing workflow that also includes pretreatment, dyeing, and finishing. The polyester dyeing application solutions page outlines how these stages connect, along with recommended auxiliaries for each step. Impact on Colorfastness Wash and rub fastness are among the specifications buyers check most closely before accepting a shipment. Surface dye that has not been cleared is loosely bound and washes out easily, which is precisely what standardized tests such as AATCC’s laundering fastness methods are designed to detect. A properly executed reduction clearing step improves these results by removing the dye that would otherwise cause a failed test. Common Quality Complaints Mills that skip or under-perform reduction clearing tend to see a recurring pattern of issues: Color bleeding onto lighter garments in the same wash load Staining on packaging or trims during transport and storage Dull or hazy shades compared to the approved lab dip Rejected shipments after failed fastness testing at the buyer’s lab These problems are almost always traceable to residual disperse dye rather than a flaw in the dye recipe itself, which is why reduction clearing deserves the same attention as the dyeing stage it follows. When Reduction Clearing Is Needed Dark and Medium Shades Darker and medium depth shades require higher dye concentrations, which naturally leaves more unfixed dye on the fiber surface. The Skycron disperse dyes range covers both dyeing and printing applications across dark, medium, and vivid shades, and pairing these dyes with a proper reduction clearing step is standard practice for reaching acceptable fastness at these heavier depths. High Dye Concentration Recipes Any recipe with a high total dye percentage on weight of fabric (% o.w.f.) benefits from reduction clearing, not only dark shades. As a general reference, mills commonly group shade depth this way: Shade Depth Typical Dye Concentration Reduction Clearing Light Below 1% o.w.f. Often optional Medium 1 to 3% o.w.f. Recommended Dark Above 3% o.w.f. Required These figures are a general guide rather than a fixed rule, since dye class, fiber blend, and fastness targets all shift the threshold. Multi-dye combinations used for precise custom shades fall into this same logic, as several dye classes combined can leave behind varying amounts of surface residue even at a moderate total percentage. Blends with Cellulosic Fibers Polyester-cotton and polyester-viscose blends add another layer of risk. Disperse dye that has not fixed to the polyester portion can stain the cellulosic fiber, causing an unwanted tone shift across the fabric. Reduction clearing protects the intended contrast or solid shade across both fiber types. When It Can Be Skipped Very light shades with low dye loading sometimes do not require a full reduction clearing cycle, particularly when high-exhaustion dyes and well-controlled dyeing conditions are used, and a simple hot wash can be enough. Skipping the step should still be a deliberate decision based on shade depth and fastness requirements, not a shortcut taken to save time. Process and Control Typical Recipe and Parameters A standard alkaline reduction clearing bath includes a reducing agent, caustic soda or soda ash, and a wetting or dispersing agent. Sulfur-free acid-clearing systems, which run at a lower pH, are increasingly used as an alternative. A general starting point looks like this: Parameter Typical Range Reducing agent 2 to 4 g/L Alkali (NaOH or soda ash) 2 to 4 g/L Temperature 70 to 80°C Time 15 to 20 minutes Liquor ratio 1:8 to 1:15 These figures vary by shade depth, dye class, and fiber blend, so lab trials should confirm the final recipe before scaling to bulk. Controlling Temperature and pH Temperature and pH are the two variables that most affect clearing efficiency: Too cool or too brief: residual dye is left behind, and fastness suffers. Too hot or too alkaline: the polyester surface or hand feel can be affected. Most conventional recipes target a mildly alkaline pH between 9 and 11. Acid-based sulfur-free systems instead work in a neutral to mildly acidic range, depending on the product used, so the pH target should always match the chemistry selected rather than a single fixed rule. Avoiding Over-Reduction or Under-Reduction Under-reduction leaves surface dye behind, which shows up later as poor fastness. Over-reduction strips properly fixed dye from the fiber, causing shade loss, dulling, or an uneven

Explore More »
C0 vs. C6 Water Repellent Finishes

C0 vs. C6 Water Repellent Finishes: Which One Fits Your Textiles?

Table of Contents The Chemistry Behind C0 and C6 What is C6 DWR What is C0 DWR Key Structural Differences Performance Comparison Water and Oil Repellency Durability and Wash Resistance Breathability and Hand Feel Global Regulatory Landscape REACH and EU Restrictions US State Regulations Brand and Retailer Requirements Use Cases by Industry Outdoor and Sportswear Workwear and Protective Textiles Home Textiles and Upholstery Choosing the Right Finish Key Factors to Consider Testing and Certification Tips Conclusion FAQs What is the difference between C0 and C6 finishes? Is C6 DWR banned? Does C0 perform as well as C6? How do I choose between C0 and C6? Ask a fabric supplier for a water-repellent finish today, and there is a good chance you will get two very different answers: C6, or C0. Both claim to keep fabric dry. Only one is currently facing phase-out pressure from regulators in the EU, California, and New York, and from major apparel brands. For buyers sourcing water-repellent textiles right now, the choice is no longer just about performance. It is about which chemistry will still be sellable in your target market two years from now. The Chemistry Behind C0 and C6 What is C6 DWR C6 durable water repellent (DWR) finishes use short-chain fluorocarbon polymers, specifically six-carbon fluorinated side chains, to coat individual fibers. This chemistry lowers the surface energy of the fiber to roughly 12 mJ/m², which is below the surface tension of most water and oils. As a result, C6 finishes deliver both water and oil repellency, a combination that few fluorine-free systems can fully match. C6 chemistry replaced older C8 fluorotelomer finishes over a decade ago. C8 degrades into PFOA, a substance known for being persistent and bioaccumulative in the environment. C6 degrades into perfluorohexanoic acid (PFHxA) instead, which has a shorter environmental half-life and lower bioaccumulation potential. However, PFHxA is not free of regulatory scrutiny, as covered in the compliance section below. For buyers sourcing C6 products, formulations such as the Skyguard C6-C8 Waterproofer combine water and oil resistance with good wash fastness on both cellulose and synthetic fibers, applied at typical dosages of 10 to 40 g/L, and are produced without PFOS, PFOA, or APEO. What is C0 DWR C0 refers to fluorine-free water repellent chemistry. Instead of fluorocarbon side chains, C0 finishes rely on dendrimer, wax, or polyurethane-based polymers to build a hydrophobic fiber surface. These systems typically reach a surface energy of 20 to 25 mJ/m², which is sufficient to repel water effectively but generally not enough to provide strong oil repellency. Demand for C0 finishes is growing quickly because they carry no PFAS-related compliance risk, a factor that matters more each year as regulatory scope widens. Ranges such as the Skyguard Fluorine-free Waterproofer line are applied at roughly 10 to 80 g/L depending on the durability required, contain no APEO, and are built for fabrics where oil repellency is not a functional requirement, including most outerwear, home textiles, and fashion applications. Key Structural Differences Attribute C6 (Fluorocarbon) C0 (Fluorine-Free) Surface energy Approx. 12 mJ/m² Approx. 20 to 25 mJ/m² Water repellency Excellent Good to excellent Oil repellency Yes Limited or none PFAS content Present (PFHxA-based) None Typical curing temperature 150 to 160°C 160 to 180°C Performance Comparison Water and Oil Repellency C6 finishes remain the benchmark wherever oil, grease, or organic stain resistance is needed alongside water repellency, such as workwear exposed to machine oils or food-contact aprons. C0 finishes have closed most of the gap on pure water repellency, with many recent formulations achieving results comparable to C6 under standardized water resistance testing. On oil-based stains, however, C0 finishes still fall short. Durability and Wash Resistance Both chemistries rely on physical adsorption when first applied to the fabric, and this bond weakens progressively with repeated laundering and detergent exposure. A crosslinking agent extends wash durability by binding DWR polymer chains to each other and to reactive groups on the fiber surface, converting a loosely adsorbed coating into a chemically anchored one. The Sylic Cross-linking Agent, for example, is dosed in the same bath at 10 to 30 percent of the water repellent quantity, contains no APEO, PFOA, PFOS, or formaldehyde, and is compatible with both C6 and fluorine-free systems, making it a practical add-on when a finish needs to withstand 20 or more industrial or home wash cycles. Breathability and Hand Feel Both C0 and C6 finishes coat the fiber surface rather than filling the pore spaces between yarns, so breathability is generally preserved at correct application levels. Two factors most often compromise this balance: Overdosing the finish, which can partially block inter-yarn porosity and stiffen the fabric hand Uneven bath concentration, which creates localized high-add zones across the fabric width C0 finishes sometimes require slightly higher application levels to match C6 water repellency, which makes dosing accuracy and bath uniformity especially important for maintaining a soft, breathable result. Global Regulatory Landscape REACH and EU Restrictions The EU regulates PFAS in textiles under REACH Annex XVII. A restriction on PFHxA, the degradation product of C6 chemistry, takes effect in the EU and EEA from 2026, and a broader restriction covering the wider PFAS family is currently under evaluation by the European Chemicals Agency. Buyers and brands sourcing for the EU market should treat C6 as a chemistry under increasing regulatory pressure rather than a long-term safe option, and should monitor ECHA’s PFAS regulatory updates for the latest scope and timelines. US State Regulations Regulation is not limited to the EU. Two US states have already enacted PFAS restrictions specific to textiles and apparel: California AB 1817 bans the manufacture, distribution, and sale of new textile articles containing intentionally added PFAS above 100 ppm total organic fluorine as of January 1, 2025, dropping to 50 ppm from January 1, 2027. Outdoor apparel for severe wet conditions has an extension until January 1, 2028. The full requirements are set out in the official bill text. New York Environmental Conservation Law § 37-0121 prohibits the sale of new apparel

Explore More »

Contact Us for Textile Auxiliaries and Dyes

Contact Skychem Group for more chemical solutions, If you have questions or need more information, please contact us.
We will respond within 24 hours

Get a project quote

Please tell us the requirements, the country and the application.

Scroll to Top
Email WhatsApp

Contact Us for Textile Auxiliaries and Dyes

Contact Skychem Group for more chemical solutions, If you have questions or need more information, please contact us.
We will respond within 24 hours