...

Contact Skychem Group for more chemical solutions, If you have questions or need more information, please contact us.
Respond within 24 hours

Dispersing Agents in Textile Dyeing: Selection, Dosage, and Compatibility

A polyester dyeing batch may look uniform at the start of a cycle, then develop specks as the temperature rises. Disperse dye particles can aggregate and settle on the fabric or equipment. A suitable dispersing agent helps maintain a stable dyebath, but its performance depends on the dyes, water, equipment, and other chemicals in the recipe.

What Dispersing Agents Do

Disperse dyes are only slightly soluble in water. In the dyebath, fine dye particles act as a reservoir: dye dissolves from their surfaces and moves into polyester fibers. The remaining particles need to stay evenly distributed as the bath heats and dyeing proceeds. A dispersing agent helps limit particle aggregation, reducing the risk of specks, uneven shades, and deposits.

Dispersing, wetting, and leveling agents address related but distinct needs:

  • Dispersing agents help keep insoluble dye particles suspended.
  • Wetting agents help the liquor contact and penetrate the fabric.
  • Leveling agents help control uneven dye uptake or promote dye migration.

Some auxiliaries combine these functions. Assess the claimed function under production conditions rather than relying on the product name alone.

Sky-blue polyester swatches prepared for shade comparison.

How to Select an Agent

Start with the dye formulation and shade depth. Commercial disperse dyes may already contain dispersing ingredients, and a blend may respond differently from a single-dye bath. If the recipe uses Skycron disperse dyes, test the specific shades and concentrations planned for production.

Next, check the conditions the agent must tolerate:

Factor What to verify
Temperature The dispersion remains stable during heating, holding, and cooling.
Bath chemistry Performance holds at the target pH and in the mill’s water.
Equipment Foam is manageable, with no troublesome filter or machine deposits.
Dyed fabric Shade and levelness match the approved standard across repeat trials.

Compare candidates under the same dyeing conditions. Sylic D2150 Dispersing Agent (NNO) is one relevant example: its product page lists a water-soluble, anionic powder intended for high-temperature use with disperse dyes, including Skycron TXF, KXF, and SWF series. The stated pH of 6.5–8.5 is measured in a 1% aqueous solution. It does not establish an operating pH range for every dyebath. Because D2150 is anionic, check compatibility with other auxiliaries, especially cationic products.

For purchasing, compare the cost of successful batches, including any rework or cleaning.

How to Set the Dosage

First, confirm the unit used in the supplier’s recipe. g/L is grams of product per liter of dyebath. % owf is product weight as a percentage of dry fabric weight. The two units are not interchangeable without knowing the bath volume and fabric weight.

For example, 1 g/L in a 1,000 L bath requires 1 kg of product. A dose of 1% owf for 100 kg of fabric also requires 1 kg, but the equal amounts in this example are coincidental. Changing the liquor ratio changes the bath volume and the g/L calculation, while the % owf calculation remains tied to fabric weight.

Use the product’s recommended range to design a lab trial. The D2150 page lists 1–2 g/L in a sample recipe that also includes Sylic D2118, acetic acid, and disperse dyes. Treat this as a recipe-specific starting point, not a general dose or a guarantee that these ingredients suit every bath.

Run trials at the intended shade depth, liquor ratio, pH, and temperature profile. Compare the proposed doses with a control, and record:

  • Bath stability during and after heating
  • Filter residue and visible dye specks
  • Foam and equipment deposits
  • Shade difference and levelness on the dyed fabric

An insufficient dose may fail to control aggregation. An excessive dose adds cost and can change dyeing behavior, so choose the lowest tested dose that meets the process requirements consistently.

Small sky-blue dye baths prepared for a dosage trial.

How to Check Compatibility

A dispersing agent must perform in the complete dyebath, not only in a beaker of dye and clean water. Include the planned dye blend, leveling agent, buffer, wetting agent, defoamer, and any other chemicals used during dyeing. The polyester dyeing auxiliaries page identifies other products used in polyester processing. Check the intended stage and chemistry of each one before combining them in a bath.

Reproduce the production addition order and concentrations with the mill’s water. Follow the intended pH and heating cycle, then inspect the bath before heating, at dyeing temperature, and after cooling. Look for flocculation, settling, excessive foam, and deposits. Filter a measured liquor sample when residue is a concern, and compare the dyed fabric with the approved shade standard.

If a trial fails, change one variable at a time to isolate the cause. Repeat a promising trial before approving the bulk recipe.

Sky-blue dyebath residue inspected during filtration.

FAQ

Do commercial disperse dyes already contain dispersants?

Many do. Check the dye supplier’s guidance, then compare trials with and without an additional agent to see whether it improves stability under production conditions.

What is the difference between a dispersing agent and a leveling agent?

A dispersing agent helps keep dye particles distributed in the liquor. A leveling agent helps achieve an even shade by influencing dye uptake or migration. One product may perform both functions, but they are separate performance goals.

How much dispersing agent should I use for polyester dyeing?

Use the specific product’s recommended range as the starting point. Confirm its unit, then select a dose from trials run under production conditions.

Can excess dispersing agent affect the final shade?

Yes, depending on the dye and auxiliary system. A higher dose may change dyeing behavior even if the bath appears stable. Compare dyed samples and measured shade differences before increasing the production dose.

How do I test compatibility with other dyeing auxiliaries?

Use the complete recipe and the intended addition order in a small-scale dyeing trial. Compare bath stability, residue, shade, and levelness with a control.

Sandy

With years of experience in chemical dyes and textile auxiliaries, I’m dedicated to sharing insights into the latest technologies, sustainable innovations, and market trends.

Recent Articles

An iodine drop is applied to a woven cotton sample.

Textile Desizing: Methods, Recipes, and Efficiency Control

Table of Contents What Is Desizing? Choose a Method by Size Type Desizing Enzymes and Chemicals Amylase for starch Wetting agents for liquor penetration Oxidative treatment for selected sizes Practical Desizing Recipes Enzymatic pad-batch Enzymatic exhaust Hot washing Oxidative treatment Measure Desizing Efficiency Select a Desizing Agent FAQ Which enzyme is used for textile desizing? Can amylase remove synthetic sizes? What is the difference between enzymatic and oxidative desizing? How is desizing efficiency tested? Why does fabric still absorb water poorly after desizing? How do I choose a desizing recipe for my mill? Warp size protects yarn during weaving. After weaving, that same coating must be removed so water and processing chemicals can reach the fabric evenly. A reliable desizing process begins with the size formulation, then moves through treatment, washing, and verification. What Is Desizing? Desizing removes the coating applied to warp yarns before weaving. It is an early preparation step for woven fabric headed to dyeing, printing, or finishing. Desizing targets applied size. Scouring removes impurities such as oils and natural waxes, while bleaching removes natural color. The steps may run separately or together, but a good result in one does not prove the others are complete. For more on their effect downstream, see how pretreatment affects fabric quality and color fastness. Choose a Method by Size Type Ask the weaving mill or yarn supplier which sizes were applied. If the formulation is unknown, test a representative sample before choosing the treatment. Size type Starting approach Main verification Starch or modified starch Amylase treatment followed by washing Residual starch Water soluble synthetic size Controlled hot washing Removal after the final rinse Mixed or difficult to remove size Trials with suitable washing and chemical treatment Removal of each component without unacceptable fabric damage These approaches are starting points. The fiber blend, size formulation, and equipment determine the final process. Desizing Enzymes and Chemicals Amylase for starch α-Amylase breaks starch into smaller, water soluble fragments that can be washed away. The enzyme must reach the size and remain active under the bath conditions. For a product-specific trial, Sylic B6141 Amylase (CY-15A) is identified as an α-amylase for textile desizing. Its product information describes compatibility with commonly used desizing wetting agents, and the pretreatment listing gives 1 g/L as a reference dosage. Confirm the working pH, temperature, and treatment time for the intended equipment before using that figure in a production recipe. Wetting agents for liquor penetration A wetting agent can improve contact between the treatment liquor and the sized fabric. Sylic P1400 Wetting Agent is listed for pretreatment of natural fibers, synthetic fibers, and blends. Its stated reference dosages are 0.5–2 g/L for intermittent processing and 2–6 g/L for continuous processing. These are product application ranges, not a confirmed recipe with any particular amylase; check bath compatibility in a trial. Oxidative treatment for selected sizes An oxidative route may be considered when washing or enzyme treatment does not adequately remove the known size. Test the proposed chemistry on the actual fabric. Size removal, strength, and appearance all matter when deciding whether to scale it up. Practical Desizing Recipes A usable recipe specifies treatment and wash-off. Set initial chemical conditions from the selected products’ technical data sheets, then validate them on production fabric. Enzymatic pad-batch Prepare a compatible enzyme bath, pad the fabric at a consistent pickup, and hold it for the validated dwell time. Wash out the degraded size afterward. Compare liquor pickup and residual starch at the center and edges of the fabric. Enzymatic exhaust Add the enzyme and any compatible auxiliaries under the recommended bath conditions. Record the liquor ratio, actual treatment temperature, and time held at that temperature. Drain and wash the fabric before testing it. Hot washing For a confirmed water soluble size, trial a wash sequence with adequate heat, liquor movement, and rinsing. Check the fabric after the final rinse, since dissolving size in the bath does not guarantee its removal from the cloth. Oxidative treatment Choose the chemical system for the known size and fiber blend. Begin with a small trial and check fabric strength and appearance alongside size removal. For each trial, record the size formulation, fabric, products, dosages, pH, temperature, time, liquor ratio or pickup, wash sequence, and test results. This makes the result reproducible across shifts and machines. Measure Desizing Efficiency For starch sized fabric, an iodine test can reveal residual starch. A TEGEWA rating can be used to record and compare the result. Sample the center and edges of the fabric at more than one point in the run. An iodine result does not establish whether synthetic size has been removed. Use an assessment suited to the known formulation, then check that the fabric meets the absorbency requirements of its next process. When results are incomplete or uneven, check four points in sequence: Size formulation: Does the treatment address every component? Bath conditions: Were concentration, pH, temperature, and time controlled? Penetration: Did liquor reach the full fabric width evenly? Wash-off: Were dissolved or degraded materials rinsed away? If starch removal is satisfactory but absorbency remains poor, investigate oils, waxes, and scouring performance before increasing the enzyme dose. Select a Desizing Agent Share the size formulation, fiber blend, machine type, available temperature range, and current defect when requesting a product recommendation. Compare candidates on the same fabric under defined trial conditions. Judge the result by residual size, absorbency, uniformity, fabric quality, washing demand, and total process cost. A lower chemical dose is not an improvement if it increases rinsing or rework. FAQ Which enzyme is used for textile desizing? α-Amylase is commonly used for starch based size. Select a product whose operating conditions suit the fabric and equipment. Can amylase remove synthetic sizes? Do not assume that it can. Identify the synthetic size and test a suitable washing or chemical treatment. What is the difference between enzymatic and oxidative desizing? Enzymatic desizing uses an enzyme to break down its target size, such as starch in an amylase process. Oxidative desizing

Explore More »
Light printed pattern on dark cotton fabric

Discharge Printing in Textiles: Process, Chemicals, and Problems

Table of Contents How Discharge Printing Works Fabrics and Dyes White and Color Discharge Chemicals and Auxiliaries Production Process Common Problems and Fixes FAQs Which dyes are suitable for discharge printing? Why does a white discharge print look yellow or pink? Can polyester or blended fabrics be discharge printed? What causes incomplete discharge? What should buyers test before bulk production? Discharge printing creates a pattern by chemically changing the dye in selected areas of an already dyed fabric. A printer applies a discharge paste, fixes the print under conditions suited to the dye and fiber, and washes away removable residues. The result is a lighter pattern or a newly colored one against the original ground shade. The method can produce crisp, light motifs on dark fabric without the heavy surface layer of an opaque overprint. Its main limitation is predictability: a recipe that gives a clean white on one ground shade may leave a pink or yellow cast on another. The ground dye and the finished trial print must therefore be evaluated together. How Discharge Printing Works The fabric is first dyed to its ground shade. A print paste containing a discharging agent is applied only where the design should appear. During fixation, the agent changes susceptible dye molecules in those areas. Most of the methods discussed here use a reducing agent, although other discharge routes exist. The required wash-off removes paste residues and dye reaction products that can be washed away. Ordinary overprinting places color over the existing shade. Resist printing prevents a ground color from developing in selected areas. Discharge printing starts with a colored fabric and changes the shade afterward. In a mixed black or navy, one dye component may resist treatment and leave a visible undertone. This is why the full ground-shade recipe matters more than the color name. Fabrics and Dyes Cotton and other cellulosic fabrics are common substrates. Selected reactive, direct, and azoic dyes can provide a dischargeable ground. Vinyl sulfone reactive dyes are used in established cotton discharge processes, although performance depends on the individual dye and shade mixture. The reactive dyes for cellulosic fabrics page identifies the Skyzol General Series as containing vinyl sulfone (KN type) and vinyl sulfone/monochlorotriazine (M type) dyes. This identifies chemistry worth screening, not a discharge rating. Request results for the exact shades before selecting a ground recipe. Polyester, wool, silk, and blends require different dye and fixation choices. Polyester processes may call for selected disperse dyes and different fixation conditions from those used on cotton. Wool and silk require close attention to fiber strength and handle. On a blend, the components may discharge differently, making an even white difficult to achieve. White and Color Discharge White discharge changes the ground shade without adding an illuminating colorant. The finished area may look white, cream, or faintly tinted, depending on the fabric and residual dye color. A white pigment may be included for greater opacity in some systems, but the ground still needs to discharge effectively. Color discharge changes the ground shade while introducing an illuminating dye or pigment in the printed area. In a suitable cotton process, selected vat dyes for cotton can serve as illuminating dyes. The product range does not specify which dyes work in discharge paste, so selection must account for paste stability, shade development, oxidation, and final fastness. White discharge makes residual ground color particularly visible. Color discharge adds the challenge of developing the new shade consistently across the run. Chemicals and Auxiliaries The discharging agent is the active component of the paste. Sodium formaldehyde sulfoxylate is widely used in cellulosic discharge processes. Zinc formaldehyde sulfoxylate is another option, including in some synthetic-fiber systems. Thiourea dioxide can be used in selected processes but requires appropriate conditions and paste stability. These agents are not interchangeable: compare discharge quality and fabric strength under the intended fixation conditions. The other paste ingredients control application and appearance. A compatible thickener helps hold sharp edges without blocking the screen. Wetting agents and humectants may be used to adjust penetration and moisture retention. In color discharge, a pigment formulation may need a binder for adhesion. Check the whole mixture for changes in viscosity, separation, or particles that could block the screen. The textile printing auxiliaries page gives useful screening details. Sylic PR4200 is an anionic thickener listed for reactive printing on cotton and linen, with electrolyte resistance and a 3% reference dosage. Sylic PR4223 is listed for roller and screen printing, with water-holding and electrolyte-resistance properties and a 1.5–2% reference dosage. These figures describe the listed printing applications, not validated discharge-paste dosages. Check each candidate’s stability with the chosen reducing agent before using it. For the broader functions of these ingredients, see thickeners, binders, and fixers in textile printing. For product selection, specify fiber content, the ground-dye recipe, print method, fixation equipment, target shade, and fastness requirements. Request technical and safety documentation. If the formulation uses a formaldehyde sulfoxylate, include customer limits on residual formaldehyde in the finished-fabric test plan. Production Process Prepare the ground fabric. Dye and wash it consistently. Confirm that pretreatment residues and shade variation will not affect the print. Test dischargeability. Print small samples of the actual ground fabric. Judge the result after full fixation and washing, not while the print is still wet. Prepare the paste. Follow the supplier’s mixing instructions. Record viscosity, ingredient order, and usable working time; prepare only as much paste as the validated process permits. Print the design. Keep screen condition, paste deposit, pressure, and fabric tension consistent. Monitor fine lines and solid areas separately. Dry and fix. Control temperature, moisture, and dwell time for the chosen fiber and chemistry. Steam and dry heat can produce different discharge effects, so use the route established in the trial. Complete post-treatment. Follow the formulation’s specified oxidation, rinsing, and wash-off sequence where applicable, then dry and finish the fabric. Insufficient washing can leave residues or a dull print. Approve the bulk standard. Compare the finished sample with the target for ground shade, print

Explore More »
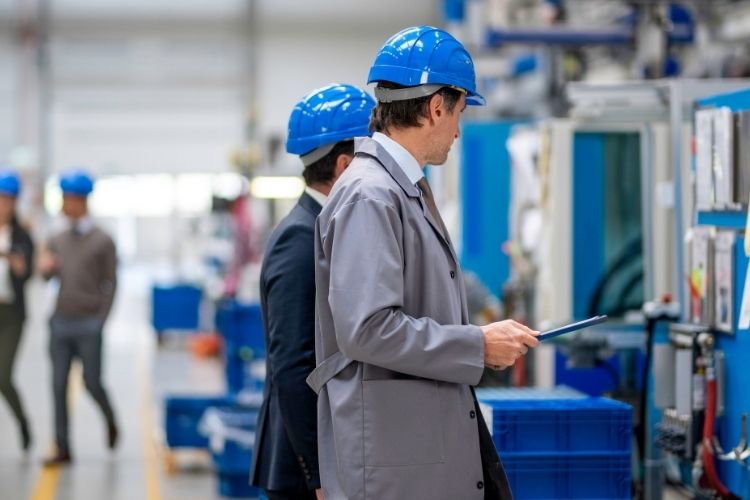
Two professionals discussing production beside factory equipment

How to Choose a Textile Chemical Supplier?

Table of Contents Check Product Quality in Your Process Verify Compliance for the Exact Product Test Batch Consistency and Traceability Evaluate Technical Support During the Trial Compare Total Cost, Then Run a Mill Trial FAQ What documents should a textile chemical supplier provide? How do I test a new dye or auxiliary supplier? How can I check batch-to-batch consistency? Which chemical compliance requirements should I verify? A textile chemical supplier influences what happens on the production floor long after a purchase order is placed. Inconsistent dye strength can force shade corrections. An auxiliary that performs well in a sample test but poorly in the mill can slow production or create rework. Missing compliance documents can delay customer approval. Price matters, but it is only one part of the decision. A sound supplier evaluation asks whether the products work in your process, whether the required evidence is available, whether performance holds across batches, and whether technical help is useful when conditions change. Before requesting samples, define the fiber, machinery, process, target result, and customer requirements. Give each prospective supplier the same information. That makes its recommendations easier to assess and its products easier to compare. Check Product Quality in Your Process Product quality depends on the application. A chemical can meet its published specifications and still be a poor match for your fabric, water, equipment, or recipe. Begin with laboratory tests, then confirm promising results at production scale. For textile dyes, assess the properties that affect the finished order: Shade and strength: Does the dye reach the target shade at the expected dosage? Recipe compatibility: Does it perform consistently alongside the other dyes and chemicals used in the bath? Process behavior: Is the result stable under the mill’s normal temperature profile, pH, and processing time? Fastness: Does the dyed fabric meet the customer’s relevant washing, rubbing, or light fastness requirements? For textile auxiliaries, test the claimed function rather than relying on a general description. A wetting agent should provide suitable penetration and uniformity within the available contact time. A leveling agent should help control uneven dyeing while allowing the target shade to develop. A softener should deliver the required hand feel without causing an unacceptable loss of absorbency or a visible shade change. Product parameters help identify candidates, but their meaning depends on the application. The listed specifications for Sylic F3400 silicone softener include 62–64% solid content and recommended dosages for a diluted emulsion. Those figures help a buyer plan a trial, but they do not establish the right dilution or dosage for every mill. Testing should confirm emulsion preparation, compatibility with the finishing bath, hand feel, and performance at the actual working concentration. Ask for a current technical data sheet and a sample of each shortlisted product. Use the same fabric and controlled conditions for comparative trials. Record both the result and the amount of product required to achieve it. Verify Compliance for the Exact Product Compliance is not a single certificate that covers every purchasing situation. Requirements depend on the formulation, the customer’s specifications, and the markets where the chemical or finished textile will be used or sold. Request a current safety data sheet for the product under consideration. Then identify any additional evidence your customer requires. If ZDHC MRSL conformance is specified, check the status of the particular formulation. The MRSL addresses restricted substances in chemical inputs used during manufacturing. It does not certify that a finished textile meets all customer requirements. A supplier’s published textile chemical certificates can help begin the review. For each document, check: The product name or code it covers The issuing body and scope Its validity period Whether the documented formulation matches the product offered Ask for clarification if a certificate names a product family but the proposed grade is unclear. If the formulation changes later, confirm whether the existing evidence still applies. This check is especially important when approving a substitute for a previously qualified chemical. Test Batch Consistency and Traceability A successful sample test establishes a starting point. It does not prove that future shipments will produce the same result. Ask the supplier which properties it measures before releasing each batch and what limits it accepts. For a dye, relevant checks may include shade and relative strength. For an auxiliary, they may include pH, solid content, and a test tied to its intended function. The appropriate limits should reflect the product and the sensitivity of your process. Every shipment should have an identifiable lot number. Confirm whether the supplier retains samples and can link a delivered lot to its production and quality records. When order volumes justify it, compare results from two or more production lots before relying on the product for a critical program. Agree on a procedure for deviations before they occur. The mill should know what information to provide, such as the lot number, fabric, recipe, process conditions, and test results. The supplier should be able to explain how it will investigate the difference and resolve an out-of-specification delivery. Clear records make it easier to distinguish a chemical variation from a change in the mill’s process. Evaluate Technical Support During the Trial A product recommendation is more useful when it is based on the mill’s operating conditions. Share enough detail for a meaningful answer: fiber content, equipment, water conditions, current recipe, target result, and the problem you are trying to solve. Then assess the response. If the issue is uneven shade, does the supplier ask about pretreatment, dosing, temperature, and bath conditions before suggesting an adjustment? If wetting is slow, does it consider the fabric and available contact time? Good technical support identifies factors to check and proposes a trial that can confirm or rule out a cause. The trial also shows how support works in practice. Confirm who will answer questions after purchase, which test data the supplier can review, and how quickly it can respond across time zones. These details matter when a mill must decide whether to adjust a process or hold production. Compare

Explore More »
Cotton terry compares water absorbency.

Silicone Softener Problems: Causes and Solutions for Yellowing, Spots and Hydrophilicity Loss

Table of Contents Yellowing Issues Common Causes Heat and Curing Effects Prevention Tips Fixing Yellowed Fabric Spots and Uneven Deposits Causes of Spots Emulsion Stability Prevention Techniques Troubleshooting Steps Shade Change After Softening Why Shade Change Happens Dye Compatibility Minimizing Shade Variation Loss of Hydrophilicity Why Absorbency Drops Balancing Softness and Absorbency Hydrophilic Softener Options Best Practices for Application Correct Dosage and Dilution Padding and Drying Parameters Quality Control Testing Conclusion FAQs What causes silicone softener to turn fabric yellow? How can I prevent spots after softener treatment? Why does fabric shade change after softening? How do I restore hydrophilicity after softener use? Silicone softeners are among the most widely used finishing chemicals in textile mills, valued for the smooth hand feel, drape, and durability they bring to fabric. But they can also be a source of real headaches on the production floor. Yellowing on white goods, oily spots after padding, unexpected shade shifts, and a sudden loss of water absorbency are among the most common complaints raised by finishers, dyers, and quality teams worldwide. Nearly every one of these problems traces back to a small number of root causes: the wrong silicone chemistry for the substrate, poor emulsion stability, incorrect bath conditions, or curing parameters pushed past the chemistry’s limits. Once the underlying fiber and polymer behavior is understood, most of these issues can be prevented with a better product choice, a small process adjustment, or tighter quality control at the padding stage. This article walks through each problem in turn, covering what causes it and how to prevent or correct it. Yellowing Issues Yellowing is one of the most commonly reported complaints with silicone softeners, especially on white and pastel fabrics where even a slight color shift is immediately visible. Common Causes Most yellowing traces back to the amine content in the silicone polymer. Amino-modified silicones deliver excellent softness because the amine groups anchor strongly to the fiber surface, but those same groups are chemically reactive and prone to oxidation. A few conditions make the problem worse: Contamination from iron or other transition metals in the bath water Residual chlorine left over from bleaching Low-quality or inconsistent raw materials in the softener itself Heat and Curing Effects Yellowing often becomes visible only after the fabric passes through the stenter. Thermal oxidation of free amine groups during curing generates chromophores, the compounds responsible for the yellow tint, and this effect grows more pronounced as yellowing can become more pronounced when curing temperatures exceed the recommended range for the specific silicone softener and fabric. A second, less obvious mechanism is gas fading, sometimes called NOx yellowing, where atmospheric nitrogen oxides react with amine groups during storage or transport. This can occur without any heat exposure at all, which is why fabric sometimes yellows weeks after it leaves the finishing line, long after the mill has moved on to the next order. Prevention Tips A few adjustments go a long way toward keeping fabric bright: Choose a softener with a lower amine value for light and white goods Keep curing temperature and dwell time within the supplier’s recommended window Use demineralized water to reduce metal ion contamination Add an antioxidant, or switch to a block silicone rather than a straight amino silicone, for goods that will be stored or shipped over long distances Fixing Yellowed Fabric Once yellowing has occurred, options are limited. Mild cases can sometimes be improved with a peroxide or reducing bleach treatment, though this carries some risk to fabric strength and should always be tested on a sample first. In most cases, the more reliable fix is prevention on the next batch rather than correction after the fact, which is why product selection and process control matter so much upfront. Cause Recommended Fix High amine value silicone Switch to a low amine value or block silicone softener Excess curing temperature Reduce stenter temperature and dwell time to supplier guidance Metal ion contamination Use demineralized or softened process water Storage-related gas fading Improve ventilation, reduce storage time, add antioxidant protection For fabrics where yellowing resistance is a priority, Sylic F3575 Soft and Smooth Silicone Oil is a high-concentration self-emulsifying silicone oil with 64 to 66 percent solid content, formulated for low yellowing along with high bath stability and compatibility. It suits cotton, polyester, and blended fabrics that need to stay bright through curing, typically applied at 5 to 20 g/L in padding or 1 to 5 percent o.w.f. in exhaust dyeing. Spots and Uneven Deposits Oily-looking spots or uneven patches after softener application are frustrating because they often only appear after the fabric has dried, which means the problem is discovered late in the process. Causes of Spots Spots usually come from poor emulsion stability. When the silicone particles in the bath are too large, or the emulsion breaks under mechanical shear, agitation, or temperature swings, the oil phase separates and deposits unevenly on the fabric surface instead of spreading uniformly across the fibers. Emulsion Stability Several bath conditions influence how stable an emulsion stays through a padding run: pH, which should generally sit in the weakly acidic range for cationic silicone emulsions Water hardness and electrolyte content, both of which can destabilize the emulsion at higher levels Mixing sequence, since adding chemicals to the bath in the wrong order can cause premature coalescence before the fabric even enters the pad Prevention Techniques Pre-diluting the softener before it enters the bath, rather than adding concentrate directly, gives the emulsion time to disperse evenly and is the single most effective safeguard against spotting. Beyond that, maintaining a consistent bath temperature and controlling water hardness both reduce risk, and filtering the bath periodically during long runs helps catch early signs of emulsion breakdown before they show up on fabric. Self-emulsifying silicone oils, which carry built-in emulsifier groups in the polymer structure, disperse more evenly with simple agitation and are a good option where spotting is a recurring issue. Troubleshooting Steps If spots appear, start by checking the bath for visible

Explore More »

Contact Us for Textile Auxiliaries and Dyes

Contact Skychem Group for more chemical solutions, If you have questions or need more information, please contact us.
We will respond within 24 hours

Get a project quote

Tell us your project requirements, country, and intended application.

Sandy

With years of experience in chemical dyes and textile auxiliaries, I’m dedicated to sharing insights into the latest technologies, sustainable innovations, and market trends.

Recent Articles

An iodine drop is applied to a woven cotton sample.

Textile Desizing: Methods, Recipes, and Efficiency Control

Table of Contents What Is Desizing? Choose a Method by Size Type Desizing Enzymes and Chemicals Amylase for starch Wetting agents for liquor penetration Oxidative treatment for selected sizes Practical Desizing Recipes Enzymatic pad-batch Enzymatic exhaust Hot washing Oxidative treatment Measure Desizing Efficiency Select a Desizing Agent FAQ Which enzyme is used for textile desizing? Can amylase remove synthetic sizes? What is the difference between enzymatic and oxidative desizing? How is desizing efficiency tested? Why does fabric still absorb water poorly after desizing? How do I choose a desizing recipe for my mill? Warp size protects yarn during weaving. After weaving, that same coating must be removed so water and processing chemicals can reach the fabric evenly. A reliable desizing process begins with the size formulation, then moves through treatment, washing, and verification. What Is Desizing? Desizing removes the coating applied to warp yarns before weaving. It is an early preparation step for woven fabric headed to dyeing, printing, or finishing. Desizing targets applied size. Scouring removes impurities such as oils and natural waxes, while bleaching removes natural color. The steps may run separately or together, but a good result in one does not prove the others are complete. For more on their effect downstream, see how pretreatment affects fabric quality and color fastness. Choose a Method by Size Type Ask the weaving mill or yarn supplier which sizes were applied. If the formulation is unknown, test a representative sample before choosing the treatment. Size type Starting approach Main verification Starch or modified starch Amylase treatment followed by washing Residual starch Water soluble synthetic size Controlled hot washing Removal after the final rinse Mixed or difficult to remove size Trials with suitable washing and chemical treatment Removal of each component without unacceptable fabric damage These approaches are starting points. The fiber blend, size formulation, and equipment determine the final process. Desizing Enzymes and Chemicals Amylase for starch α-Amylase breaks starch into smaller, water soluble fragments that can be washed away. The enzyme must reach the size and remain active under the bath conditions. For a product-specific trial, Sylic B6141 Amylase (CY-15A) is identified as an α-amylase for textile desizing. Its product information describes compatibility with commonly used desizing wetting agents, and the pretreatment listing gives 1 g/L as a reference dosage. Confirm the working pH, temperature, and treatment time for the intended equipment before using that figure in a production recipe. Wetting agents for liquor penetration A wetting agent can improve contact between the treatment liquor and the sized fabric. Sylic P1400 Wetting Agent is listed for pretreatment of natural fibers, synthetic fibers, and blends. Its stated reference dosages are 0.5–2 g/L for intermittent processing and 2–6 g/L for continuous processing. These are product application ranges, not a confirmed recipe with any particular amylase; check bath compatibility in a trial. Oxidative treatment for selected sizes An oxidative route may be considered when washing or enzyme treatment does not adequately remove the known size. Test the proposed chemistry on the actual fabric. Size removal, strength, and appearance all matter when deciding whether to scale it up. Practical Desizing Recipes A usable recipe specifies treatment and wash-off. Set initial chemical conditions from the selected products’ technical data sheets, then validate them on production fabric. Enzymatic pad-batch Prepare a compatible enzyme bath, pad the fabric at a consistent pickup, and hold it for the validated dwell time. Wash out the degraded size afterward. Compare liquor pickup and residual starch at the center and edges of the fabric. Enzymatic exhaust Add the enzyme and any compatible auxiliaries under the recommended bath conditions. Record the liquor ratio, actual treatment temperature, and time held at that temperature. Drain and wash the fabric before testing it. Hot washing For a confirmed water soluble size, trial a wash sequence with adequate heat, liquor movement, and rinsing. Check the fabric after the final rinse, since dissolving size in the bath does not guarantee its removal from the cloth. Oxidative treatment Choose the chemical system for the known size and fiber blend. Begin with a small trial and check fabric strength and appearance alongside size removal. For each trial, record the size formulation, fabric, products, dosages, pH, temperature, time, liquor ratio or pickup, wash sequence, and test results. This makes the result reproducible across shifts and machines. Measure Desizing Efficiency For starch sized fabric, an iodine test can reveal residual starch. A TEGEWA rating can be used to record and compare the result. Sample the center and edges of the fabric at more than one point in the run. An iodine result does not establish whether synthetic size has been removed. Use an assessment suited to the known formulation, then check that the fabric meets the absorbency requirements of its next process. When results are incomplete or uneven, check four points in sequence: Size formulation: Does the treatment address every component? Bath conditions: Were concentration, pH, temperature, and time controlled? Penetration: Did liquor reach the full fabric width evenly? Wash-off: Were dissolved or degraded materials rinsed away? If starch removal is satisfactory but absorbency remains poor, investigate oils, waxes, and scouring performance before increasing the enzyme dose. Select a Desizing Agent Share the size formulation, fiber blend, machine type, available temperature range, and current defect when requesting a product recommendation. Compare candidates on the same fabric under defined trial conditions. Judge the result by residual size, absorbency, uniformity, fabric quality, washing demand, and total process cost. A lower chemical dose is not an improvement if it increases rinsing or rework. FAQ Which enzyme is used for textile desizing? α-Amylase is commonly used for starch based size. Select a product whose operating conditions suit the fabric and equipment. Can amylase remove synthetic sizes? Do not assume that it can. Identify the synthetic size and test a suitable washing or chemical treatment. What is the difference between enzymatic and oxidative desizing? Enzymatic desizing uses an enzyme to break down its target size, such as starch in an amylase process. Oxidative desizing

Explore More »
Light printed pattern on dark cotton fabric

Discharge Printing in Textiles: Process, Chemicals, and Problems

Table of Contents How Discharge Printing Works Fabrics and Dyes White and Color Discharge Chemicals and Auxiliaries Production Process Common Problems and Fixes FAQs Which dyes are suitable for discharge printing? Why does a white discharge print look yellow or pink? Can polyester or blended fabrics be discharge printed? What causes incomplete discharge? What should buyers test before bulk production? Discharge printing creates a pattern by chemically changing the dye in selected areas of an already dyed fabric. A printer applies a discharge paste, fixes the print under conditions suited to the dye and fiber, and washes away removable residues. The result is a lighter pattern or a newly colored one against the original ground shade. The method can produce crisp, light motifs on dark fabric without the heavy surface layer of an opaque overprint. Its main limitation is predictability: a recipe that gives a clean white on one ground shade may leave a pink or yellow cast on another. The ground dye and the finished trial print must therefore be evaluated together. How Discharge Printing Works The fabric is first dyed to its ground shade. A print paste containing a discharging agent is applied only where the design should appear. During fixation, the agent changes susceptible dye molecules in those areas. Most of the methods discussed here use a reducing agent, although other discharge routes exist. The required wash-off removes paste residues and dye reaction products that can be washed away. Ordinary overprinting places color over the existing shade. Resist printing prevents a ground color from developing in selected areas. Discharge printing starts with a colored fabric and changes the shade afterward. In a mixed black or navy, one dye component may resist treatment and leave a visible undertone. This is why the full ground-shade recipe matters more than the color name. Fabrics and Dyes Cotton and other cellulosic fabrics are common substrates. Selected reactive, direct, and azoic dyes can provide a dischargeable ground. Vinyl sulfone reactive dyes are used in established cotton discharge processes, although performance depends on the individual dye and shade mixture. The reactive dyes for cellulosic fabrics page identifies the Skyzol General Series as containing vinyl sulfone (KN type) and vinyl sulfone/monochlorotriazine (M type) dyes. This identifies chemistry worth screening, not a discharge rating. Request results for the exact shades before selecting a ground recipe. Polyester, wool, silk, and blends require different dye and fixation choices. Polyester processes may call for selected disperse dyes and different fixation conditions from those used on cotton. Wool and silk require close attention to fiber strength and handle. On a blend, the components may discharge differently, making an even white difficult to achieve. White and Color Discharge White discharge changes the ground shade without adding an illuminating colorant. The finished area may look white, cream, or faintly tinted, depending on the fabric and residual dye color. A white pigment may be included for greater opacity in some systems, but the ground still needs to discharge effectively. Color discharge changes the ground shade while introducing an illuminating dye or pigment in the printed area. In a suitable cotton process, selected vat dyes for cotton can serve as illuminating dyes. The product range does not specify which dyes work in discharge paste, so selection must account for paste stability, shade development, oxidation, and final fastness. White discharge makes residual ground color particularly visible. Color discharge adds the challenge of developing the new shade consistently across the run. Chemicals and Auxiliaries The discharging agent is the active component of the paste. Sodium formaldehyde sulfoxylate is widely used in cellulosic discharge processes. Zinc formaldehyde sulfoxylate is another option, including in some synthetic-fiber systems. Thiourea dioxide can be used in selected processes but requires appropriate conditions and paste stability. These agents are not interchangeable: compare discharge quality and fabric strength under the intended fixation conditions. The other paste ingredients control application and appearance. A compatible thickener helps hold sharp edges without blocking the screen. Wetting agents and humectants may be used to adjust penetration and moisture retention. In color discharge, a pigment formulation may need a binder for adhesion. Check the whole mixture for changes in viscosity, separation, or particles that could block the screen. The textile printing auxiliaries page gives useful screening details. Sylic PR4200 is an anionic thickener listed for reactive printing on cotton and linen, with electrolyte resistance and a 3% reference dosage. Sylic PR4223 is listed for roller and screen printing, with water-holding and electrolyte-resistance properties and a 1.5–2% reference dosage. These figures describe the listed printing applications, not validated discharge-paste dosages. Check each candidate’s stability with the chosen reducing agent before using it. For the broader functions of these ingredients, see thickeners, binders, and fixers in textile printing. For product selection, specify fiber content, the ground-dye recipe, print method, fixation equipment, target shade, and fastness requirements. Request technical and safety documentation. If the formulation uses a formaldehyde sulfoxylate, include customer limits on residual formaldehyde in the finished-fabric test plan. Production Process Prepare the ground fabric. Dye and wash it consistently. Confirm that pretreatment residues and shade variation will not affect the print. Test dischargeability. Print small samples of the actual ground fabric. Judge the result after full fixation and washing, not while the print is still wet. Prepare the paste. Follow the supplier’s mixing instructions. Record viscosity, ingredient order, and usable working time; prepare only as much paste as the validated process permits. Print the design. Keep screen condition, paste deposit, pressure, and fabric tension consistent. Monitor fine lines and solid areas separately. Dry and fix. Control temperature, moisture, and dwell time for the chosen fiber and chemistry. Steam and dry heat can produce different discharge effects, so use the route established in the trial. Complete post-treatment. Follow the formulation’s specified oxidation, rinsing, and wash-off sequence where applicable, then dry and finish the fabric. Insufficient washing can leave residues or a dull print. Approve the bulk standard. Compare the finished sample with the target for ground shade, print

Explore More »
Two professionals discussing production beside factory equipment

How to Choose a Textile Chemical Supplier?

Table of Contents Check Product Quality in Your Process Verify Compliance for the Exact Product Test Batch Consistency and Traceability Evaluate Technical Support During the Trial Compare Total Cost, Then Run a Mill Trial FAQ What documents should a textile chemical supplier provide? How do I test a new dye or auxiliary supplier? How can I check batch-to-batch consistency? Which chemical compliance requirements should I verify? A textile chemical supplier influences what happens on the production floor long after a purchase order is placed. Inconsistent dye strength can force shade corrections. An auxiliary that performs well in a sample test but poorly in the mill can slow production or create rework. Missing compliance documents can delay customer approval. Price matters, but it is only one part of the decision. A sound supplier evaluation asks whether the products work in your process, whether the required evidence is available, whether performance holds across batches, and whether technical help is useful when conditions change. Before requesting samples, define the fiber, machinery, process, target result, and customer requirements. Give each prospective supplier the same information. That makes its recommendations easier to assess and its products easier to compare. Check Product Quality in Your Process Product quality depends on the application. A chemical can meet its published specifications and still be a poor match for your fabric, water, equipment, or recipe. Begin with laboratory tests, then confirm promising results at production scale. For textile dyes, assess the properties that affect the finished order: Shade and strength: Does the dye reach the target shade at the expected dosage? Recipe compatibility: Does it perform consistently alongside the other dyes and chemicals used in the bath? Process behavior: Is the result stable under the mill’s normal temperature profile, pH, and processing time? Fastness: Does the dyed fabric meet the customer’s relevant washing, rubbing, or light fastness requirements? For textile auxiliaries, test the claimed function rather than relying on a general description. A wetting agent should provide suitable penetration and uniformity within the available contact time. A leveling agent should help control uneven dyeing while allowing the target shade to develop. A softener should deliver the required hand feel without causing an unacceptable loss of absorbency or a visible shade change. Product parameters help identify candidates, but their meaning depends on the application. The listed specifications for Sylic F3400 silicone softener include 62–64% solid content and recommended dosages for a diluted emulsion. Those figures help a buyer plan a trial, but they do not establish the right dilution or dosage for every mill. Testing should confirm emulsion preparation, compatibility with the finishing bath, hand feel, and performance at the actual working concentration. Ask for a current technical data sheet and a sample of each shortlisted product. Use the same fabric and controlled conditions for comparative trials. Record both the result and the amount of product required to achieve it. Verify Compliance for the Exact Product Compliance is not a single certificate that covers every purchasing situation. Requirements depend on the formulation, the customer’s specifications, and the markets where the chemical or finished textile will be used or sold. Request a current safety data sheet for the product under consideration. Then identify any additional evidence your customer requires. If ZDHC MRSL conformance is specified, check the status of the particular formulation. The MRSL addresses restricted substances in chemical inputs used during manufacturing. It does not certify that a finished textile meets all customer requirements. A supplier’s published textile chemical certificates can help begin the review. For each document, check: The product name or code it covers The issuing body and scope Its validity period Whether the documented formulation matches the product offered Ask for clarification if a certificate names a product family but the proposed grade is unclear. If the formulation changes later, confirm whether the existing evidence still applies. This check is especially important when approving a substitute for a previously qualified chemical. Test Batch Consistency and Traceability A successful sample test establishes a starting point. It does not prove that future shipments will produce the same result. Ask the supplier which properties it measures before releasing each batch and what limits it accepts. For a dye, relevant checks may include shade and relative strength. For an auxiliary, they may include pH, solid content, and a test tied to its intended function. The appropriate limits should reflect the product and the sensitivity of your process. Every shipment should have an identifiable lot number. Confirm whether the supplier retains samples and can link a delivered lot to its production and quality records. When order volumes justify it, compare results from two or more production lots before relying on the product for a critical program. Agree on a procedure for deviations before they occur. The mill should know what information to provide, such as the lot number, fabric, recipe, process conditions, and test results. The supplier should be able to explain how it will investigate the difference and resolve an out-of-specification delivery. Clear records make it easier to distinguish a chemical variation from a change in the mill’s process. Evaluate Technical Support During the Trial A product recommendation is more useful when it is based on the mill’s operating conditions. Share enough detail for a meaningful answer: fiber content, equipment, water conditions, current recipe, target result, and the problem you are trying to solve. Then assess the response. If the issue is uneven shade, does the supplier ask about pretreatment, dosing, temperature, and bath conditions before suggesting an adjustment? If wetting is slow, does it consider the fabric and available contact time? Good technical support identifies factors to check and proposes a trial that can confirm or rule out a cause. The trial also shows how support works in practice. Confirm who will answer questions after purchase, which test data the supplier can review, and how quickly it can respond across time zones. These details matter when a mill must decide whether to adjust a process or hold production. Compare

Explore More »
Cotton terry compares water absorbency.

Silicone Softener Problems: Causes and Solutions for Yellowing, Spots and Hydrophilicity Loss

Table of Contents Yellowing Issues Common Causes Heat and Curing Effects Prevention Tips Fixing Yellowed Fabric Spots and Uneven Deposits Causes of Spots Emulsion Stability Prevention Techniques Troubleshooting Steps Shade Change After Softening Why Shade Change Happens Dye Compatibility Minimizing Shade Variation Loss of Hydrophilicity Why Absorbency Drops Balancing Softness and Absorbency Hydrophilic Softener Options Best Practices for Application Correct Dosage and Dilution Padding and Drying Parameters Quality Control Testing Conclusion FAQs What causes silicone softener to turn fabric yellow? How can I prevent spots after softener treatment? Why does fabric shade change after softening? How do I restore hydrophilicity after softener use? Silicone softeners are among the most widely used finishing chemicals in textile mills, valued for the smooth hand feel, drape, and durability they bring to fabric. But they can also be a source of real headaches on the production floor. Yellowing on white goods, oily spots after padding, unexpected shade shifts, and a sudden loss of water absorbency are among the most common complaints raised by finishers, dyers, and quality teams worldwide. Nearly every one of these problems traces back to a small number of root causes: the wrong silicone chemistry for the substrate, poor emulsion stability, incorrect bath conditions, or curing parameters pushed past the chemistry’s limits. Once the underlying fiber and polymer behavior is understood, most of these issues can be prevented with a better product choice, a small process adjustment, or tighter quality control at the padding stage. This article walks through each problem in turn, covering what causes it and how to prevent or correct it. Yellowing Issues Yellowing is one of the most commonly reported complaints with silicone softeners, especially on white and pastel fabrics where even a slight color shift is immediately visible. Common Causes Most yellowing traces back to the amine content in the silicone polymer. Amino-modified silicones deliver excellent softness because the amine groups anchor strongly to the fiber surface, but those same groups are chemically reactive and prone to oxidation. A few conditions make the problem worse: Contamination from iron or other transition metals in the bath water Residual chlorine left over from bleaching Low-quality or inconsistent raw materials in the softener itself Heat and Curing Effects Yellowing often becomes visible only after the fabric passes through the stenter. Thermal oxidation of free amine groups during curing generates chromophores, the compounds responsible for the yellow tint, and this effect grows more pronounced as yellowing can become more pronounced when curing temperatures exceed the recommended range for the specific silicone softener and fabric. A second, less obvious mechanism is gas fading, sometimes called NOx yellowing, where atmospheric nitrogen oxides react with amine groups during storage or transport. This can occur without any heat exposure at all, which is why fabric sometimes yellows weeks after it leaves the finishing line, long after the mill has moved on to the next order. Prevention Tips A few adjustments go a long way toward keeping fabric bright: Choose a softener with a lower amine value for light and white goods Keep curing temperature and dwell time within the supplier’s recommended window Use demineralized water to reduce metal ion contamination Add an antioxidant, or switch to a block silicone rather than a straight amino silicone, for goods that will be stored or shipped over long distances Fixing Yellowed Fabric Once yellowing has occurred, options are limited. Mild cases can sometimes be improved with a peroxide or reducing bleach treatment, though this carries some risk to fabric strength and should always be tested on a sample first. In most cases, the more reliable fix is prevention on the next batch rather than correction after the fact, which is why product selection and process control matter so much upfront. Cause Recommended Fix High amine value silicone Switch to a low amine value or block silicone softener Excess curing temperature Reduce stenter temperature and dwell time to supplier guidance Metal ion contamination Use demineralized or softened process water Storage-related gas fading Improve ventilation, reduce storage time, add antioxidant protection For fabrics where yellowing resistance is a priority, Sylic F3575 Soft and Smooth Silicone Oil is a high-concentration self-emulsifying silicone oil with 64 to 66 percent solid content, formulated for low yellowing along with high bath stability and compatibility. It suits cotton, polyester, and blended fabrics that need to stay bright through curing, typically applied at 5 to 20 g/L in padding or 1 to 5 percent o.w.f. in exhaust dyeing. Spots and Uneven Deposits Oily-looking spots or uneven patches after softener application are frustrating because they often only appear after the fabric has dried, which means the problem is discovered late in the process. Causes of Spots Spots usually come from poor emulsion stability. When the silicone particles in the bath are too large, or the emulsion breaks under mechanical shear, agitation, or temperature swings, the oil phase separates and deposits unevenly on the fabric surface instead of spreading uniformly across the fibers. Emulsion Stability Several bath conditions influence how stable an emulsion stays through a padding run: pH, which should generally sit in the weakly acidic range for cationic silicone emulsions Water hardness and electrolyte content, both of which can destabilize the emulsion at higher levels Mixing sequence, since adding chemicals to the bath in the wrong order can cause premature coalescence before the fabric even enters the pad Prevention Techniques Pre-diluting the softener before it enters the bath, rather than adding concentrate directly, gives the emulsion time to disperse evenly and is the single most effective safeguard against spotting. Beyond that, maintaining a consistent bath temperature and controlling water hardness both reduce risk, and filtering the bath periodically during long runs helps catch early signs of emulsion breakdown before they show up on fabric. Self-emulsifying silicone oils, which carry built-in emulsifier groups in the polymer structure, disperse more evenly with simple agitation and are a good option where spotting is a recurring issue. Troubleshooting Steps If spots appear, start by checking the bath for visible

Explore More »

Contact Us for Textile Auxiliaries and Dyes

Contact Skychem Group for more chemical solutions, If you have questions or need more information, please contact us.
We will respond within 24 hours

Get a project quote

Please tell us the requirements, the country and the application.

Scroll to Top
Email WhatsApp

Contact Us for Textile Auxiliaries and Dyes

Contact Skychem Group for more chemical solutions, If you have questions or need more information, please contact us.
We will respond within 24 hours